

 English
 中文简体
 русский
 Deutsch
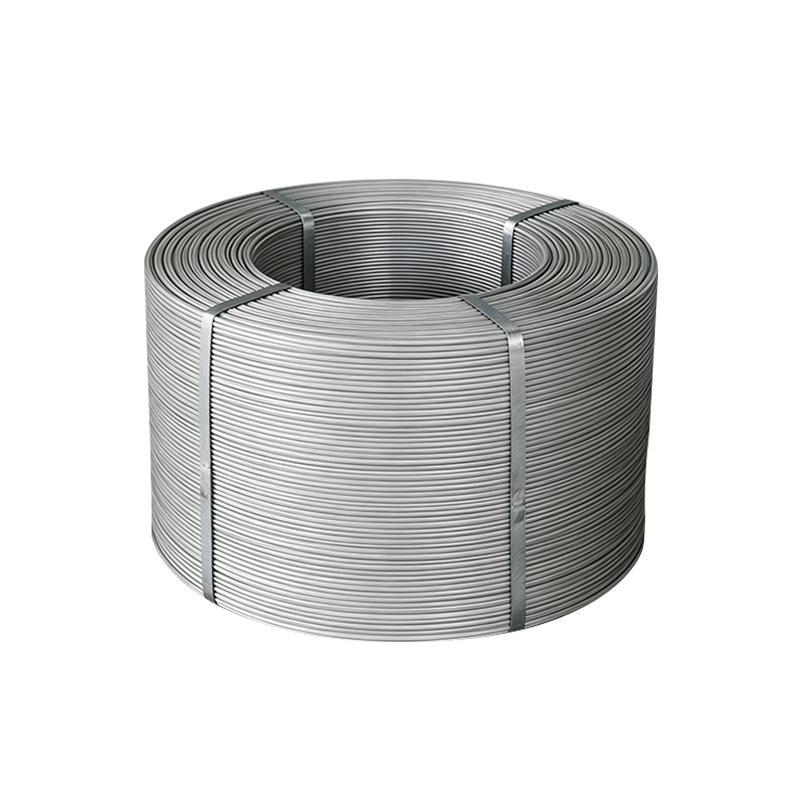
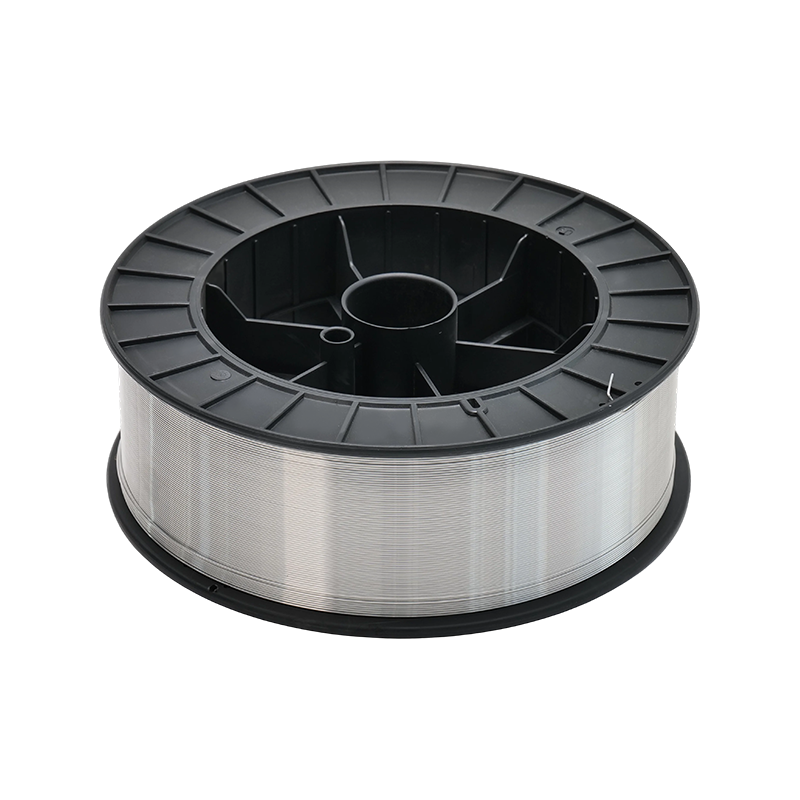
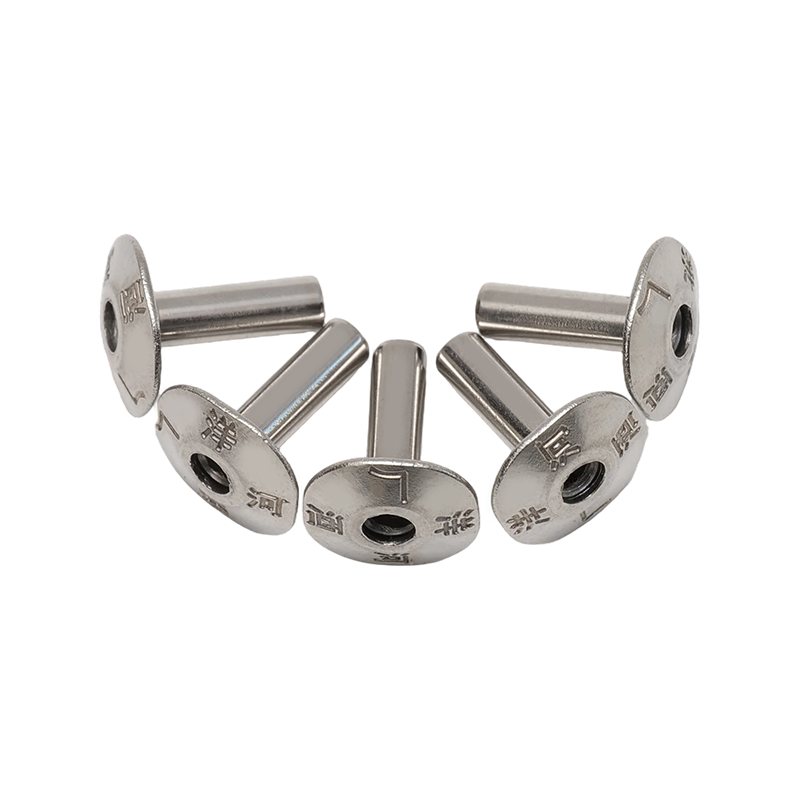
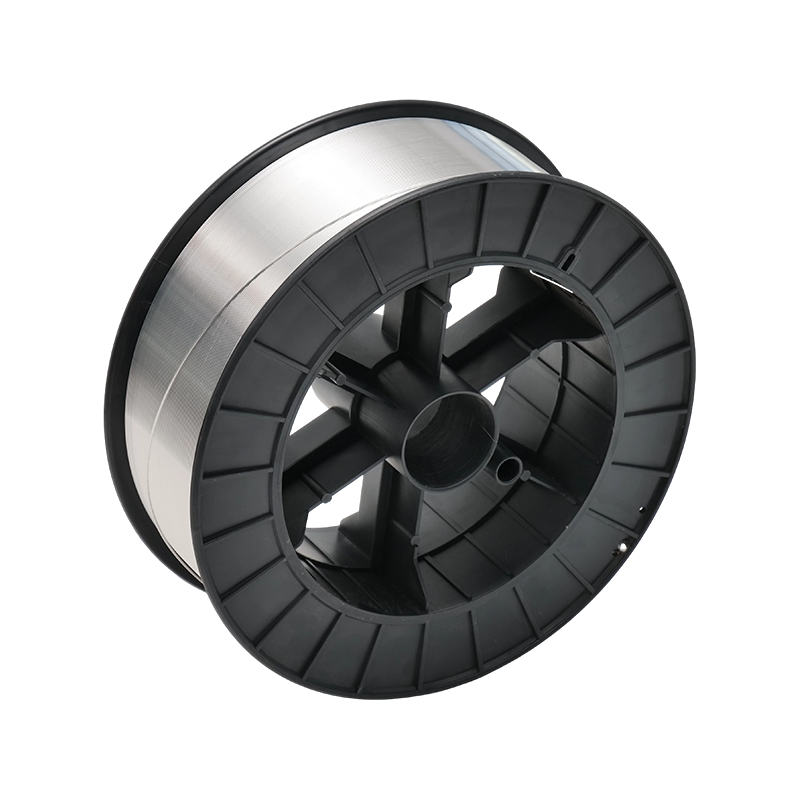
High-strength aluminum alloy wire for rivets is an essential engineering material in industries where low weight, dependable mechanical performance, corrosion resistance, and dimensional consistency are required at the same time. Riveted joints remain widely used in aircraft structures, aerospace assemblies, transportation equipment, defense systems, and precision mechanical components because they can provide reliable fastening without the heat-affected zones associated with some welding processes. The quality of the rivet wire directly influences forming behavior, joint strength, fatigue performance, corrosion resistance, and long-term service reliability.
This product is designed for demanding applications that require carefully controlled alloy chemistry, stable wire dimensions, consistent surface quality, and compatibility with different heat-treatment conditions. It is primarily associated with high-strength aluminum alloy wire, while the wider product range also includes high-purity aluminum wire and aluminum or aluminum alloy welding materials. The available alloy portfolio includes 2A10, 2219, 7050, and 7075, together with several aluminum-magnesium and aluminum-silicon grades used for welding and related industrial purposes.
Aluminum rivet wire offers a valuable alternative to heavier steel-based fastening materials. Its low density helps reduce structural weight, while its alloy design can provide high specific strength. In aviation and aerospace applications, even a small reduction in fastening weight can contribute to lower fuel consumption, increased payload capacity, improved range, and better overall efficiency. At the same time, a properly selected alloy can deliver the strength and durability needed for highly loaded structural joints.
The product is manufactured by Jiangsu Hetuo Aluminum Wire Co., Ltd., an aluminum wire producer based in Lianyungang, Jiangsu Province, China. The company operates a manufacturing facility covering approximately 40,000 square meters and has developed production capabilities for high-purity aluminum wire, high-strength aluminum alloy wire, welding wire, alloy rods, and precision aluminum profiles. Its production system combines alloy preparation, controlled processing, drawing, surface management, inspection, and order-specific manufacturing support.
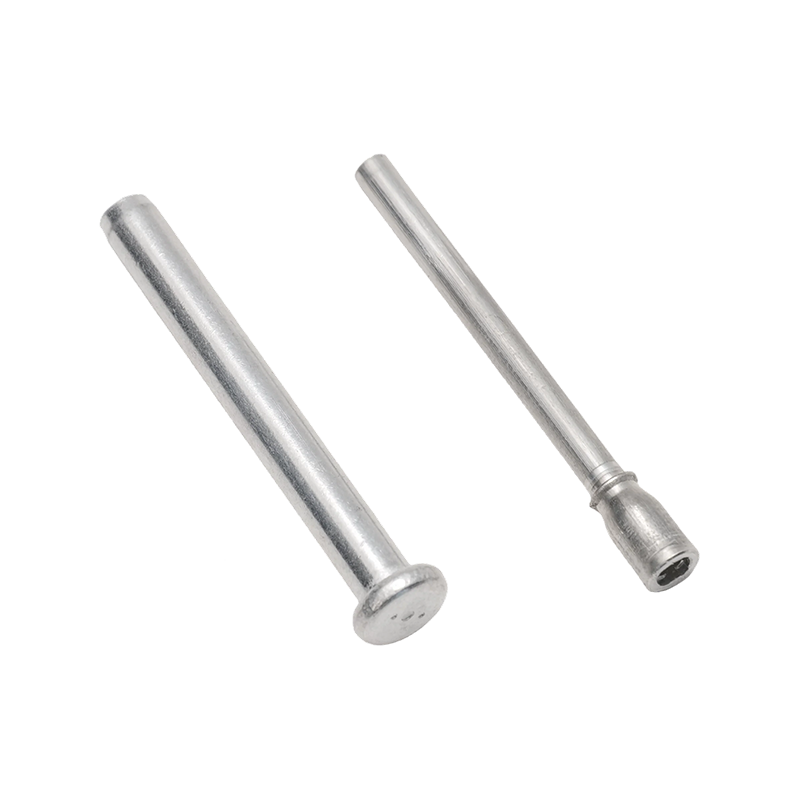
For Rivets
Content
- 1 Why Aluminum Alloy Rivet Wire Matters in Modern Engineering
- 2 Product Advantages Compared with Conventional Rivet Materials
- 3 Alloy Portfolio for Rivets and Aluminum Processing
- 4 Manufacturing Process and Quality Control
- 5 Advanced Manufacturing Strengths
- 6 Application Areas
- 7 How to Select the Correct Rivet Wire
- 8 Packaging, Storage, and Handling
- 9 Competitive Value for Global Buyers
- 10 Recommended Purchasing Checklist
- 11 Quality and Sustainability Considerations
- 12 Q&A: Aluminum Alloy Wire for Rivets
- 12.1 What is aluminum alloy rivet wire used for?
- 12.2 Which alloys are available for high-strength rivet applications?
- 12.3 Why are T6, T73, and T76 conditions important?
- 12.4 Is 7075 always the best alloy for rivets?
- 12.5 Can the wire be customized?
- 12.6 What quality documents should buyers request?
- 12.7 How does wire quality affect rivet production?
- 12.8 Can these products support welding applications as well as riveting?
- 12.9 Where is the manufacturer located?
- 12.10 How should aluminum alloy wire be stored?
- 13 Conclusion
- 14 References
- 15 Product: For Rivets
Why Aluminum Alloy Rivet Wire Matters in Modern Engineering
Rivets are permanent mechanical fasteners that join two or more components by deforming a prepared shank. During installation, the rivet is inserted through aligned holes and then upset, compressed, or formed to create a second head. The material must therefore balance strength with ductility. If the wire is too hard or brittle, forming may cause cracking, splitting, or incomplete head formation. If it is too soft, the finished rivet may not provide the required clamping force or resistance to service loads.
Aluminum alloy rivet wire is produced to meet this balance. The alloy is selected according to the intended application, required strength level, corrosion environment, forming method, and heat-treatment route. For example, copper-containing aluminum alloys may provide high strength after suitable treatment, while aluminum-magnesium alloys may emphasize corrosion resistance, weldability, and stable performance in marine or industrial environments.
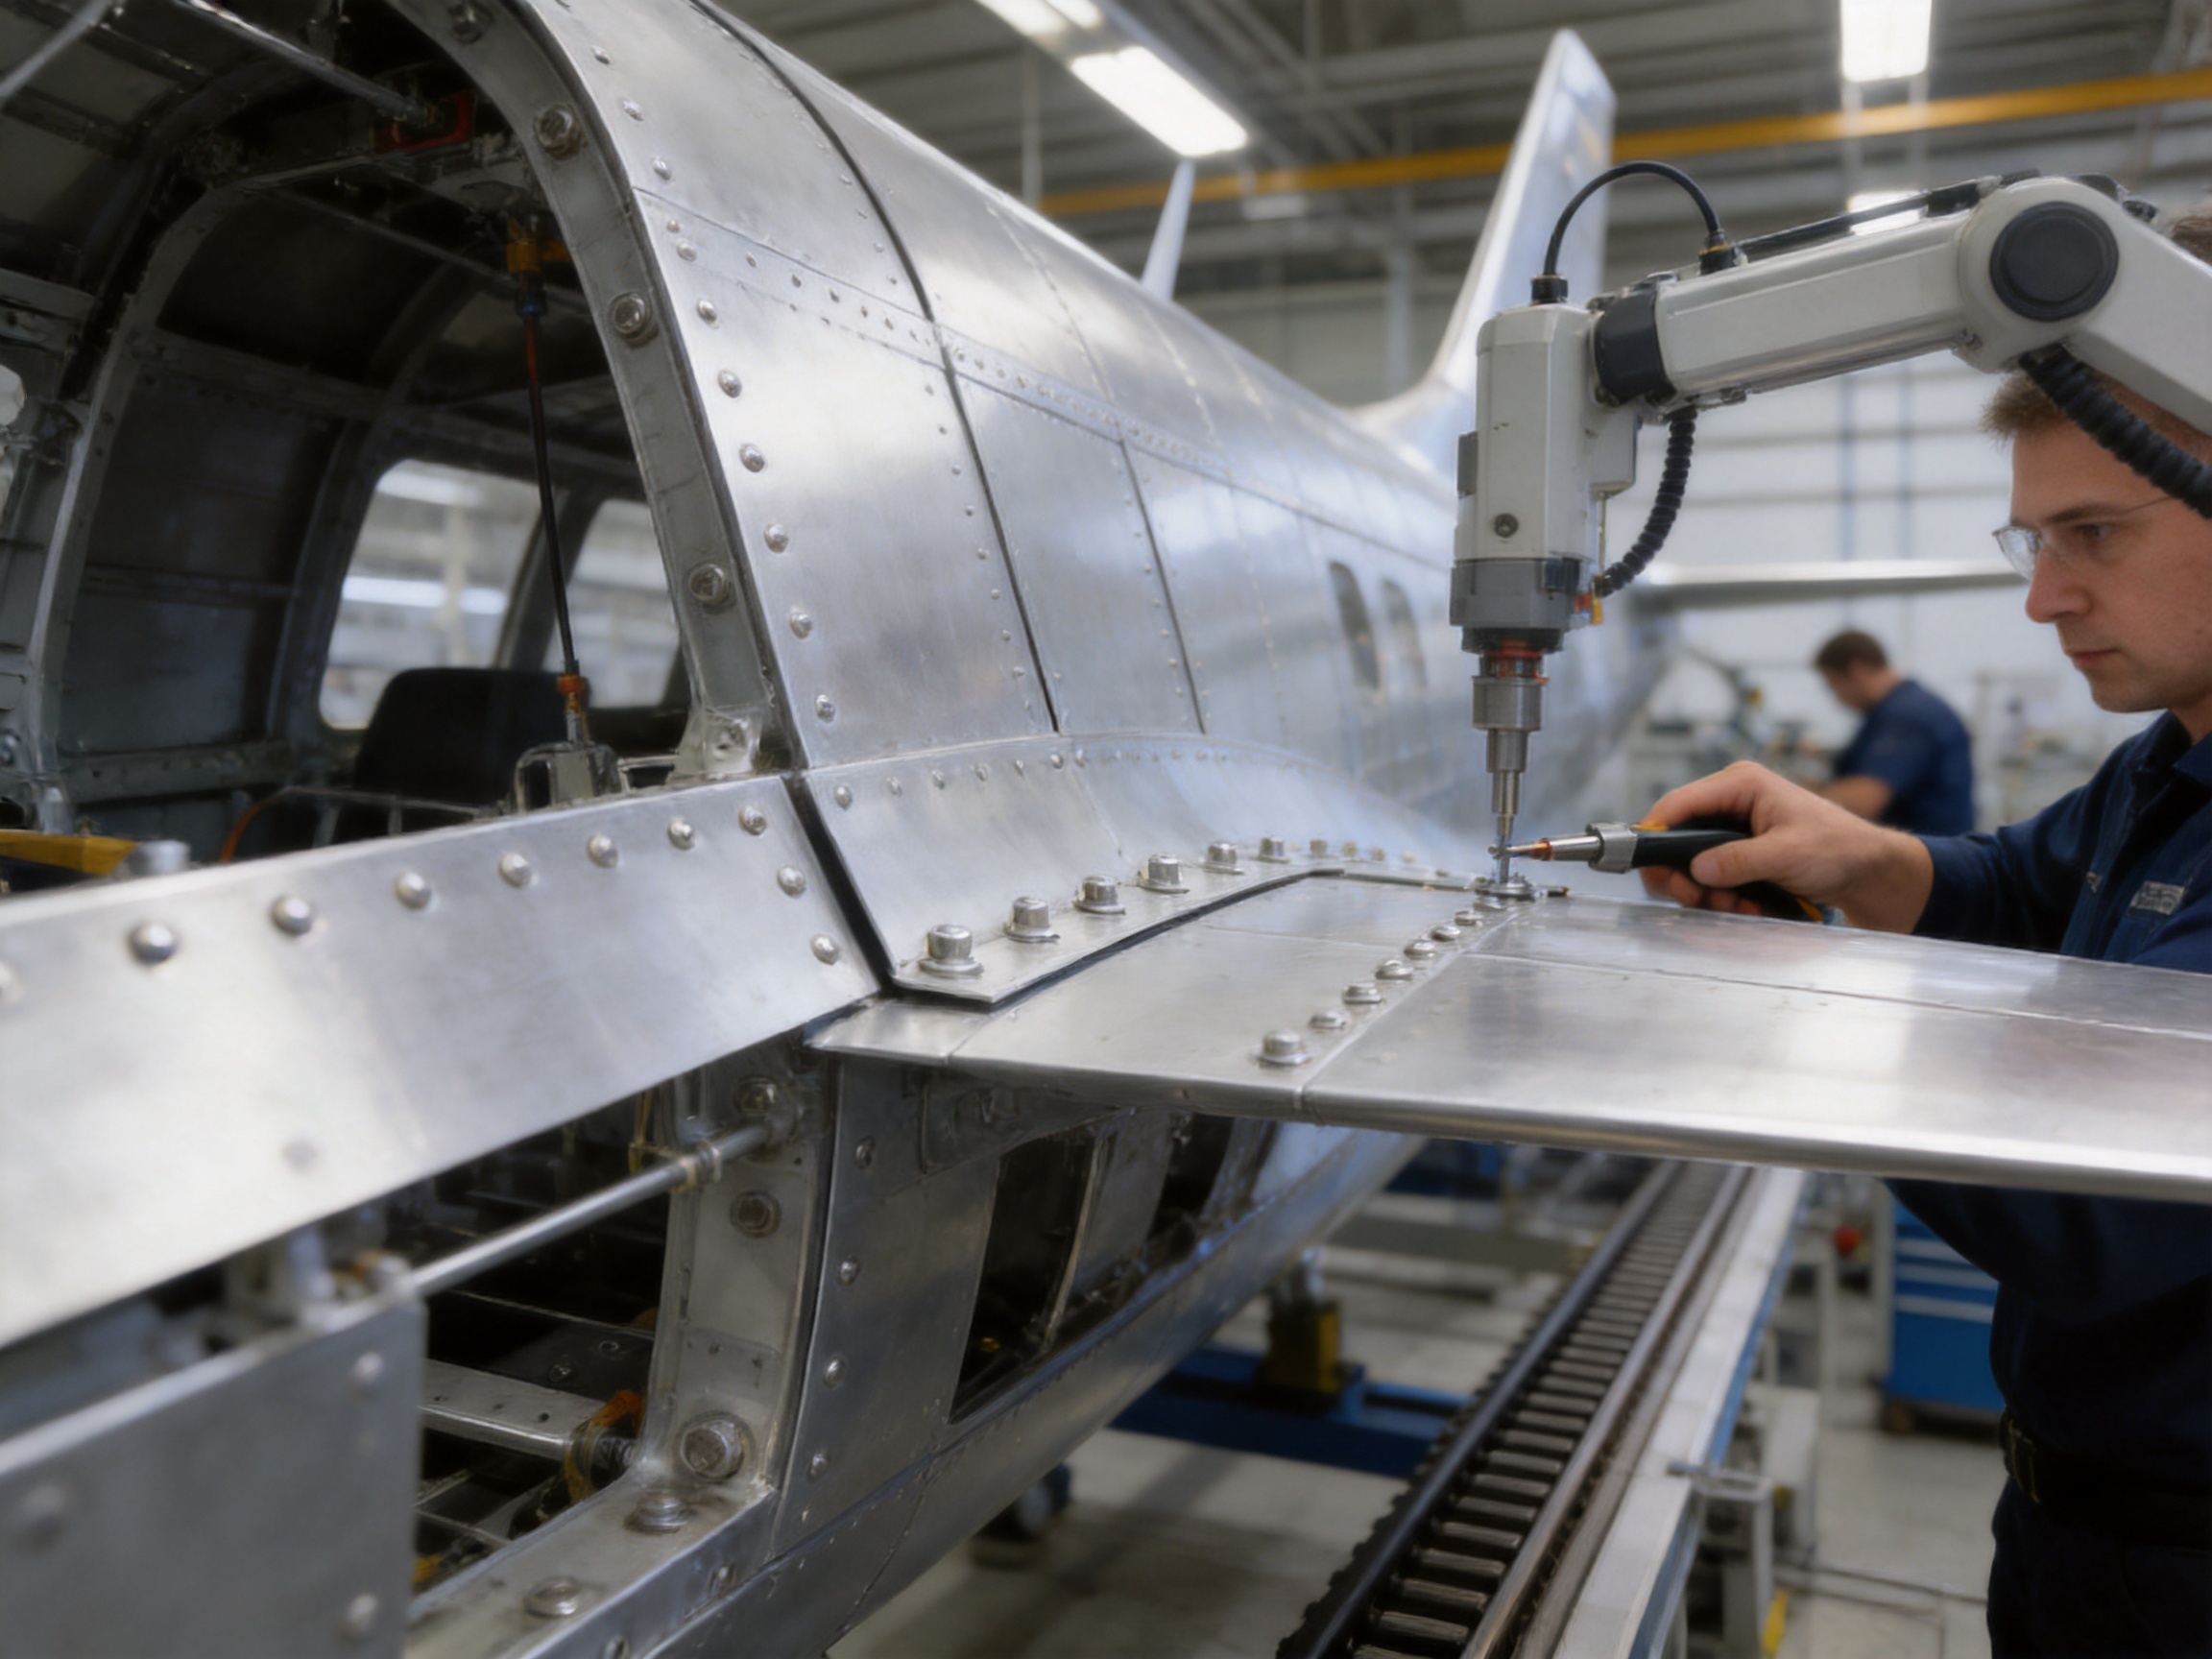
In aerospace structures, rivets may be used in fuselage skins, wing components, frames, brackets, panels, seats, access structures, and internal reinforcement systems. These components are exposed to vibration, pressure cycling, temperature changes, moisture, and repeated mechanical loads. The rivet must maintain joint integrity over a long service life. Consistent alloy chemistry and wire quality are therefore critical from the first stage of production.
In military and defense applications, fastening materials may be required to perform in severe environments, including low temperatures, high vibration, dust, humidity, and rapid changes in operating conditions. A suitable high-strength aluminum alloy wire can provide the required combination of light weight, structural performance, and corrosion resistance while supporting efficient repair and assembly processes.
In general industrial applications, aluminum rivet wire can be used where conventional fasteners are too heavy, where galvanic compatibility with aluminum components is important, or where an economical and repeatable cold-forming process is preferred. The material can be supplied for automatic rivet production, precision forming, and custom manufacturing programs that require controlled dimensions and repeatable batches.
Product Advantages Compared with Conventional Rivet Materials
Low Density and Weight Reduction
One of the most important advantages of aluminum alloy rivet wire is its low density compared with steel, stainless steel, and many nickel-based fastening materials. Reducing the weight of individual rivets may appear minor, but large aircraft, rail vehicles, industrial panels, and assembled equipment can contain thousands or millions of fasteners. The accumulated weight reduction can be significant.
Weight savings are particularly valuable in aviation and aerospace. Lower fastening weight can support fuel efficiency, range, payload optimization, and easier handling during assembly or maintenance. In transportation equipment, lightweight aluminum fasteners may contribute to improved energy efficiency and reduced structural mass without requiring a major redesign of the joint.
High Specific Strength
Aluminum alloys do not simply compete on density. Several precipitation-strengthened grades provide high strength relative to their weight. Alloy families such as 2A10, 2219, 7050, and 7075 can be considered for applications where a high strength-to-weight ratio is more important than maximum absolute strength alone.
The strength of these materials depends on alloy chemistry, processing history, final diameter, temper, and heat treatment. The product information identifies T6, T73, and T76 conditions as important performance states for high-strength aluminum alloys. T6 is associated with high strength, while T73 emphasizes fracture toughness and resistance to stress corrosion and exfoliation corrosion. T76 is described as providing higher strength than T73 while maintaining higher stress-corrosion resistance than T6.
This range of temper options gives designers greater flexibility. A component exposed mainly to static loads may require a high-strength condition, while a critical aerospace joint exposed to sustained stress and a corrosive environment may benefit from a condition that places greater emphasis on toughness and corrosion resistance.
Corrosion Resistance and Service Stability
Aluminum naturally forms a thin oxide film that helps protect the underlying metal. Alloy selection and processing determine how effectively the material performs in a particular environment. Aluminum-magnesium alloys are often valued for corrosion resistance, while carefully treated high-strength alloys can provide improved resistance to stress corrosion cracking and exfoliation corrosion.
The T73 and T76 conditions are especially relevant where long-term environmental durability is important. Stress corrosion can develop when tensile stress and a corrosive environment act together. Exfoliation corrosion can affect certain alloy structures and may reduce the reliability of heavily worked or rolled components. Selecting the correct alloy and temper helps engineers balance strength with environmental resistance rather than relying on strength alone.
Corrosion resistance also influences maintenance costs. A stable rivet material can reduce the likelihood of premature replacement, joint degradation, and surface damage. However, final performance still depends on joint design, surface treatment, contact with dissimilar metals, moisture management, and installation practice.
Reliable Formability
Rivet wire must be capable of forming under controlled pressure or impact. The wire is often cut into blanks before the rivet head is created. During this process, the material experiences localized plastic deformation. Uniform microstructure, clean surface condition, and consistent diameter help reduce the risk of head cracking, incomplete filling, eccentricity, and dimensional variation.
The correct temper is essential. A material optimized only for maximum strength may be difficult to form, while an overly soft material may not meet the final mechanical requirements. Manufacturers and users must therefore coordinate the incoming wire condition with the downstream forming and heat-treatment process.
Controlled drawing and intermediate processing can help produce wire with stable dimensions and a smooth surface. These characteristics are important for automated equipment because feeding systems, cutters, dies, and heading tools depend on predictable material behavior.
Compatibility with Precision Manufacturing
Modern rivet production is increasingly automated. High-speed equipment requires wire that feeds consistently, maintains a narrow diameter tolerance, and does not contain excessive surface defects. Variations in wire geometry can lead to stoppages, tool wear, inconsistent rivet dimensions, and increased scrap.
Precision aluminum wire supports better production efficiency by helping manufacturers stabilize their forming conditions. Consistent coil or spool packaging can also simplify material handling and reduce the time required for production changeovers. For high-volume customers, these benefits may be as important as the nominal alloy strength.
Alloy Portfolio for Rivets and Aluminum Processing
The product information includes a broad chemical composition table covering structural rivet alloys and welding grades. Not every grade is intended for exactly the same end use. The correct selection depends on the application, required strength, forming behavior, welding compatibility, and applicable standards. The following grades are especially relevant to high-strength aluminum wire and associated aluminum material programs.
| Alloy | Main Alloying Features | Typical Performance Focus | Potential Application Direction |
|---|---|---|---|
| 2A10 | Copper approximately 3.9–4.5%; manganese approximately 0.30–0.50%; magnesium approximately 0.15–0.30% | High-strength precipitation-hardenable aluminum alloy | Aircraft and aerospace rivet components |
| 2219 | Copper approximately 5.8–6.8%; manganese approximately 0.2–0.4% | High strength, heat-treatable performance, and elevated-temperature capability | Aerospace structures and demanding mechanical assemblies |
| 7050 | Zinc approximately 5.7–6.7%; magnesium approximately 1.9–2.6%; copper approximately 2.0–2.6% | Very high strength with attention to stress-corrosion performance | Highly loaded aerospace and defense components |
| 7075 | Zinc approximately 5.0–7.0%; magnesium approximately 1.8–2.8%; copper approximately 1.4–2.0% | High strength-to-weight ratio | High-strength structural and precision components |
| 4043 | Silicon approximately 4.5–6.0% | Good melting and welding characteristics | Aluminum welding materials and joining applications |
| 4047 | Silicon approximately 11.0–13.0% | High silicon content and fluidity for joining processes | Brazing and welding-related applications |
| 5183 | Magnesium approximately 4.3–5.2%; manganese approximately 0.5–1.0% | Strength and corrosion-resistant aluminum-magnesium performance | Welding materials and fabricated structures |
| 5356 | Magnesium approximately 4.5–5.5% | General-purpose aluminum-magnesium welding performance | Welding wire for aluminum structures |
2A10 Aluminum Alloy Wire
2A10 is a copper-containing, heat-treatable aluminum alloy designed for high-strength applications. The reported copper range is approximately 3.9% to 4.5%, with manganese and magnesium used as additional alloying elements. Copper contributes to precipitation strengthening after appropriate thermal treatment, allowing the alloy to achieve performance levels that are not available from commercially pure aluminum.
For rivet applications, 2A10 can be considered where a balance of strength and forming capability is required. The exact suitability depends on the supplied temper and the forming procedure. It is particularly relevant to aircraft and aerospace manufacturing, where high-strength aluminum fastening materials have a long history of use.
2219 Aluminum Alloy Wire
2219 contains a relatively high copper level, listed at approximately 5.8% to 6.8%, together with manganese. It is known as a heat-treatable alloy family used in demanding aerospace environments. Its engineering value comes from its combination of strength, weldability within suitable processes, and useful elevated-temperature performance.
When supplied as wire for precision components, 2219 requires close control of chemistry, surface condition, diameter, and temper. It may be selected for applications involving aerospace structures or assemblies that require predictable behavior during forming and subsequent treatment.
7050 Aluminum Alloy Wire
7050 is a zinc-magnesium-copper aluminum alloy designed for very high strength. The product composition lists zinc at approximately 5.7% to 6.7%, magnesium at approximately 1.9% to 2.6%, and copper at approximately 2.0% to 2.6%. The alloy is associated with highly loaded aerospace structures and other applications where high mechanical performance is required.
The performance of 7050 depends strongly on temper and processing history. In critical applications, designers must evaluate fracture toughness, stress-corrosion resistance, exfoliation corrosion, fatigue behavior, and compatibility with the surrounding structure. The product's emphasis on T73 and T76 conditions reflects the need to consider durability in addition to peak strength.
7075 Aluminum Alloy Wire
7075 is one of the most widely recognized high-strength aluminum alloys. Its primary alloying elements include zinc, magnesium, and copper. The listed ranges are approximately 5.0% to 7.0% zinc, 1.8% to 2.8% magnesium, and 1.4% to 2.0% copper, with chromium and other controlled additions also present.
7075 is attractive when the application requires a high strength-to-weight ratio. It may be used for high-performance structural components, precision parts, and aerospace-related hardware. As with 7050, the alloy temper and environmental requirements must be carefully considered. The highest nominal strength is not always the best choice if the component is exposed to sustained stress, corrosive media, or severe cyclic loading.
Manufacturing Process and Quality Control
The performance of aluminum rivet wire begins with the quality of the raw materials and continues through every manufacturing stage. A modern aluminum wire production system must control chemistry, melting, casting, homogenization, rolling or drawing, heat treatment, surface condition, dimensional accuracy, packaging, and traceability.
Raw Material Selection and Alloy Preparation
Alloy preparation starts with selecting aluminum and alloying additions that meet the target composition. Copper, magnesium, zinc, manganese, silicon, chromium, titanium, zirconium, and other elements must be introduced in controlled quantities. Excessive impurities can reduce ductility, affect corrosion behavior, or create inclusions that interfere with wire drawing and rivet forming.
For high-strength grades, small changes in chemistry may influence precipitation response and final mechanical properties. The manufacturer therefore needs accurate weighing, careful melting practice, appropriate temperature control, and representative sampling. Chemical analysis verifies that the melt is within the designated alloy range before the material moves to the next stage.
Melting, Casting, and Homogenization
During melting, process control is necessary to reduce contamination, hydrogen pickup, oxide formation, and compositional segregation. Proper furnace management and melt treatment help improve the cleanliness and uniformity of the resulting billet or rod.
Casting transforms the molten alloy into a solid form suitable for subsequent processing. The casting method influences grain structure, segregation, porosity, and surface condition. Homogenization may then be applied to reduce chemical non-uniformity and prepare the material for hot working or rolling. A stable internal structure supports more consistent drawing and heat treatment.
Rod Production and Controlled Reduction
After casting and homogenization, the alloy may be processed into rod through controlled forming operations. Reduction schedules must be selected according to the alloy's work-hardening characteristics and the required final wire size. Excessive deformation without suitable intermediate treatment can produce residual stress, cracking, or undesirable texture.
Controlled reduction also affects the wire's mechanical properties. Grain refinement, directional structure, and work hardening influence tensile strength, elongation, bending behavior, and forming response. Production parameters are therefore adjusted according to the target alloy, diameter, temper, and customer specification.
Drawing and Dimensional Control
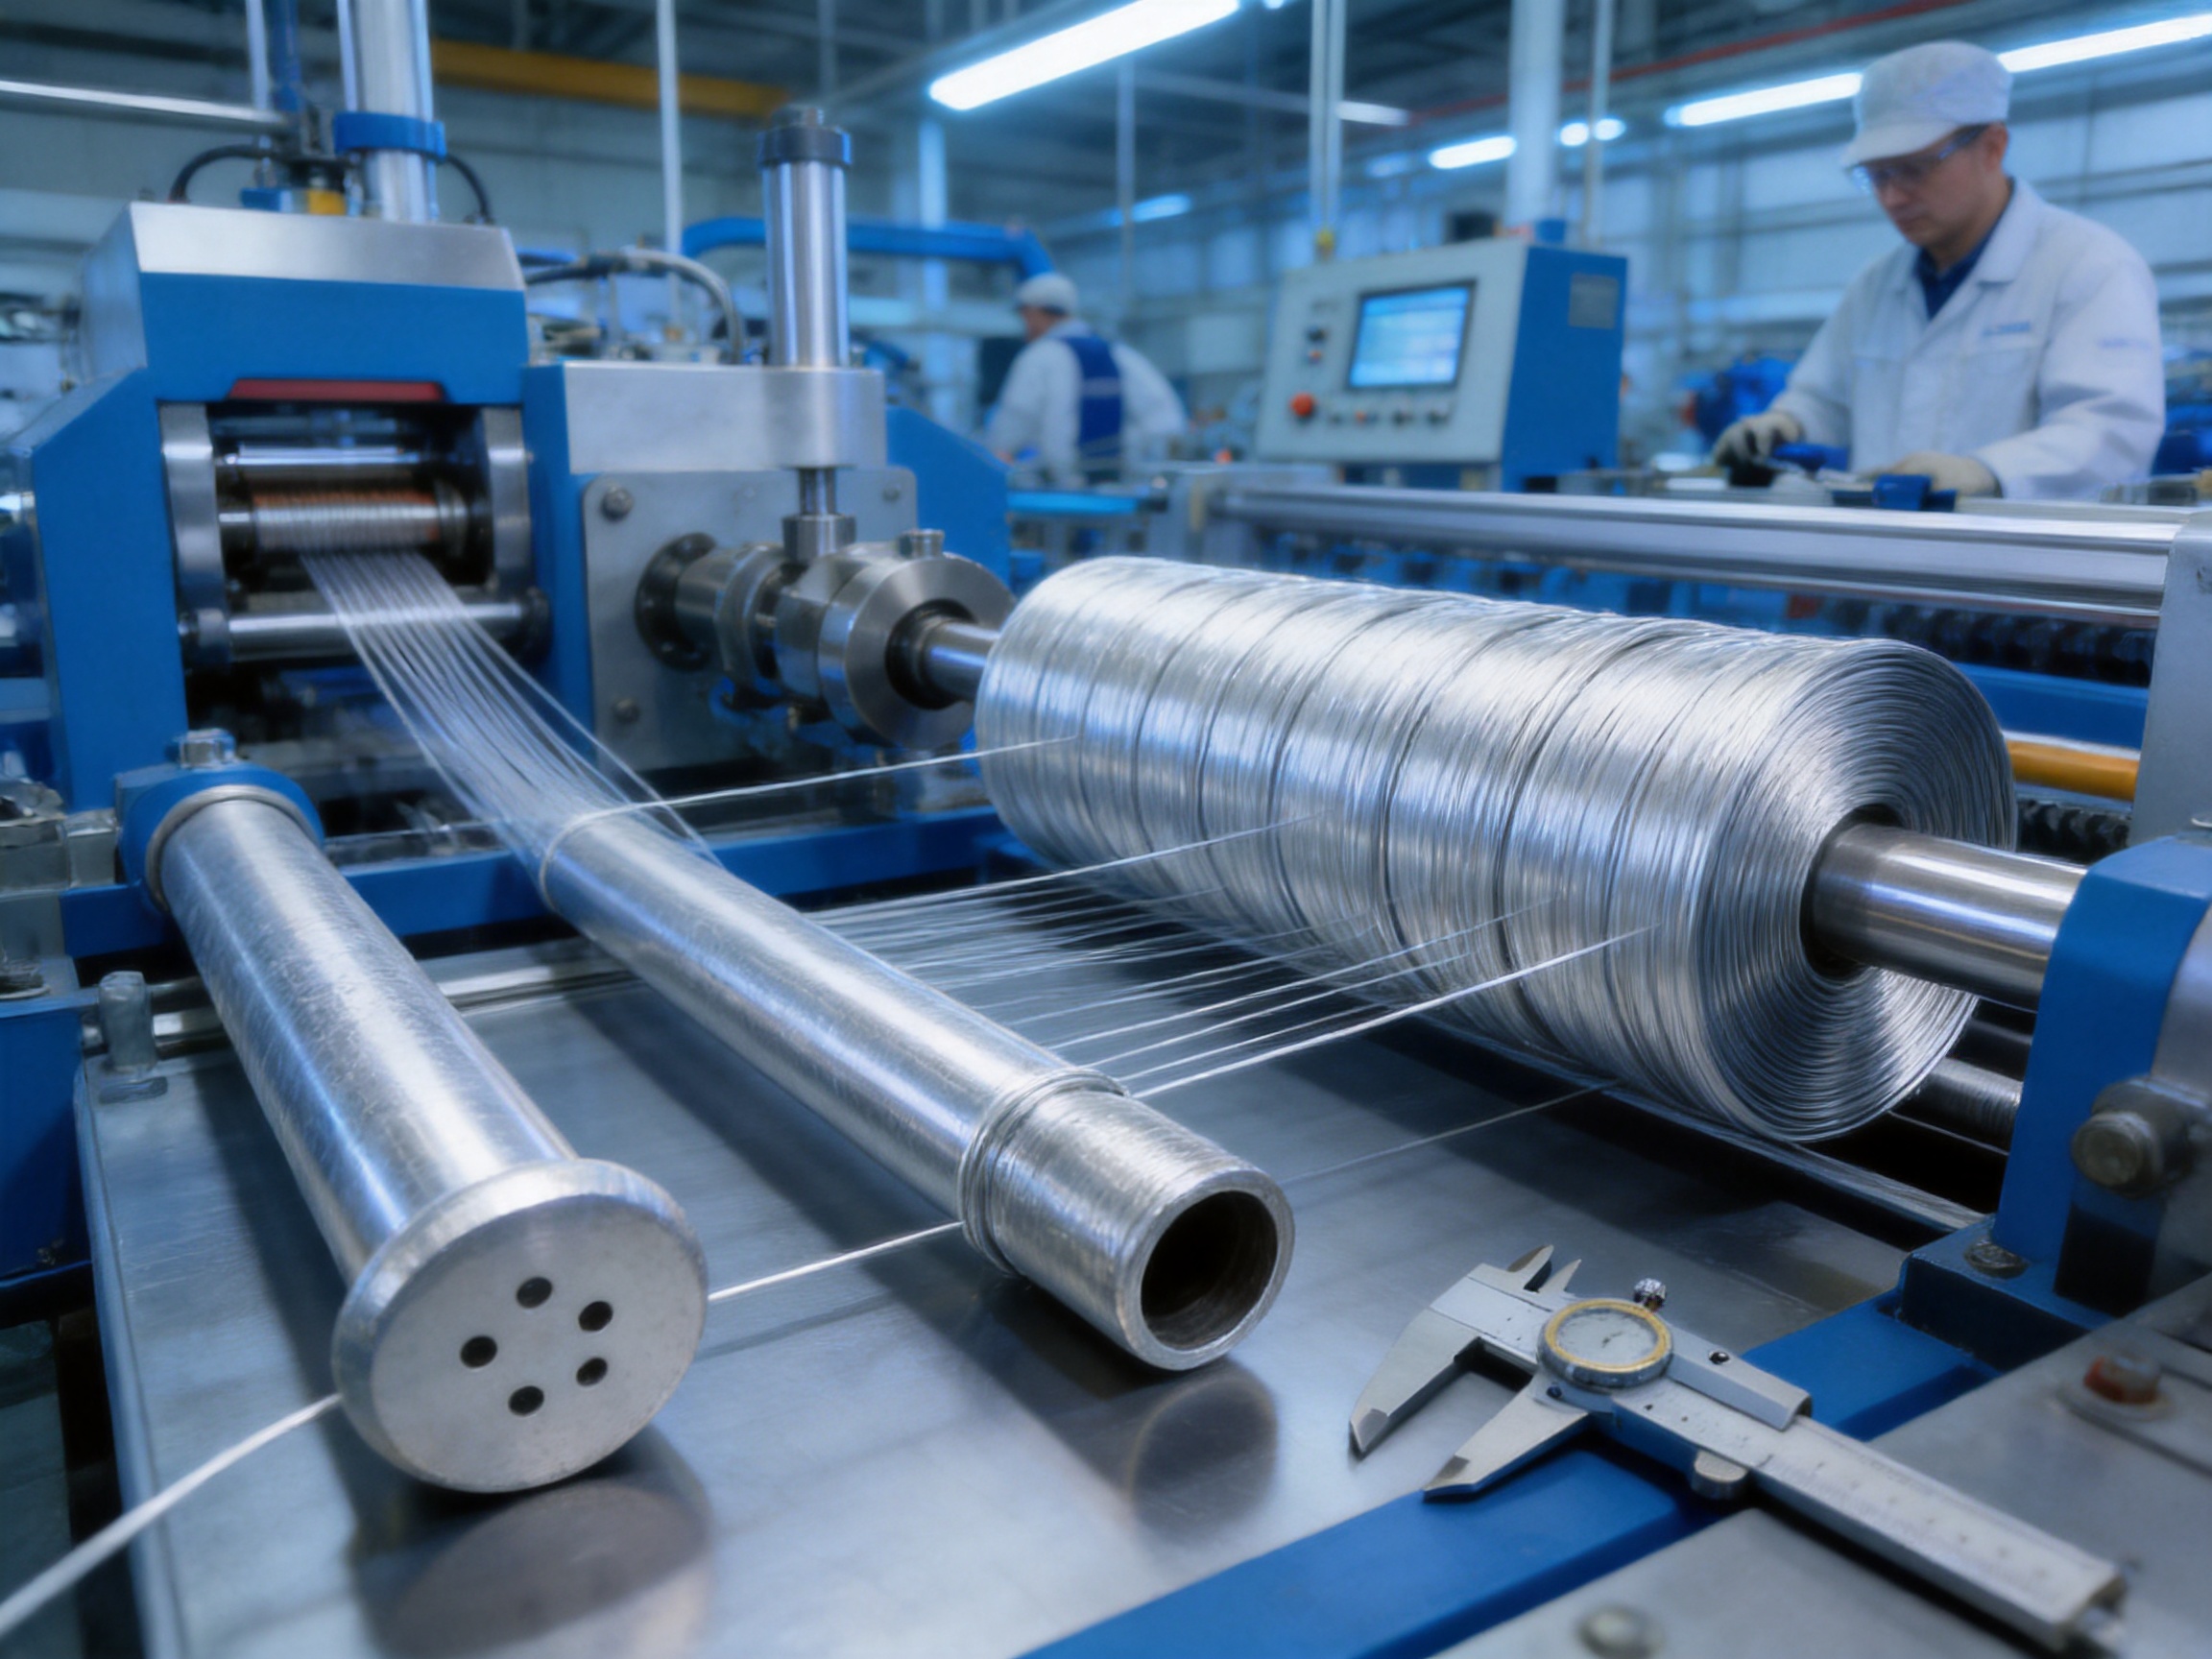
Wire drawing reduces the rod to the required diameter through a series of dies. This stage requires close control of die condition, lubrication, drawing speed, reduction per pass, and intermediate annealing or heat treatment where applicable.
Dimensional consistency is essential for rivet production. Diameter variation can influence the volume of the rivet blank, the final head geometry, insertion force, and joint fit. Advanced manufacturing systems use calibrated measurement tools and inspection routines to identify deviations during production rather than waiting until the finished coil is tested.
Surface quality is equally important. Scratches, laps, seams, oxide deposits, and embedded particles can become initiation points for cracking during heading. A controlled drawing environment and suitable surface management help provide wire that is clean, smooth, and compatible with automated forming equipment.
Heat Treatment and Temper Management
Heat treatment is a central factor in high-strength aluminum alloy wire. Solution treatment, quenching, artificial aging, overaging, or stabilization may be used depending on the alloy and target temper. The purpose is to control the precipitation of strengthening phases and establish the desired balance of strength, ductility, toughness, and corrosion resistance.
The T6 condition generally prioritizes high strength. The T73 condition uses an overaged approach to improve fracture toughness and resistance to stress corrosion and exfoliation corrosion. T76 is designed to provide a combination of elevated strength and improved stress-corrosion performance compared with a conventional T6 condition.
Heat-treatment uniformity is vital. Differences in furnace temperature, material loading, transfer time, quench delay, or aging schedule can lead to variation between coils or within a single batch. Consistent process records and calibrated equipment are therefore necessary for reliable results.
Inspection and Testing
Quality inspection should cover chemical composition, diameter, ovality, surface condition, tensile properties, elongation, hardness, and temper where applicable. Additional tests may be required for aerospace or defense applications, including corrosion testing, metallographic examination, fracture-related evaluation, or batch-specific qualification testing.
Chemical analysis confirms the alloy designation and verifies that key elements remain within the specified ranges. Dimensional inspection confirms that the wire can be fed and formed consistently. Mechanical testing provides evidence that the supplied temper achieves the expected strength and ductility. Surface inspection helps identify conditions that might cause failure during rivet heading.
Traceability connects test results to a specific melt, rod batch, drawing route, heat-treatment cycle, and finished coil. This information supports customer quality systems, root-cause analysis, and long-term supply management.
Advanced Manufacturing Strengths
Integrated Production Capability
An integrated production system can provide better control than a fragmented supply chain in which melting, rod production, drawing, and finishing are performed by unrelated suppliers. When the manufacturer manages multiple stages internally, process information can be shared more efficiently, adjustments can be made faster, and production records can be linked more clearly to the finished product.
The company operates an intelligent manufacturing system covering high-purity aluminum wire, high-strength aluminum alloy wire, aluminum and aluminum alloy welding materials, alloy rods, and precision profiles. This broad capability supports material development across several aluminum alloy families and allows production resources to be matched to different customer requirements.
Specialized Equipment and Process Discipline
High-quality aluminum wire production depends on suitable melting equipment, casting facilities, drawing machines, heat-treatment systems, inspection instruments, and packaging equipment. Advanced machinery alone does not guarantee product quality, but it provides the foundation for stable and repeatable production when combined with trained personnel and documented procedures.
The company reports the use of advanced equipment and facilities, together with quality inspection throughout production. Continuous inspection is important because defects can originate at any stage. Early identification reduces waste, protects downstream equipment, and helps prevent nonconforming material from reaching the customer.
Quality Management Systems
The company has obtained ISO 9001 and IATF 16949 quality management system certifications. ISO 9001 provides a structured framework for quality planning, process control, corrective action, customer communication, and continual improvement. IATF 16949 adds automotive-industry quality requirements, including stronger attention to risk management, traceability, process capability, and defect prevention.
These systems are relevant even when the final application is outside the automotive sector. They encourage systematic process management rather than relying only on final inspection. For high-strength aluminum wire, prevention is particularly valuable because chemistry errors, heat-treatment variation, or internal defects may not always be visible in a simple appearance check.
Technical Personnel and Customer Support
The company employs approximately 60 people, including around 30 professional managers and technicians. Technical personnel play an important role in alloy selection, production planning, drawing schedules, heat-treatment control, test interpretation, and customer communication.
For customized rivet wire, technical cooperation may include reviewing the target alloy, diameter range, delivery condition, surface requirements, packaging method, and documentation. Customers may also require trial batches, sample testing, special tolerances, or production records. A technically capable supplier can help convert these requirements into a practical manufacturing specification.
Application Areas
Aviation and Aerospace
Aviation remains one of the most demanding application areas for aluminum rivet wire. Aircraft structures require lightweight materials that can maintain joint integrity under pressure cycles, vibration, temperature variation, and repeated loading. Rivet wire used in these applications must be compatible with controlled forming operations and approved material systems.
High-strength grades such as 2A10, 2219, 7050, and 7075 may be evaluated for different aerospace purposes. The final selection depends on structural loads, heat-treatment requirements, corrosion protection, compatibility with the parent material, and applicable aerospace specifications.
In addition to new aircraft production, rivet wire may be used for maintenance, repair, and overhaul. Repair organizations require dependable material identification, stable forming behavior, and clear batch documentation. The wire must support repeatable repairs while minimizing the risk of damage to surrounding structure.
Military and Defense Equipment
Defense equipment often operates under harsh environmental and mechanical conditions. Aluminum alloy rivet wire can help reduce weight in vehicles, aircraft, shelters, equipment housings, and structural assemblies. Its corrosion resistance and nonmagnetic characteristics may also be advantageous in selected applications.
Military customers may require special traceability, qualification testing, packaging, and delivery controls. A supplier with documented processes and a broad alloy portfolio can support both standard production and specialized procurement programs.
Transportation and Lightweight Structures
Rail vehicles, buses, commercial vehicles, trailers, and specialized transport equipment increasingly use lightweight aluminum structures. Rivets can join panels, brackets, frames, and interior systems where a permanent mechanical connection is preferred.
Aluminum rivet wire can reduce fastener weight and may simplify joining aluminum components. The selected alloy should be compatible with the surrounding structure and protected against galvanic interaction when dissimilar metals are present.
Industrial Equipment and Fabrication
Industrial equipment manufacturers may use aluminum rivets in enclosures, heat-management systems, machine guards, access panels, and lightweight frames. The required grade may be different from that used in aerospace, and the main priorities may include forming efficiency, corrosion resistance, appearance, or economical high-volume production.
The availability of both high-strength alloy wire and aluminum welding materials allows a supplier to support multiple joining methods within the same industrial program. This can simplify sourcing when a project uses riveted and welded aluminum components together.
How to Select the Correct Rivet Wire
Choosing an aluminum alloy rivet wire requires more than selecting the highest available strength. Engineers should first define the joint load, environmental exposure, forming process, service temperature, inspection requirements, and desired service life.
Define Mechanical Requirements
Important mechanical factors include tensile strength, yield strength, shear performance, elongation, fatigue resistance, fracture toughness, and hardness. The rivet must be strong enough to transfer the expected loads but ductile enough to form without cracking.
For structural aerospace applications, fracture toughness and fatigue performance may be more important than a small increase in nominal tensile strength. For less demanding assemblies, a more formable grade may improve production efficiency and reduce tooling wear.
Evaluate Environmental Conditions
Moisture, salt spray, temperature, chemicals, and sustained tensile stress can affect alloy selection. A grade with excellent strength in a laboratory environment may not be the most suitable choice for a corrosive service environment. T73 and T76 conditions may be considered where stress-corrosion and exfoliation-corrosion resistance are important.
Confirm Forming and Heat-Treatment Requirements
Customers should identify whether the rivet will be formed in the supplied condition or whether it will receive additional solution treatment and aging after forming. The wire temper, diameter, and storage conditions must be compatible with the planned process.
Some rivets are installed shortly after manufacturing, while others may be stored before use. Storage time and temperature can influence the material condition of certain heat-treatable alloys. Clear documentation between the wire supplier, rivet manufacturer, and end user helps avoid unexpected changes in forming behavior.
Review Dimensional and Surface Specifications
Diameter tolerance, ovality, straightness, coil size, surface finish, and packaging should be included in the purchasing specification. Automated forming lines may require narrower tolerances than manual operations. Surface cleanliness is especially important where the wire will be cut and headed at high speed.
Request Complete Documentation
For high-performance applications, customers should request a material certificate, chemical analysis, mechanical test results, temper information, batch identification, and inspection records. Additional documents may include quality certificates, packaging details, compliance statements, and manufacturing traceability.
Packaging, Storage, and Handling
Even high-quality wire can be damaged by unsuitable storage or handling. Aluminum wire should be protected from moisture, dirt, impact, and contamination during transport. Packaging should prevent coil deformation and protect the surface from scratches caused by contact with hard materials.
Storage areas should be clean, dry, and maintained at stable conditions where possible. Sudden temperature changes can produce condensation on cold metal surfaces. If moisture becomes trapped between coils or within packaging, staining and corrosion may occur. Materials should be allowed to reach the storage environment gradually before packaging is opened.
Operators should use clean gloves and suitable lifting equipment when handling precision wire. Contact with steel particles, oils, salts, or corrosive chemicals should be avoided. Coils should be clearly identified so that alloy and temper are not mixed during production.
First-in, first-out inventory control can help manage storage duration, particularly for heat-treatable materials whose condition may change over time. Customers should follow the supplier's recommendations regarding shelf life, refrigeration, natural aging, or pre-installation treatment where applicable.
Competitive Value for Global Buyers
The main competitive advantage of this aluminum rivet wire program is the combination of alloy breadth, manufacturing capability, process control, and application knowledge. Customers can evaluate high-strength grades for rivets while also sourcing high-purity aluminum wire and aluminum alloy welding materials from a manufacturer with related technical capabilities.
A broad product range can reduce the need to coordinate multiple suppliers for different aluminum joining requirements. It may also support standardization across projects, particularly when an engineering group uses high-strength fastening wire, welding wire, and precision aluminum products in the same supply chain.
The company's location in Jiangsu Province provides access to China's manufacturing and logistics networks. Its products are reported to be exported to high-end overseas markets, indicating experience with international customer requirements, documentation, packaging, and shipment coordination.
Customization is another important value point. Aluminum wire customers may require special diameters, alloy grades, temper conditions, coil weights, packaging formats, or inspection documents. A manufacturer with internal technical and production resources can review these requirements and develop a practical supply plan rather than offering only a limited standard catalog.
Cost competitiveness should also be considered over the full production cycle. Stable wire quality can reduce rivet-forming scrap, tool adjustments, machine downtime, inspection failures, and customer complaints. The lowest purchase price is not always the lowest total cost if inconsistent material causes production interruptions.
Recommended Purchasing Checklist
Before placing an order for aluminum alloy rivet wire, the buyer should prepare a clear technical specification. The following points are recommended:
1. Required alloy designation, such as 2A10, 2219, 7050, or 7075.
2. Required temper or delivery condition, including whether the wire will be formed before or after heat treatment.
3. Finished wire diameter, dimensional tolerance, and allowable ovality.
4. Mechanical property requirements, including tensile strength, yield strength, elongation, and hardness where applicable.
5. Surface requirements, including cleanliness, allowable marks, and protection against contamination.
6. Coil or spool dimensions, total weight, inner diameter, outer diameter, and packaging method.
7. Chemical composition documentation and batch traceability.
8. Required inspection reports, certificates, and quality-system documentation.
9. Application environment, including temperature, humidity, salt exposure, chemicals, and sustained stress.
10. Delivery schedule, sample requirements, production approval process, and after-sales technical support.
A complete specification helps the manufacturer select suitable processing conditions and reduces misunderstandings during production. It also enables the customer to compare suppliers on technical performance rather than price alone.
Quality and Sustainability Considerations
Aluminum is valued for its combination of low density, recyclability, and long service life. A durable aluminum rivet can remain in service for many years, reducing the need for replacement and conserving maintenance resources. Lightweight structures can also reduce energy consumption during transportation and operation.
Responsible manufacturing requires control of energy use, material yield, process waste, emissions, and recycling streams. Drawing scrap, offcuts, and rejected material may be returned to appropriate recycling channels when chemistry and contamination controls permit. Maintaining high process capability is itself a sustainability measure because it reduces scrap and prevents unnecessary remanufacturing.
Long-term sustainability also depends on correct alloy selection. Using a material that is stronger, more corrosion resistant, or more durable than necessary may increase cost and processing demands. Using a material that is too weak or poorly suited to the environment can cause premature failure and replacement. Engineering evaluation should therefore balance performance, service life, manufacturability, and resource efficiency.
Q&A: Aluminum Alloy Wire for Rivets
What is aluminum alloy rivet wire used for?
It is used to manufacture rivets for aviation, aerospace, military equipment, transportation structures, industrial assemblies, and other applications requiring lightweight permanent fastening. The wire is cut into blanks and formed into rivets through controlled heading or upsetting operations.
Which alloys are available for high-strength rivet applications?
The product information identifies 2A10, 2219, 7050, and 7075 as important high-strength aluminum alloy options. The best choice depends on the required strength, corrosion resistance, toughness, forming behavior, temper, and applicable customer or industry specification.
Why are T6, T73, and T76 conditions important?
T6 is generally associated with high strength. T73 provides relatively high fracture toughness and improved resistance to stress corrosion and exfoliation corrosion. T76 is described as offering higher strength than T73 while maintaining higher stress-corrosion resistance than T6. The correct condition should be selected according to the complete service environment.
Is 7075 always the best alloy for rivets?
No. 7075 provides high strength-to-weight performance, but maximum strength is not the only design requirement. Formability, fracture toughness, corrosion resistance, heat-treatment response, joint design, and installation conditions must also be considered. Another alloy or temper may provide a better overall balance.
Can the wire be customized?
Customization may be available for alloy, diameter, temper, packaging, coil weight, surface requirements, and inspection documentation. Customers should provide a detailed technical specification so the manufacturer can confirm feasibility and establish suitable production conditions.
What quality documents should buyers request?
Buyers may request chemical composition results, mechanical test reports, dimensional inspection records, heat-treatment information, batch traceability, material certificates, and quality-system documentation. Aerospace and defense projects may require additional qualification or compliance records.
How does wire quality affect rivet production?
Wire diameter, surface condition, internal cleanliness, microstructure, and temper influence cutting, feeding, heading, dimensional accuracy, and cracking resistance. Consistent wire quality can reduce forming defects, machine interruptions, tooling wear, and production scrap.
Can these products support welding applications as well as riveting?
The wider product range includes aluminum and aluminum alloy welding materials such as 4043, 4047, 5183, 5154, 5356, AlMg3, AlMg5, and AlMg6. These grades serve different joining requirements and should not be substituted for high-strength rivet alloys without technical evaluation.
Where is the manufacturer located?
Jiangsu Hetuo Aluminum Wire Co., Ltd. is located in the Small and Medium-sized Enterprises Park, Economic Development Zone, Guannan County, Lianyungang City, Jiangsu Province, China.
How should aluminum alloy wire be stored?
The wire should be stored in a clean, dry area and protected from moisture, condensation, impact, dirt, and contact with dissimilar contaminants. Coils should remain identified by alloy and temper, and handling should be performed carefully to prevent surface damage.
Conclusion
High-strength aluminum alloy wire for rivets provides an effective solution for lightweight, durable, and precision fastening. Its advantages include low density, high specific strength, corrosion-resistance options, forming capability, and compatibility with automated rivet production. These characteristics make it especially valuable in aviation, aerospace, military, transportation, and advanced industrial applications.
The available alloy portfolio includes 2A10, 2219, 7050, and 7075 for high-strength requirements, together with aluminum-magnesium and aluminum-silicon grades for welding and related joining processes. T6, T73, and T76 conditions allow users to select a performance balance suited to strength, toughness, and corrosion resistance.
Reliable performance depends on more than alloy designation. Controlled melting, accurate composition, stable casting, appropriate homogenization, precise drawing, consistent heat treatment, surface management, dimensional inspection, and complete traceability are all essential. The manufacturer's 40,000-square-meter facility, technical personnel, advanced equipment, ISO 9001 and IATF 16949 certifications, and broad aluminum wire capabilities provide a strong foundation for customized supply.
For buyers, the best purchasing decision should be based on total application requirements rather than nominal strength alone. By coordinating alloy, temper, diameter, forming method, environment, packaging, and documentation, users can obtain aluminum rivet wire that supports reliable production and long service life.
References
1. Aluminum Association. Aluminum Standards and Data.
2. ASTM International. Standards for Aluminum and Aluminum-Alloy Products, Chemical Composition, and Mechanical Testing.
3. SAE International. Aerospace Material Specifications for Aluminum Alloy Products and Fasteners.
4. ASM International. Aluminum and Aluminum Alloys: Properties, Processing, and Applications.
5. ISO 9001. Quality Management Systems Requirements.
6. IATF 16949. Quality Management System Requirements for Automotive Production and Relevant Service Parts Organizations.
7. Product technical information supplied for high-strength aluminum alloy wire, aluminum rivet wire, and aluminum alloy welding materials.