

 English
 中文简体
 русский
 Deutsch
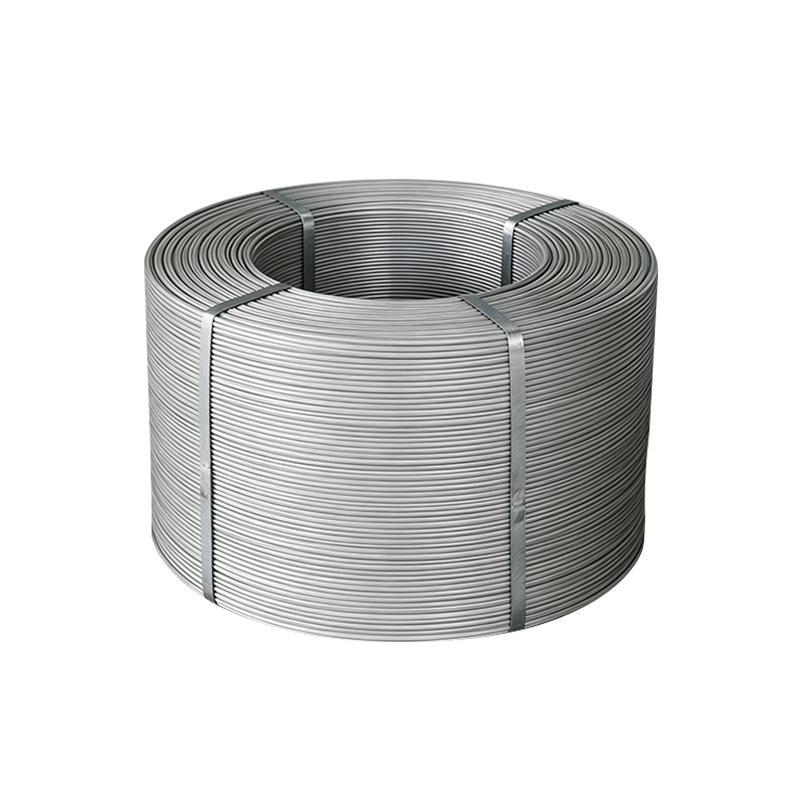
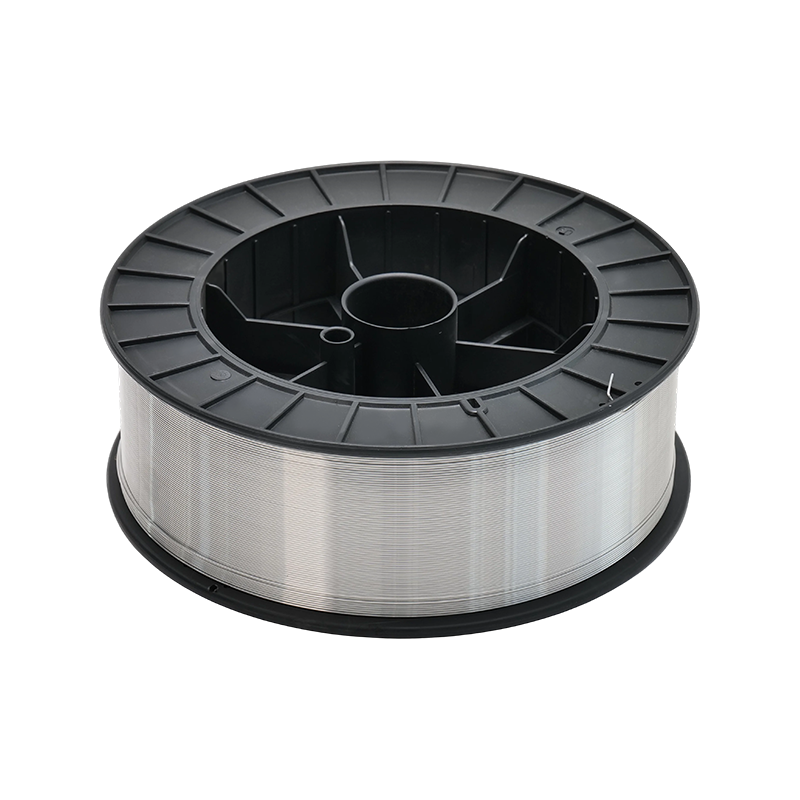
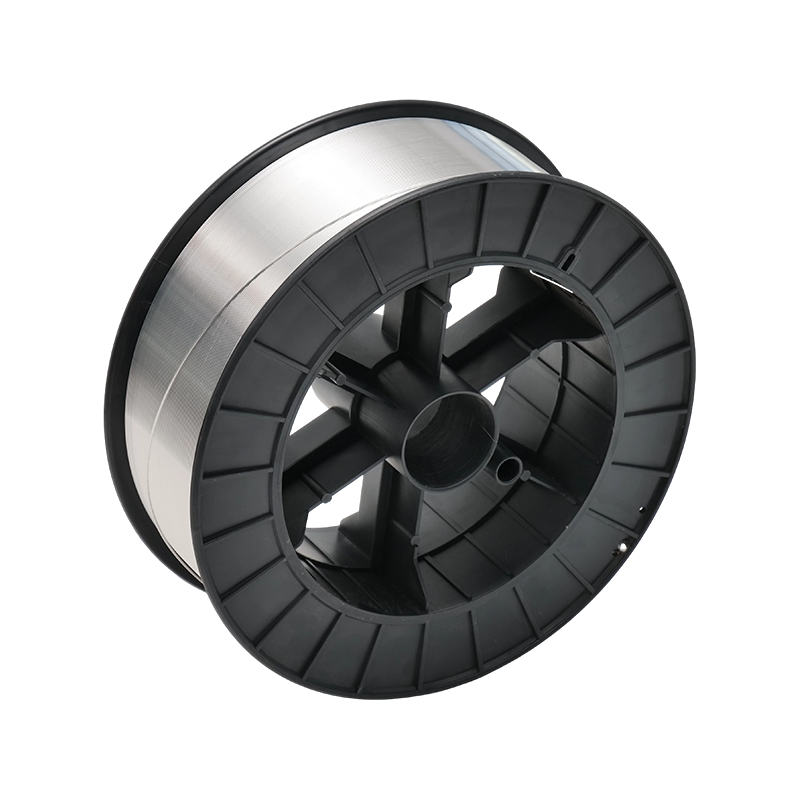
Tungsten inert gas welding, commonly known as TIG welding, is valued for its precision, cleanliness, and ability to produce highly controlled welds. When aluminum or aluminum alloys are involved, the choice of filler material has a direct influence on weld appearance, joint strength, corrosion resistance, process stability, and production efficiency. TIG wire is designed to support non-consumable tungsten electrode welding under an inert argon atmosphere, allowing fabricators to add carefully controlled filler metal where joint design, material thickness, or service requirements demand it.
For manufacturers working with aluminum structures, precision profiles, fabricated components, transportation equipment, pressure-related assemblies, and general industrial products, a reliable TIG wire is more than a consumable. It is an important part of the complete welding system. The filler wire must be clean, dimensionally consistent, metallurgically suitable, and easy for the operator or wire-feeding equipment to handle. Variations in surface condition, diameter, straightness, or alloy chemistry can affect arc behavior and may lead to porosity, lack of fusion, cracking, excessive spatter, or an unattractive weld profile.
Jiangsu Hetuo Aluminum Wire Co., Ltd. produces aluminum and aluminum alloy welding materials for industrial users that require dependable quality and consistent supply. Established in 2019, the company has developed an intelligent manufacturing system covering high-purity aluminum wire, high-strength aluminum alloy wire, and aluminum and aluminum alloy welding materials. Its TIG wire is mainly used for non-melting electrode argon arc welding and is manufactured within a production organization focused on process control, inspection, and customer-oriented technical support.
The combination of aluminum material expertise, modern production equipment, systematic quality management, and a dedicated manufacturing site enables the product to serve applications where welding consistency is essential. This article examines the characteristics of TIG wire, its role in aluminum welding, the manufacturing strengths behind a reliable product, and the factors buyers should consider when selecting a supplier.
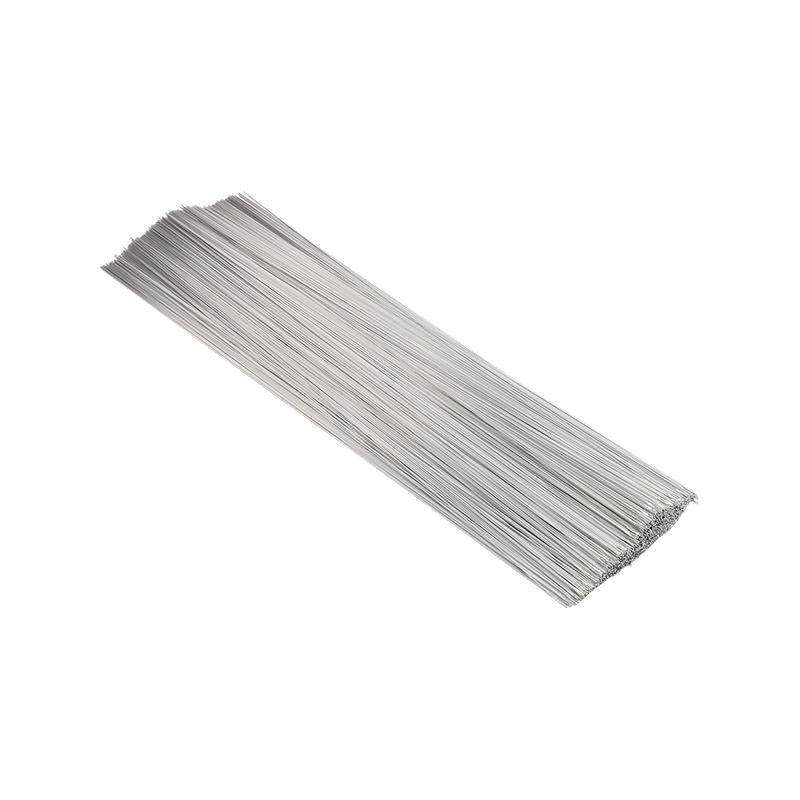
TIG Wire
Content
- 1 Understanding TIG Wire in Aluminum Welding
- 2 Key Advantages of High-Quality TIG Wire
- 3 Manufacturing Strengths Behind the Product
- 4 Production Environment and Organizational Capacity
- 5 Technical Considerations When Selecting TIG Wire
- 6 Comparison with Less Specialized Alternatives
- 7 Applications for Aluminum TIG Wire
- 8 Recommended Welding Practices
- 9 Customer-Oriented Supply and Technical Support
- 10 Why Choose a Specialized Manufacturer
- 11 Purchasing Checklist for TIG Wire
- 12 Frequently Asked Questions
- 12.1 What is TIG wire used for?
- 12.2 Is TIG wire the same as a tungsten electrode?
- 12.3 Why is surface cleanliness important for aluminum TIG wire?
- 12.4 How do I select the correct aluminum TIG wire?
- 12.5 Can TIG wire be used for automated welding?
- 12.6 What advantages does a specialized aluminum wire manufacturer provide?
- 12.7 What quality systems support this TIG wire?
- 12.8 Where is the manufacturer located?
- 12.9 How can customers contact the manufacturer?
- 12.10 What should be done with opened wire that has been exposed to moisture?
- 13 Conclusion
- 14 References
- 15 Product: TIG Wire
Understanding TIG Wire in Aluminum Welding
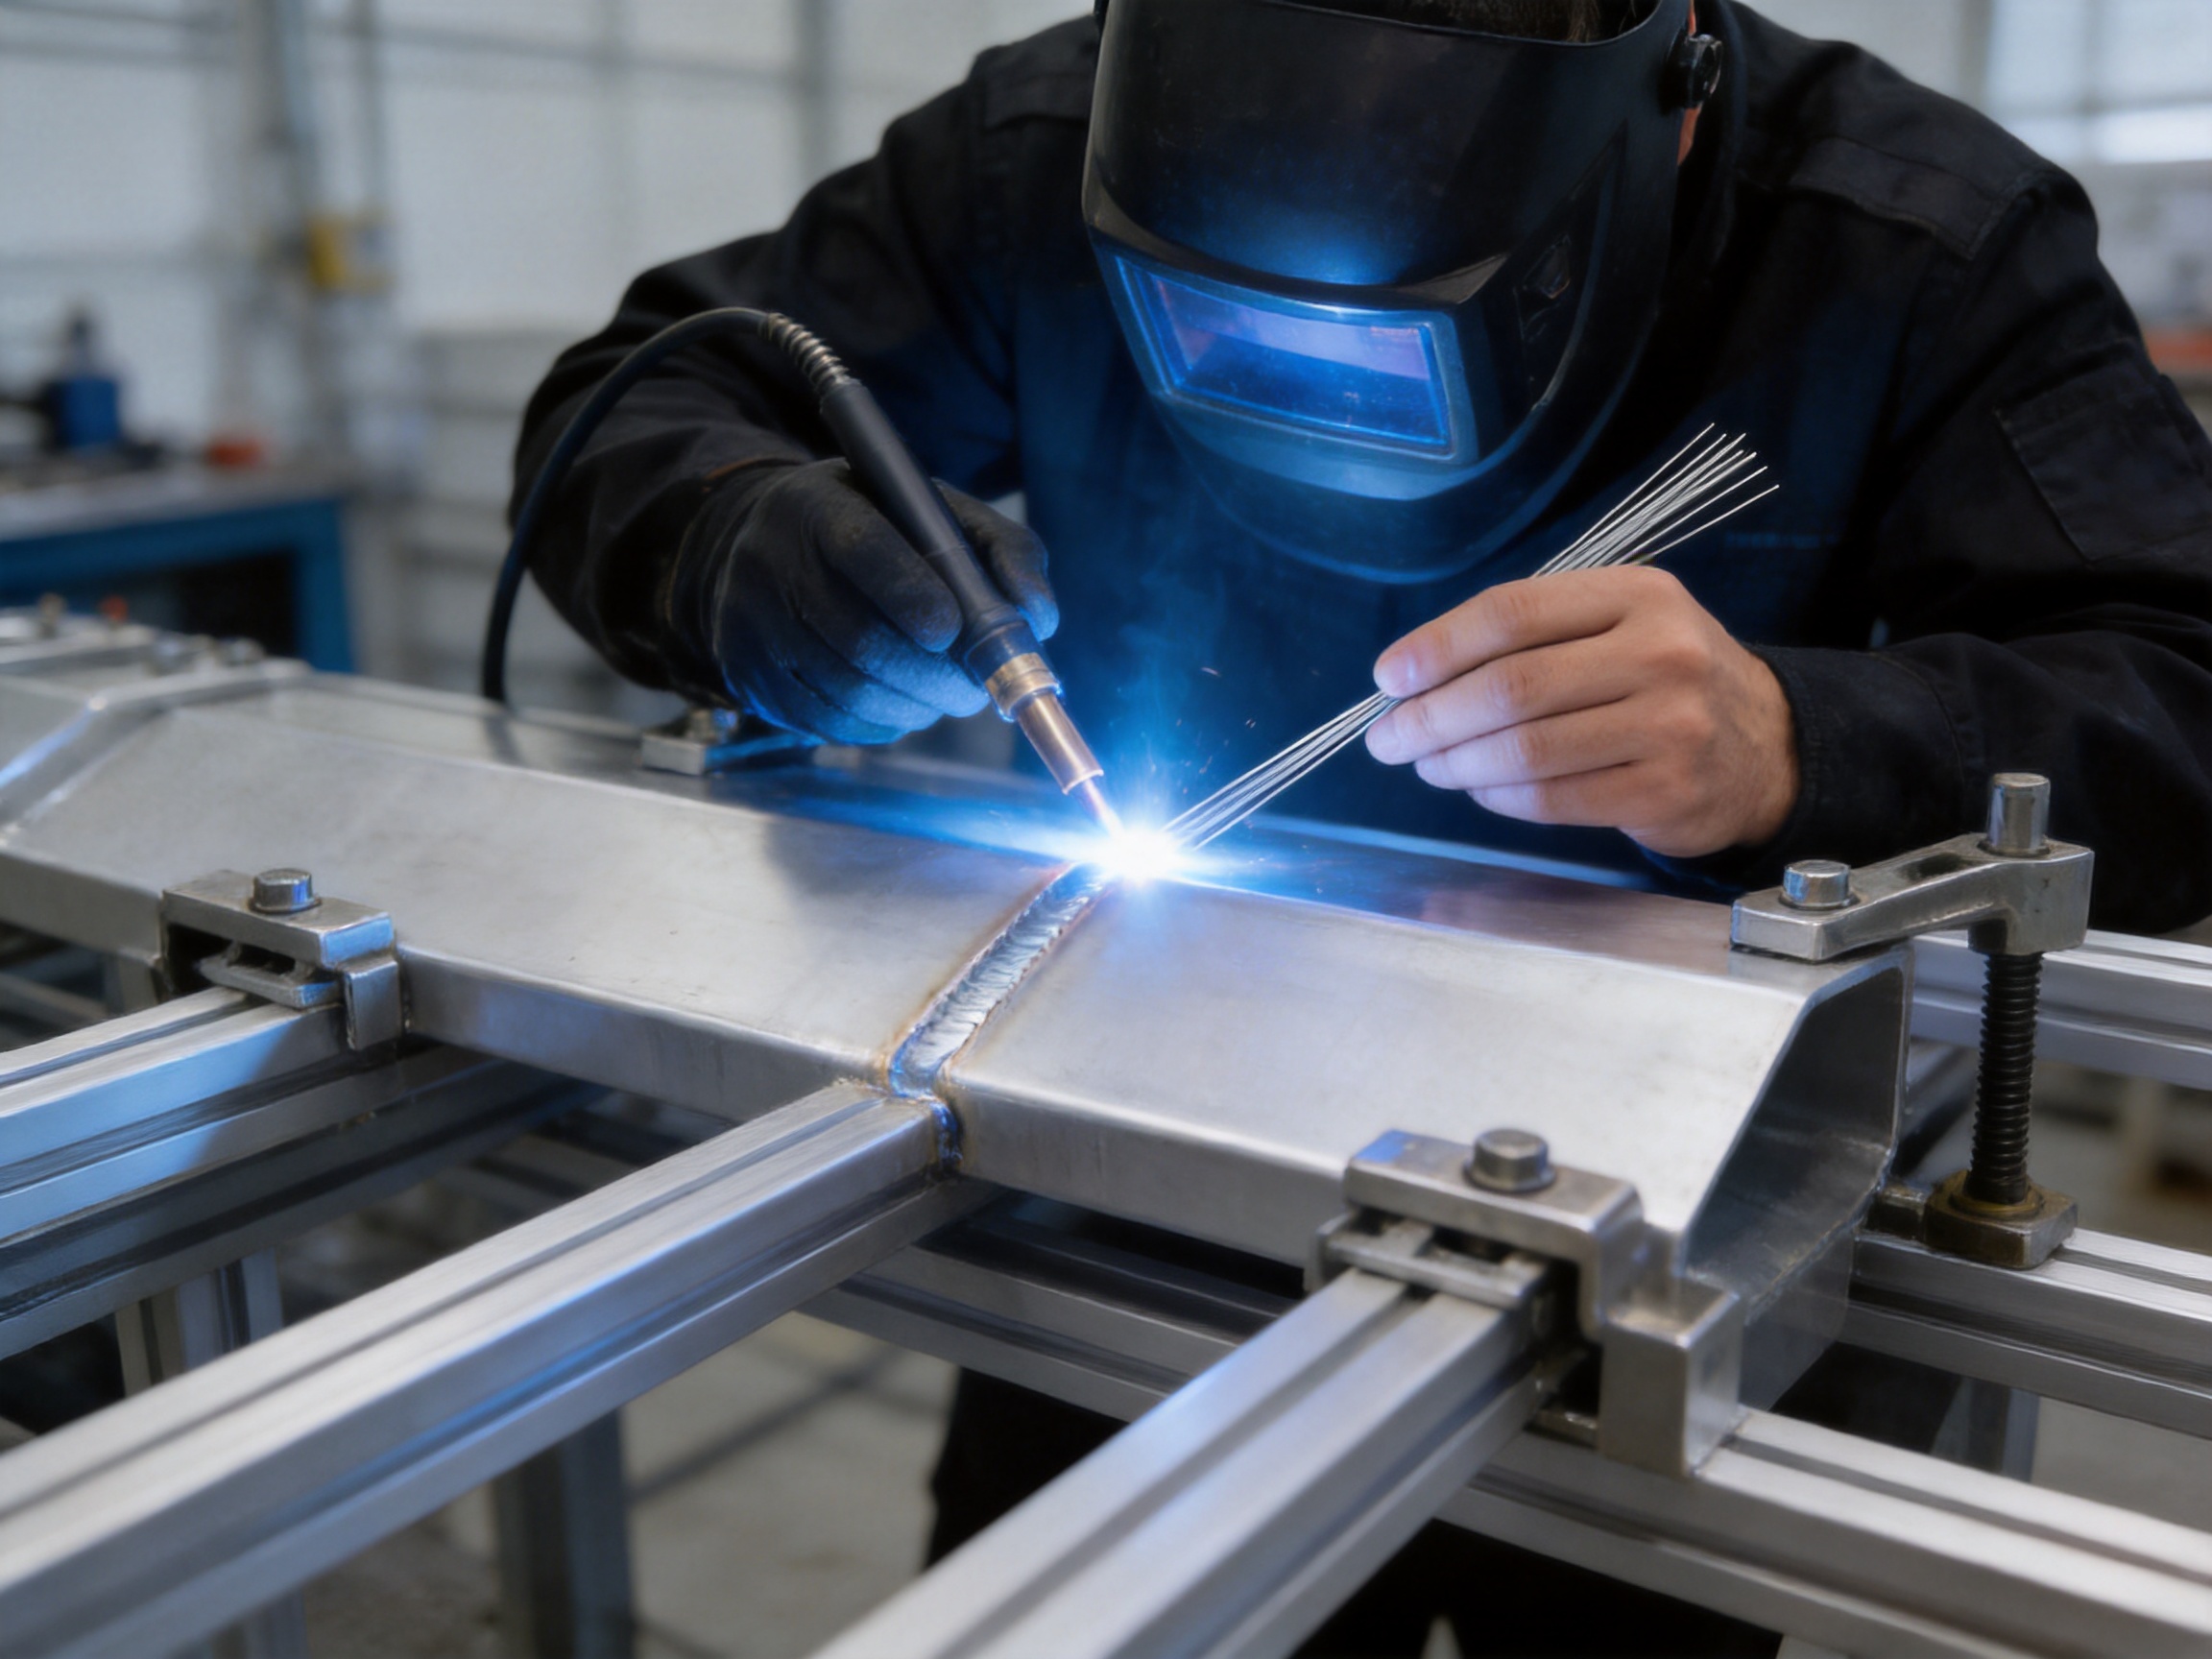
TIG welding uses a non-consumable tungsten electrode to establish and maintain the arc. Shielding gas, generally argon or an argon-based mixture, protects the molten weld pool from atmospheric oxygen, nitrogen, and moisture. Unlike processes in which the electrode itself continuously melts into the weld, the tungsten electrode remains separate from the filler metal. The operator introduces TIG wire manually or through a controlled feeding system into the weld pool.
This operating principle provides excellent control over heat input and filler addition. It is particularly useful for aluminum because aluminum components often require careful management of thermal expansion, oxide removal, joint fit-up, and solidification behavior. The operator can add small amounts of filler wire precisely when required, helping to control bead size and reduce unnecessary heat accumulation.
TIG wire may be used to join aluminum components, repair cast or fabricated parts, build up worn areas, fill gaps, complete corner joints, or create smooth, visually consistent welds. It is suitable for both manual fabrication and applications supported by mechanized or automated equipment, provided that the selected wire is compatible with the base material and the welding procedure.
Why aluminum requires carefully selected filler wire
Aluminum has several characteristics that make welding different from welding carbon steel or stainless steel. It conducts heat rapidly, has a relatively low melting temperature compared with many steels, and forms a tenacious oxide layer on its surface. The oxide layer melts at a significantly higher temperature than the aluminum beneath it. As a result, the welding system must provide sufficient cleaning action, appropriate alternating-current settings where applicable, and a filler wire that melts and flows consistently.
Aluminum also expands significantly when heated. Poor control of joint preparation, preheating, torch movement, or filler addition can contribute to distortion and residual stress. The weld metal must solidify in a way that supports the required joint performance. Depending on the base alloy and service environment, the filler selection may influence crack sensitivity, ductility, strength, corrosion behavior, and appearance.
A high-quality TIG wire supports the welding operator by providing a stable and predictable addition of metal. When wire diameter and surface condition remain consistent, the operator can maintain a more uniform feeding rhythm. This improves control of the weld pool and helps reduce process variation between operators, shifts, and production batches.
Key Advantages of High-Quality TIG Wire
The performance of TIG wire depends on more than the nominal alloy designation. Product quality includes chemical consistency, cleanliness, dimensional accuracy, surface condition, packaging, traceability, and the supplier’s ability to maintain repeatable manufacturing conditions. The following advantages are especially important in professional aluminum welding.
Consistent arc and weld-pool behavior
Uniform filler wire allows the operator to introduce metal at a predictable rate. Inconsistent diameter can create irregular melting behavior and force the operator to adjust hand movement or current settings. A controlled wire diameter supports a smoother relationship between arc energy, filler addition, and travel speed.
Surface cleanliness is equally important. Oil, moisture, dust, metal fines, and other contaminants may become sources of porosity or inclusions. Clean TIG wire helps the shielding system perform effectively and reduces the chance that unwanted substances will enter the weld pool. This is particularly valuable in applications where the finished weld must meet demanding appearance or inspection requirements.
Improved weld appearance
TIG welding is frequently selected when appearance matters. Components may remain visible after fabrication, or the weld may need to meet a defined visual standard before finishing, anodizing, painting, or assembly. Consistent TIG wire can contribute to an even bead profile, controlled reinforcement, and a clean transition between filler metal and base material.
A good appearance is not merely cosmetic. A smooth and well-controlled weld profile can reduce sharp transitions, simplify subsequent finishing, and make visual inspection easier. It may also help identify surface discontinuities at an early stage. The final appearance still depends on operator skill, joint preparation, shielding gas coverage, torch technique, and equipment settings, but the filler wire remains an important part of the result.
Reliable feeding and handling
In manual TIG welding, the filler wire must be easy to hold, cut, and introduce into the weld pool. In mechanized systems, dimensional consistency and surface quality become even more important because the wire may pass through guides, feeders, or delivery systems. Straight and properly packaged wire helps reduce feeding interruptions and handling damage.
Reliable handling also improves workplace efficiency. Operators spend less time sorting, correcting, or rejecting wire that is bent, contaminated, or inconsistently packaged. When the product is supplied in a format appropriate to the user’s process, material preparation becomes more efficient and production planning becomes easier.
Support for high-integrity joints
Welding quality is influenced by the interaction between the base metal, filler metal, shielding gas, and procedure. Properly manufactured TIG wire helps the welding team work toward sound joints with suitable strength and ductility. It can support the production of welds that are easier to inspect and less likely to display avoidable defects caused by filler inconsistency.
For critical applications, filler wire should be incorporated into a documented welding procedure. The user should verify compatibility with the base alloy, joint design, service temperature, corrosion conditions, and applicable standards. A responsible supplier supports this process by maintaining controlled production and providing product information that allows users to identify and manage the material correctly.
Reduced rework and material waste
Rework is costly because it consumes labor, electricity, shielding gas, filler metal, inspection resources, and production time. Weld defects may also damage the base component if excessive grinding or repair is required. Consistent TIG wire can help reduce process variability and support first-pass quality, especially when combined with correct storage and qualified welding procedures.
Lower waste is also relevant to sustainability. Aluminum is highly recyclable, but unnecessary scrap still represents energy and resource consumption. A stable welding consumable contributes to more efficient use of raw materials and supports manufacturers seeking lighter, stronger, and more sustainable material solutions.
Manufacturing Strengths Behind the Product
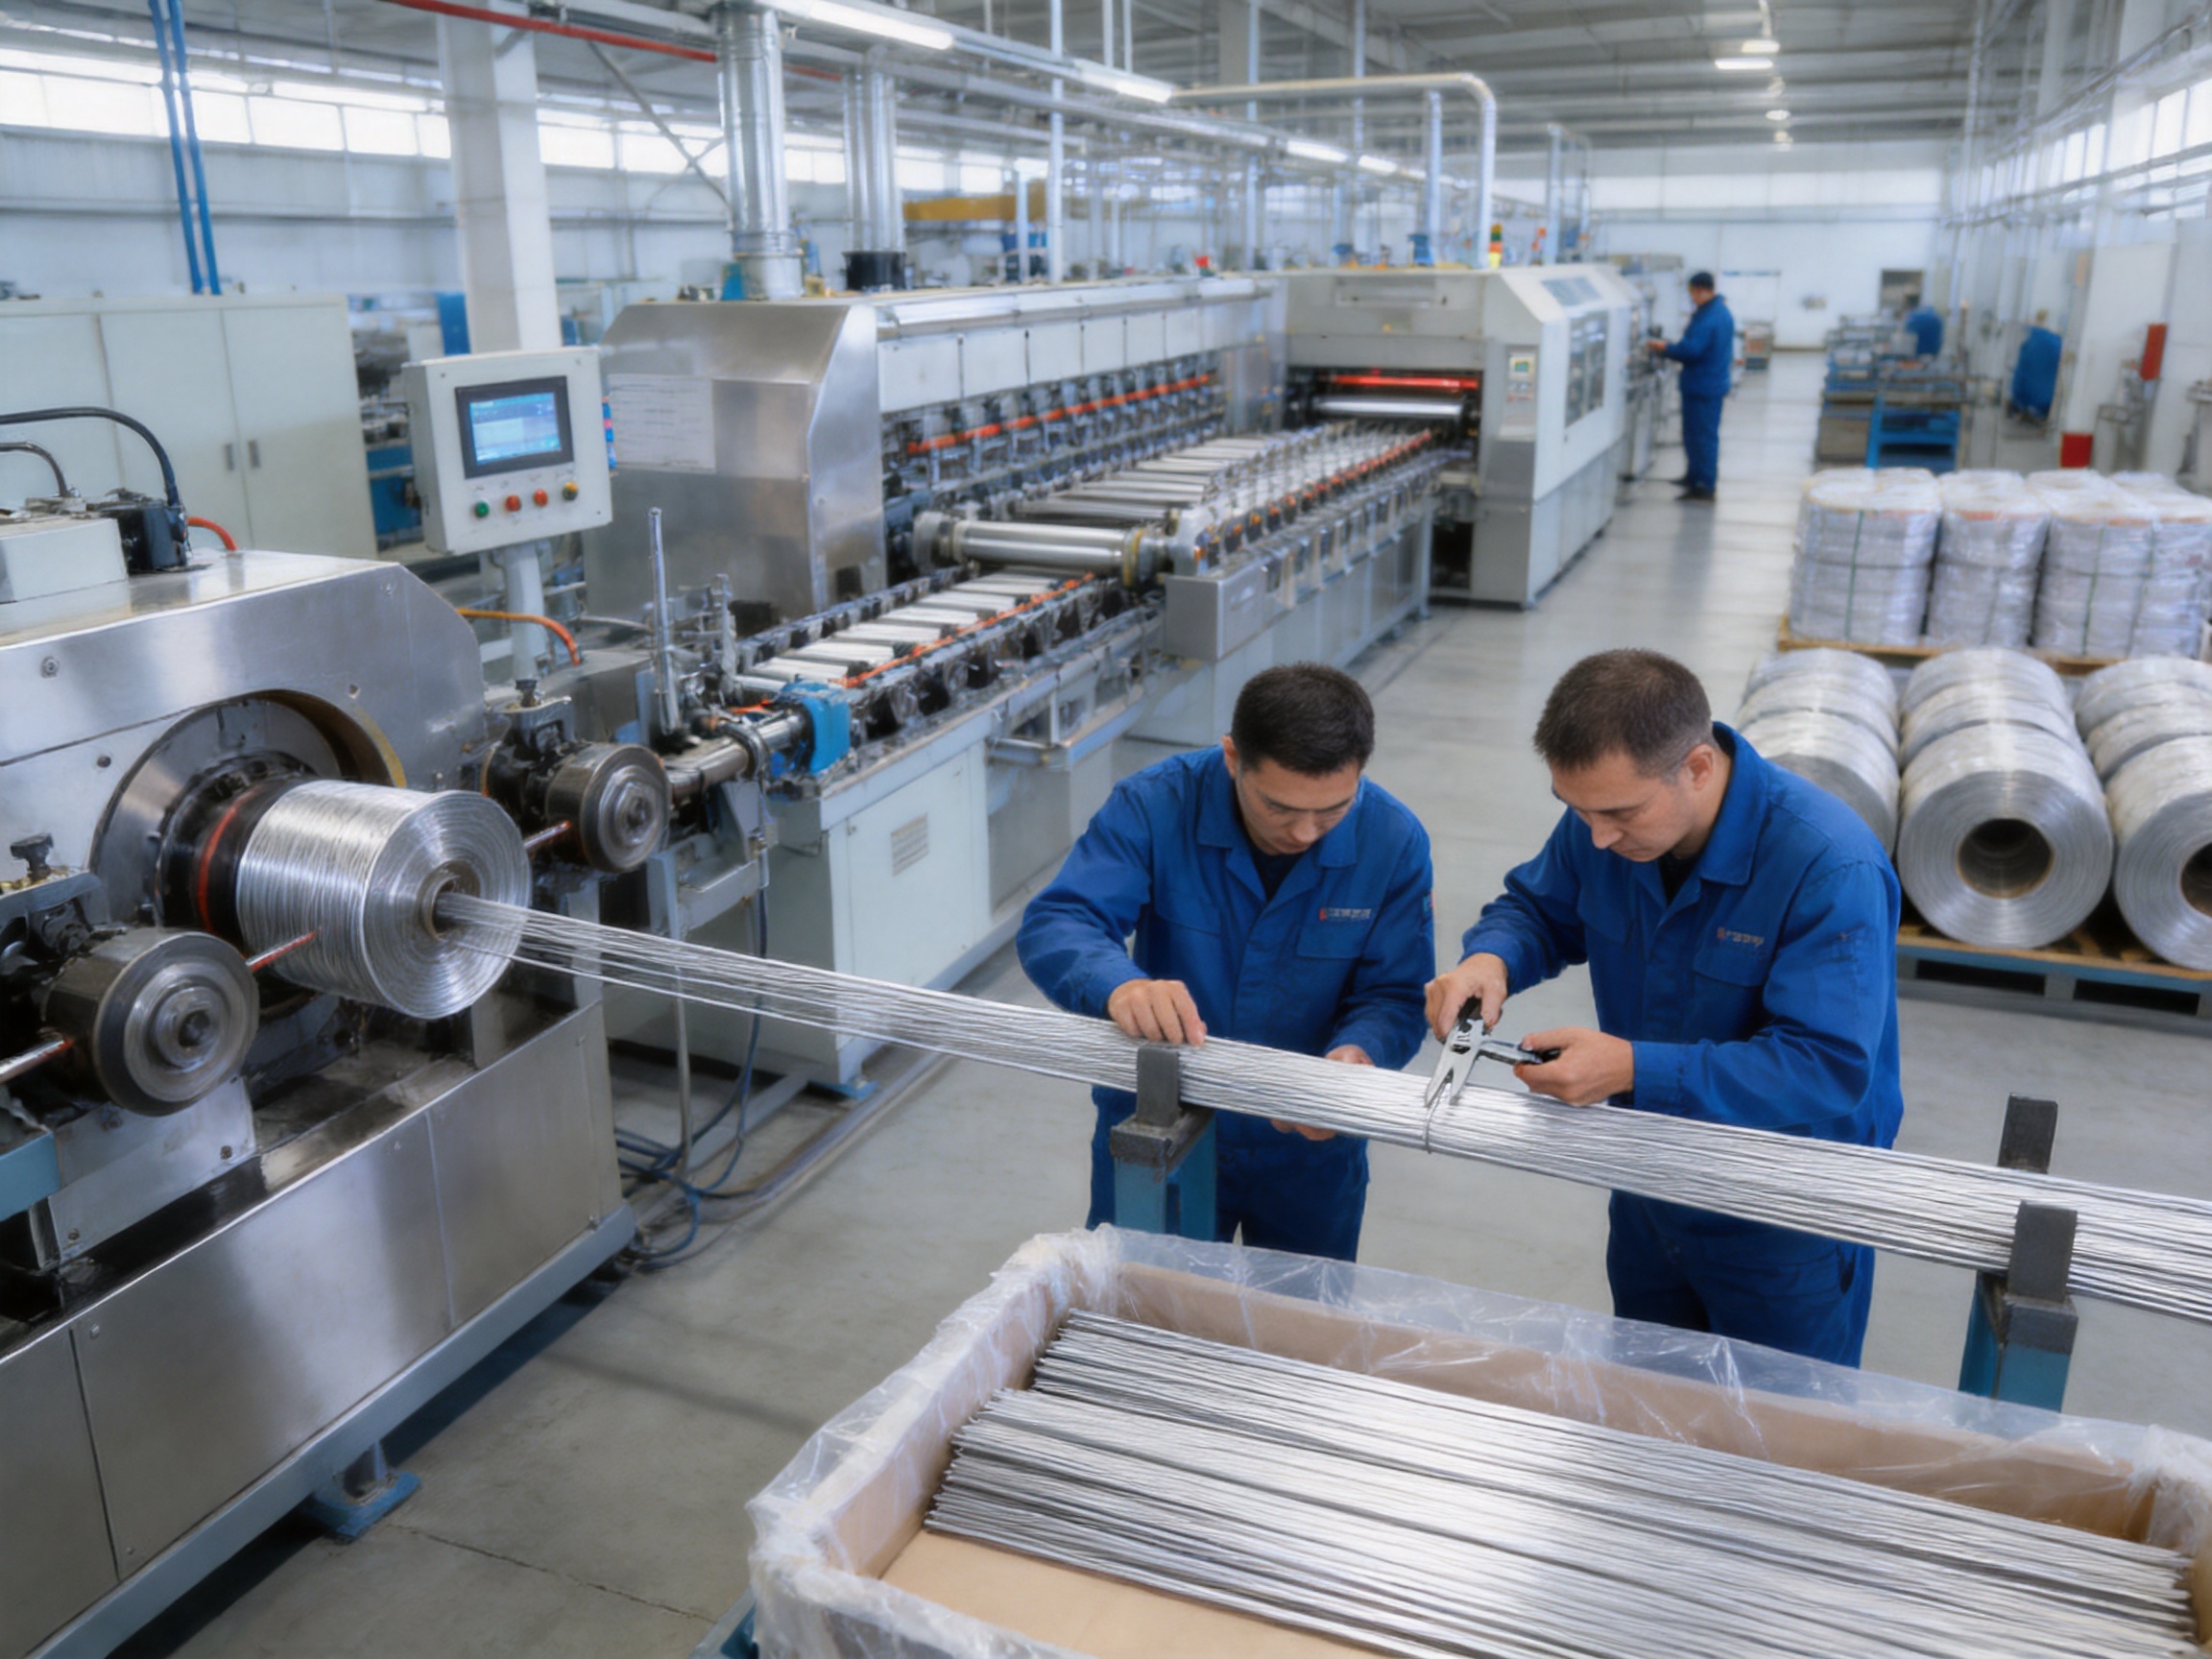
The reliability of a welding wire depends on the manufacturing system that produces it. A product may have the correct nominal description, but it will not perform consistently if the raw materials, forming operations, cleaning procedures, inspection methods, and packaging controls are not properly managed. Jiangsu Hetuo Aluminum Wire Co., Ltd. has established an integrated manufacturing structure designed to support aluminum wire and aluminum alloy material production.
Specialized aluminum material capability
The company’s product scope includes high-purity aluminum wire, high-strength aluminum alloy wire, and aluminum and aluminum alloy welding materials. This specialization gives the organization experience across several related aluminum product categories rather than limiting its operations to a single finished form. Knowledge developed in aluminum rod, wire, welding material, and precision profile production can contribute to improved control of material handling and conversion processes.
Aluminum is sensitive to contamination and surface damage during processing. A manufacturing organization focused on aluminum products can develop procedures that address cleaning, segregation, storage, forming, inspection, and packaging requirements specific to the material. This type of focus is valuable for customers that need stable welding performance from batch to batch.
Intelligent manufacturing system
The company has built an intelligent manufacturing system covering its principal aluminum product categories. Intelligent manufacturing can support production visibility, equipment coordination, process documentation, and the collection of quality information. It does not replace engineering judgment or operator skill; rather, it helps establish a more systematic relationship between production instructions, machine operation, inspection, and shipment.
For TIG wire, systematic manufacturing control may involve the monitoring of material preparation, forming dimensions, surface condition, cutting or straightening operations, and final packaging. The specific production route can vary according to alloy, wire size, delivery condition, and customer requirements. A coordinated system helps ensure that each stage is performed according to defined process expectations.
Advanced equipment and facilities
Jiangsu Hetuo Aluminum Wire Co., Ltd. introduces advanced equipment and facilities into its production operations. Modern equipment can offer improved dimensional control, repeatability, productivity, and process stability compared with less organized or heavily manual production methods. Equipment alone does not guarantee quality, but it provides a stronger foundation for controlled manufacturing when combined with trained personnel and documented procedures.
Production equipment for aluminum wire must be selected and maintained with attention to surface protection and contamination prevention. Contact surfaces, guides, rollers, dies, and handling areas can influence the condition of the finished wire. Proper equipment management helps reduce scratches, dents, embedded particles, and other defects that could affect feeding or welding behavior.
Quality inspection throughout production
The company states that it strictly implements quality inspection throughout production. In-process inspection is important because it allows issues to be identified before a full batch is completed. Depending on the product specification, inspection may include raw material verification, dimensional measurement, surface examination, chemical or material documentation, packaging checks, and final release review.
Inspection at multiple stages is more effective than relying only on a final visual check. If a forming operation begins to produce inconsistent dimensions, early detection allows timely adjustment. If packaging is found to be unsuitable, corrective action can be taken before the product reaches the customer. This approach supports both quality improvement and cost control.
For customers with strict procurement requirements, traceability is also important. Batch identification and production records can assist with receiving inspection, inventory management, welding procedure documentation, and investigation of any unexpected performance issue. The exact level of traceability depends on the agreed specification and order requirements, but a structured quality system provides the framework for managing it.
ISO 9001 and IATF 16949 certification
The company has obtained ISO 9001 and IATF 16949 quality management system certifications. ISO 9001 provides a recognized framework for quality management, process control, customer focus, corrective action, and continual improvement. IATF 16949 is associated with the automotive supply chain and places additional emphasis on risk management, defect prevention, process consistency, and customer-specific requirements.
These certifications do not mean that every welding application is automatically qualified without procedure development. Instead, they demonstrate that the manufacturer operates within formalized management systems intended to support repeatable quality and continual improvement. For buyers, this can provide greater confidence when evaluating supplier organization, documentation, corrective-action capability, and production discipline.
Production Environment and Organizational Capacity
Manufacturing capacity affects a supplier’s ability to manage orders, maintain equipment, support quality work, and respond to customer requirements. The company operates a factory covering approximately 40,000 square meters and employs 60 people, including 30 professional managers and technicians. This structure provides a balance between production personnel and technical or management resources.
A dedicated technical and management team can support activities such as process planning, quality review, equipment coordination, customer communication, and product improvement. In welding material production, technical support is particularly useful because the suitability of a wire depends on the customer’s base material, welding method, joint design, and acceptance criteria.
The company’s location in the Guannan Economic Development Zone of Lianyungang, Jiangsu Province, provides an established industrial setting for manufacturing and logistics. Its address is the Small and Medium-sized Enterprises Park, Economic Development Zone, Guannan County, Lianyungang City, Jiangsu Province, China. Industrial-zone operations can support access to transportation, utilities, production services, and a network of related manufacturing resources.
The company’s products are exported to high-end overseas markets. International supply requires attention to product consistency, communication, packaging, documentation, delivery coordination, and customer expectations across different regions. Export experience can help a manufacturer understand the importance of clear specifications and stable order execution.
Technical Considerations When Selecting TIG Wire
Selecting TIG wire should begin with the base material and the intended service condition. A filler wire that performs well on one aluminum alloy may not be the best choice for another. Buyers should consider the base alloy family, required weld properties, joint geometry, operating temperature, corrosion exposure, appearance requirements, and applicable standards.
Base alloy compatibility
The filler metal should be evaluated for compatibility with the aluminum or aluminum alloy being welded. Different base alloys may have different requirements for strength, ductility, crack resistance, corrosion performance, and post-weld behavior. The welding engineer or qualified procedure should determine whether the selected filler is appropriate rather than relying only on a general description such as “aluminum wire.”
When the base material is unknown or has been mixed with several alloy types, welding quality can become difficult to control. Material identification, supplier documentation, and a preliminary welding trial may be necessary. A dependable filler supplier can assist by clarifying available product categories and helping customers match the wire to their application requirements.
Wire diameter
Diameter affects the rate at which filler metal can be added and the amount of heat required to melt the wire. Smaller diameters may support delicate work, thin sections, and precise bead control. Larger diameters may be suitable for thicker components or higher deposition requirements. The correct size depends on current, joint preparation, material thickness, welding position, and operator technique.
Diameter consistency is essential. Significant variation can influence feeding, melting, and bead geometry. For automated or semi-automated processes, the acceptable dimensional range may be especially important because the equipment is programmed around a predictable wire size.
Surface cleanliness and storage
TIG wire should be stored in a clean, dry area protected from dust, oil, corrosive substances, and moisture. Aluminum naturally forms an oxide layer, but additional contamination can create welding problems. Wire should remain in its original protective packaging until needed, and opened material should be handled with clean gloves or tools where appropriate.
If wire has been exposed to condensation or heavy contamination, it should not be introduced directly into a critical weld. The user should follow internal procedures for inspection, cleaning, or disposition. Good storage practices protect the investment in the consumable and help maintain the quality established during manufacturing.
Packaging and identification
Packaging should protect the wire from bending, impact, contamination, and moisture during transportation and storage. Labels should clearly identify the product, size, quantity, batch or lot information where applicable, and any other agreed details. Clear identification reduces the risk of mixing different wires in the welding area.
For manufacturers operating several welding lines, organized material control is especially important. Separate storage locations, clear issue procedures, and batch records help prevent the wrong filler from being used in a qualified welding procedure. A supplier that understands these needs can provide packaging and documentation suited to professional production environments.
Comparison with Less Specialized Alternatives
Buyers often compare specialized aluminum TIG wire with lower-cost or general-purpose alternatives. Price is important, but the total cost of a welding consumable includes more than its purchase price. It also includes handling, inspection, rework, scrap, downtime, inventory complexity, and the risk of customer complaints.
| Evaluation factor | Specialized aluminum TIG wire | Inconsistent or general-purpose alternative |
|---|---|---|
| Material control | Produced within an aluminum-focused manufacturing system with defined inspection practices | May provide limited information about raw material and process control |
| Dimensional consistency | Designed for predictable feeding and controlled filler addition | Variation may cause irregular handling or melting behavior |
| Surface condition | Manufactured and packaged with attention to cleanliness and protection | Higher risk of contamination, oxidation, scratches, or handling damage |
| Quality management | Supported by ISO 9001 and IATF 16949 quality management systems | Quality procedures and corrective-action systems may be unclear |
| Application support | Supplier can discuss aluminum wire and welding material requirements | Technical guidance may be limited to basic product selling |
| Total production effect | Can support stable welding, reduced rework, and better process repeatability | Lower purchase cost may be offset by defects, waste, and downtime |
This comparison does not mean that every general-purpose product is unsuitable. Some alternative wires may perform well when correctly specified and controlled. The key difference is the level of assurance created by specialization, documented manufacturing, inspection, and technical communication. For applications where weld quality and repeatability matter, a supplier’s complete production capability should be considered alongside the unit price.
Applications for Aluminum TIG Wire
Aluminum TIG wire can support a broad range of fabrication and maintenance applications. The most appropriate application depends on the selected alloy, diameter, welding procedure, and customer acceptance requirements.
Precision aluminum fabrication
TIG welding is frequently used when operators need fine control over heat and filler addition. This includes precision frames, enclosures, brackets, panels, tubes, and small assemblies where appearance and dimensional accuracy are important. The process can produce controlled welds with limited spatter when properly managed.
Transportation and lightweight structures
Aluminum is used in transportation because it can reduce structural weight while providing useful strength and corrosion resistance. TIG wire may be applied to components requiring careful fit-up, controlled welding, repairability, or a high-quality visible finish. The selection of filler material must be based on the specific base alloy and the structural requirements of the component.
Industrial equipment
Industrial equipment may contain aluminum guards, frames, fluid-handling components, heat-transfer structures, fixtures, and fabricated housings. TIG welding allows manufacturers to join thinner sections and produce clean welds in areas where access and appearance are important. A consistent wire helps the production team maintain repeatable results across multiple assemblies.
Maintenance and repair
Repair welding requires careful assessment of the original material, contamination, previous heat exposure, and service history. TIG wire can be introduced in a controlled manner, making the process suitable for localized repairs and buildup work. Before repair, the component should be cleaned, inspected, and evaluated for cracks or hidden damage. The filler should then be selected according to the repair objective and the base alloy.
Precision profiles and fabricated sections
Aluminum profiles are used in machinery, architectural systems, industrial frames, and specialized equipment. When profiles must be joined or modified, TIG welding can provide a clean and accurately controlled connection. The quality of the filler wire is important because profile surfaces may remain visible and dimensional distortion may be difficult to correct after welding.
Recommended Welding Practices
A high-quality TIG wire performs best when the entire welding procedure is controlled. The following practices can help users obtain reliable results, although the final procedure should be established by qualified welding personnel for the particular application.
Prepare the base material
Remove oil, grease, paint, adhesive residue, and other contaminants before welding. Aluminum oxide should be managed using suitable cleaning methods and dedicated tools that will not introduce iron or other unwanted particles. Joint surfaces should be properly fitted, and excessive gaps should be avoided unless the welding procedure is designed to accommodate them.
Use suitable shielding gas coverage
Argon shielding must protect the tungsten electrode, filler wire, and molten weld pool. Incorrect flow, drafts, blocked gas passages, damaged cups, or excessive torch distance can allow atmospheric contamination. Shielding gas settings should be selected according to torch design, current, joint configuration, and the surrounding environment.
Control heat input
Aluminum conducts heat quickly, so the operator may need to balance current, travel speed, torch angle, and filler addition carefully. Excessive heat can cause burn-through, distortion, wide beads, and loss of dimensional accuracy. Insufficient heat may result in incomplete fusion or poor wetting. Consistent wire diameter and surface condition make it easier to maintain this balance.
Protect the wire during use
Filler wire should not be dragged across dirty surfaces or placed where it can collect dust, oil, or moisture. Cut lengths should be kept organized and protected before use. If the wire becomes visibly contaminated, it should be evaluated before being introduced into a weld intended for inspection or service.
Document successful procedures
Once a welding procedure produces acceptable results, record the relevant details. These may include base alloy, filler wire specification and diameter, tungsten type and size, current, polarity or waveform, shielding gas, flow rate, travel speed, preheat, interpass temperature, joint preparation, and inspection method. Documentation helps reduce variation and provides a basis for training new operators.
Customer-Oriented Supply and Technical Support
A welding material supplier should do more than ship a product. Customers may need assistance with product selection, packaging, batch information, export documentation, delivery planning, and communication about application requirements. Jiangsu Hetuo Aluminum Wire Co., Ltd. states that it is guided by customer needs and committed to customer satisfaction. This orientation is important because aluminum welding requirements vary considerably between industries.
Customer-oriented supply begins with clear communication. Before placing an order, the buyer should provide the intended base material, wire diameter, expected quantity, packaging preference, welding process, application sector, and any required certification or inspection documentation. The supplier can then confirm whether the available TIG wire is appropriate for the request or whether additional technical information is needed.
Stable supply is also important for production continuity. A change in filler wire diameter, packaging, surface condition, or material category can require adjustments to a qualified process. Buyers should therefore evaluate a supplier’s ability to maintain consistent production and communicate any specification changes in advance.
For international customers, the supplier’s export experience can support more efficient coordination. Clear product names, consistent labels, organized packing, and timely documentation help reduce receiving delays. When a product is used in a regulated or quality-sensitive industry, communication between the supplier’s technical team and the customer’s quality department may be especially valuable.
Why Choose a Specialized Manufacturer
Purchasing directly from a specialized manufacturer can offer several advantages over relying on an undifferentiated trading source. The manufacturer has greater control over raw material selection, production planning, equipment condition, inspection, packaging, and corrective action. This does not eliminate the need for customer verification, but it can improve transparency and responsiveness.
Jiangsu Hetuo Aluminum Wire Co., Ltd. combines product specialization with a substantial manufacturing base. Its capabilities cover aluminum wire, aluminum alloy wire, welding materials, and related precision products. This breadth allows customers to discuss several material needs with one organization while still working with a company focused on aluminum products.
The company’s 40,000-square-meter factory, 60-person workforce, and team of 30 professional managers and technicians provide an organizational foundation for production and quality management. Its advanced equipment, intelligent manufacturing approach, and inspection throughout production support the objective of delivering consistent material for demanding applications.
ISO 9001 and IATF 16949 certifications further demonstrate a formal approach to quality management. For customers comparing suppliers, these credentials can be considered together with actual product samples, technical documents, inspection results, response time, delivery performance, and application feedback. The strongest supplier relationship is based on verified performance rather than marketing statements alone.
Purchasing Checklist for TIG Wire
Before ordering aluminum TIG wire, buyers can review the following points:
1. Confirm the base aluminum or aluminum alloy and identify the required filler compatibility.
2. Specify the wire diameter, delivery form, length or package type, and estimated consumption.
3. Define the required surface condition, cleanliness level, and storage expectations.
4. Request product identification, batch information, and available quality documentation.
5. Confirm whether the product is intended for manual TIG, mechanized TIG, or another compatible application.
6. Review packaging requirements for domestic or international transportation.
7. Ask about production lead time, minimum order quantity, and repeat-order consistency.
8. Verify that the supplier has suitable quality management and inspection procedures.
9. Conduct a welding trial if the material will be used in a new or critical application.
10. Establish a clear process for reporting nonconformities and requesting corrective action.
This checklist helps transform a general consumable purchase into a controlled material-selection decision. It also encourages communication between purchasing, welding engineering, production, and quality departments.
Frequently Asked Questions
What is TIG wire used for?
TIG wire is used as filler metal in tungsten inert gas welding. It is introduced into the weld pool created by a non-consumable tungsten electrode under argon or another suitable inert shielding gas. For aluminum applications, it can be used to join, repair, or build up aluminum and aluminum alloy components.
Is TIG wire the same as a tungsten electrode?
No. TIG wire is the filler material added to the weld. The tungsten electrode creates and maintains the arc but is designed not to melt into the joint during normal operation. Both are important, but they perform different functions.
Why is surface cleanliness important for aluminum TIG wire?
Contamination can enter the weld pool and contribute to porosity, inclusions, unstable melting, or poor appearance. Clean wire helps the shielding gas and welding procedure protect the molten metal. Proper storage and handling are still necessary after the wire leaves the manufacturer.
How do I select the correct aluminum TIG wire?
Start with the base alloy, required weld properties, joint design, service environment, and applicable welding standard. Consider wire diameter, welding current, material thickness, position, and appearance requirements. A qualified welding engineer or experienced supplier should confirm the selection for critical work.
Can TIG wire be used for automated welding?
It may be suitable for mechanized or automated TIG systems when the wire form, diameter, packaging, and feeding characteristics match the equipment. Automated applications generally require closer control of dimensional consistency, straightness, surface condition, and delivery format than basic manual work.
What advantages does a specialized aluminum wire manufacturer provide?
A specialized manufacturer can offer greater knowledge of aluminum materials, more focused process control, suitable equipment, inspection systems, technical communication, and better support for repeat orders. These advantages may reduce variability and help customers manage total welding costs.
What quality systems support this TIG wire?
Jiangsu Hetuo Aluminum Wire Co., Ltd. has obtained ISO 9001 and IATF 16949 quality management system certifications. The company also states that it performs quality inspection throughout production and uses advanced equipment and facilities.
Where is the manufacturer located?
The manufacturer is located in the Small and Medium-sized Enterprises Park, Economic Development Zone, Guannan County, Lianyungang City, Jiangsu Province, China.
How can customers contact the manufacturer?
Customers can contact the company by telephone at +86-15961627690 or +86-18961612067. The listed email address is [email protected].
What should be done with opened wire that has been exposed to moisture?
The wire should be inspected and evaluated according to the user’s quality procedure. Moisture, condensation, and contamination can affect welding performance. For critical work, questionable material should not be used without appropriate approval, cleaning, or testing.
Conclusion
TIG wire is a fundamental component of controlled aluminum welding. Its value is determined not only by its nominal material description, but also by the consistency of its chemistry, dimensions, surface condition, packaging, and supply history. When these characteristics are stable, welders can better control filler addition, weld-pool behavior, appearance, and production repeatability.
Jiangsu Hetuo Aluminum Wire Co., Ltd. offers TIG wire within a broader aluminum material manufacturing system that includes high-purity aluminum wire, high-strength aluminum alloy wire, and aluminum and aluminum alloy welding materials. Its factory covers approximately 40,000 square meters, and its workforce includes professional managers and technicians supporting production and quality activities. Advanced equipment, intelligent manufacturing, inspection throughout production, ISO 9001 certification, and IATF 16949 certification provide important strengths for customers evaluating a supplier.
Compared with less specialized alternatives, a controlled aluminum welding material can help reduce process variation, handling problems, rework, and material waste. The best results are achieved when the wire is matched correctly to the base alloy and used with a qualified welding procedure, suitable shielding, proper joint preparation, and disciplined storage.
For manufacturers seeking dependable aluminum welding materials, the selection process should consider technical suitability, quality management, production capability, export experience, documentation, and long-term supply stability. A specialized supplier with a customer-focused approach can help convert these requirements into a practical and repeatable welding solution.
References
1. American Welding Society, Welding Handbook, Volume 1: Welding Science and Technology.
2. American Welding Society, Specification for Aluminum and Aluminum-Alloy Bare Welding Rods and Wires.
3. International Organization for Standardization, ISO 9001: Quality Management Systems — Requirements.
4. International Automotive Task Force, IATF 16949: Quality Management System Requirements for Automotive Production and Relevant Service Parts Organizations.
5. Aluminum Association, Aluminum Standards and Data.
6. Technical information provided for aluminum and aluminum alloy welding materials by Jiangsu Hetuo Aluminum Wire Co., Ltd.