

 English
 中文简体
 русский
 Deutsch
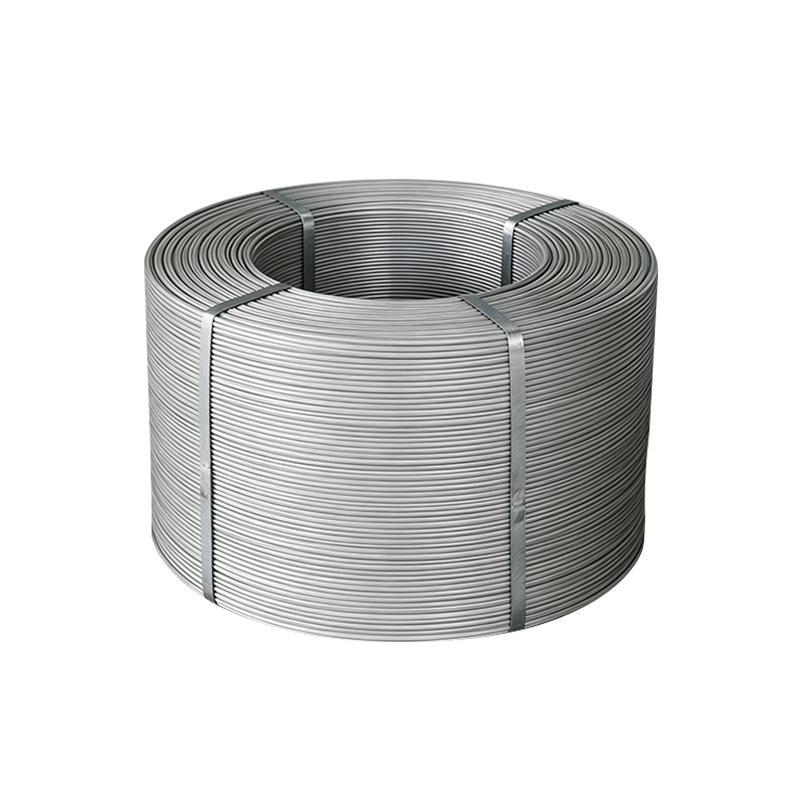
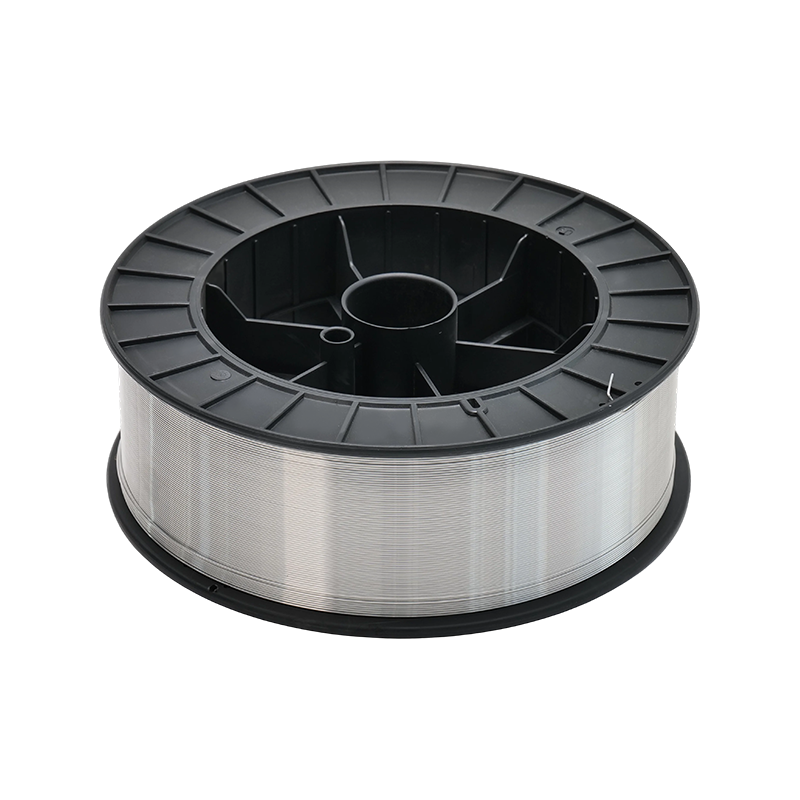
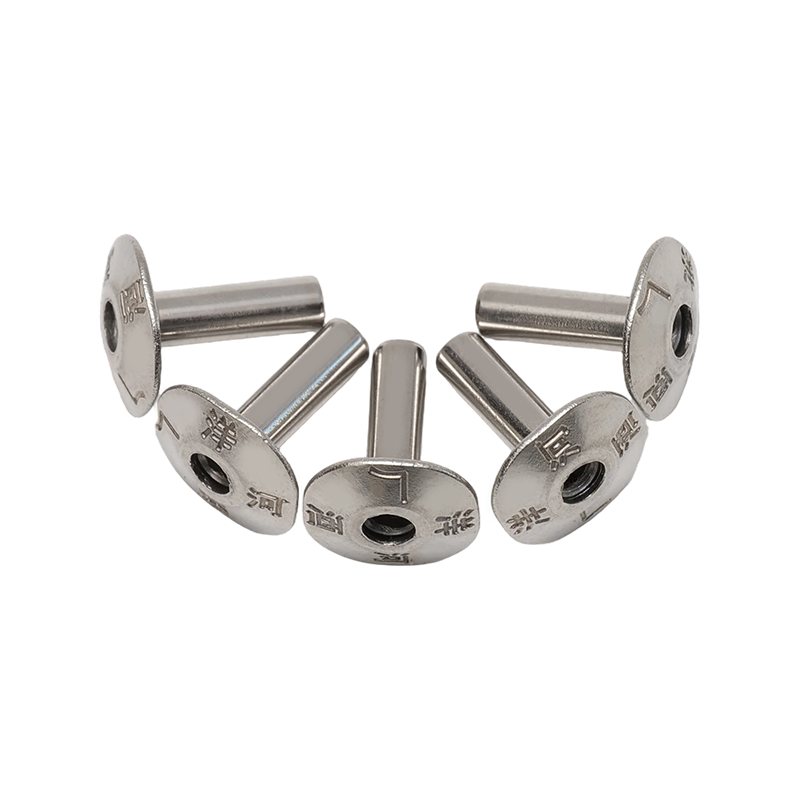
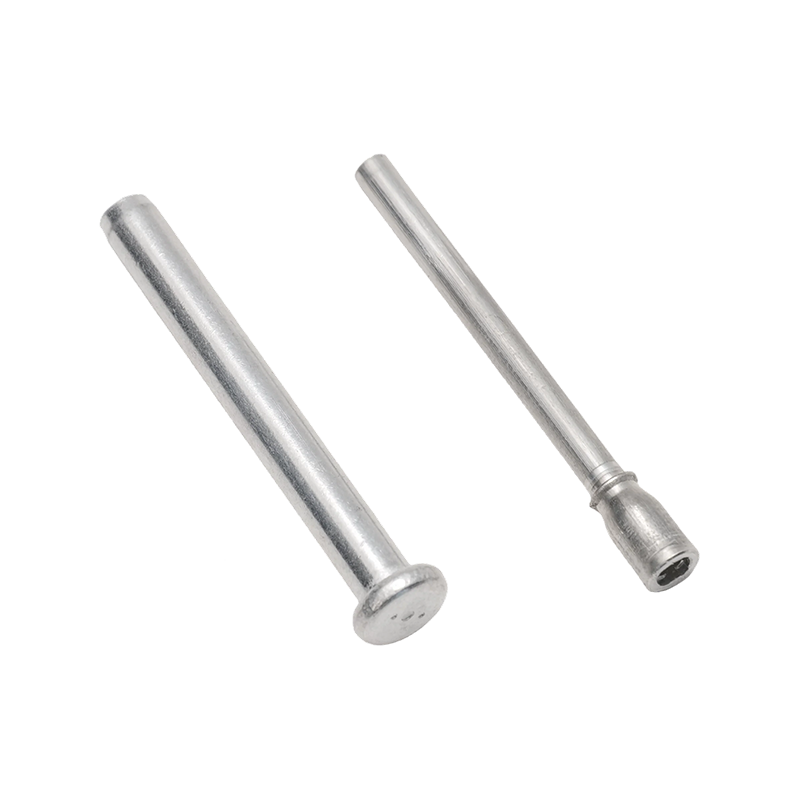
High-strength aluminum alloy wire for rivets is an essential engineering material for aircraft, aerospace structures, military equipment, transportation systems, and other applications where lightweight construction must be combined with dependable mechanical performance. Rivet wire is used to produce fasteners that join sheets, profiles, and structural components without adding the excessive weight associated with steel or other dense metals. The selection of the correct aluminum alloy, temper, diameter, surface condition, and forming performance directly affects the safety, service life, and manufacturing efficiency of the finished assembly.
Jiangsu Hetuo Aluminum Wire Co., Ltd. supplies aluminum alloy wire for rivet applications and focuses on high-purity aluminum wire, high-strength aluminum alloy wire, and aluminum and aluminum alloy welding materials. Its product range includes grades intended for demanding applications in aviation, aerospace, military manufacturing, and industrial fabrication. The company combines alloy control, precision wire processing, process inspection, and customer-oriented customization to provide material solutions for different rivet designs and production requirements.
The “For Rivets” product is positioned within the high-strength aluminum alloy wire category. It is particularly suitable for applications that require a balance of strength, fracture toughness, corrosion resistance, low-temperature performance, and forming reliability. Depending on the selected alloy and heat-treatment condition, the wire can be used to manufacture rivets for high-load structural assemblies or specialized components exposed to challenging environments.
Content
- 1 Why Aluminum Alloy Wire Is Used for Rivets
- 2 Material Performance and Strengthening Characteristics
- 3 Available Alloy Grades and Chemical Composition
- 4 Advantages Over General-Purpose Aluminum Wire
- 5 Advanced Manufacturing and Process Control
- 6 Manufacturing Strengths of the Supplier
- 7 Rivet-Wire Manufacturing Considerations
- 8 Applications in Aviation, Aerospace, and Military Equipment
- 9 How the Product Supports Customer Competitiveness
- 10 Quality, Traceability, and Technical Communication
- 11 Environmental and Sustainability Considerations
- 12 Recommended Selection Process
- 13 Frequently Asked Questions
- 13.1 What is high-strength aluminum alloy rivet wire?
- 13.2 Which industries use this product?
- 13.3 What are the main advantages of aluminum rivet wire?
- 13.4 What is the difference between T6, T73, and T76?
- 13.5 Can the wire be customized?
- 13.6 Are all listed aluminum grades intended for rivets?
- 13.7 How is quality controlled during production?
- 13.8 What information should be included in an inquiry?
- 13.9 How should aluminum alloy wire be stored?
- 13.10 Can the material be used directly in aerospace production?
- 14 Conclusion
- 15 References
- 16 Product: For Rivets
Why Aluminum Alloy Wire Is Used for Rivets
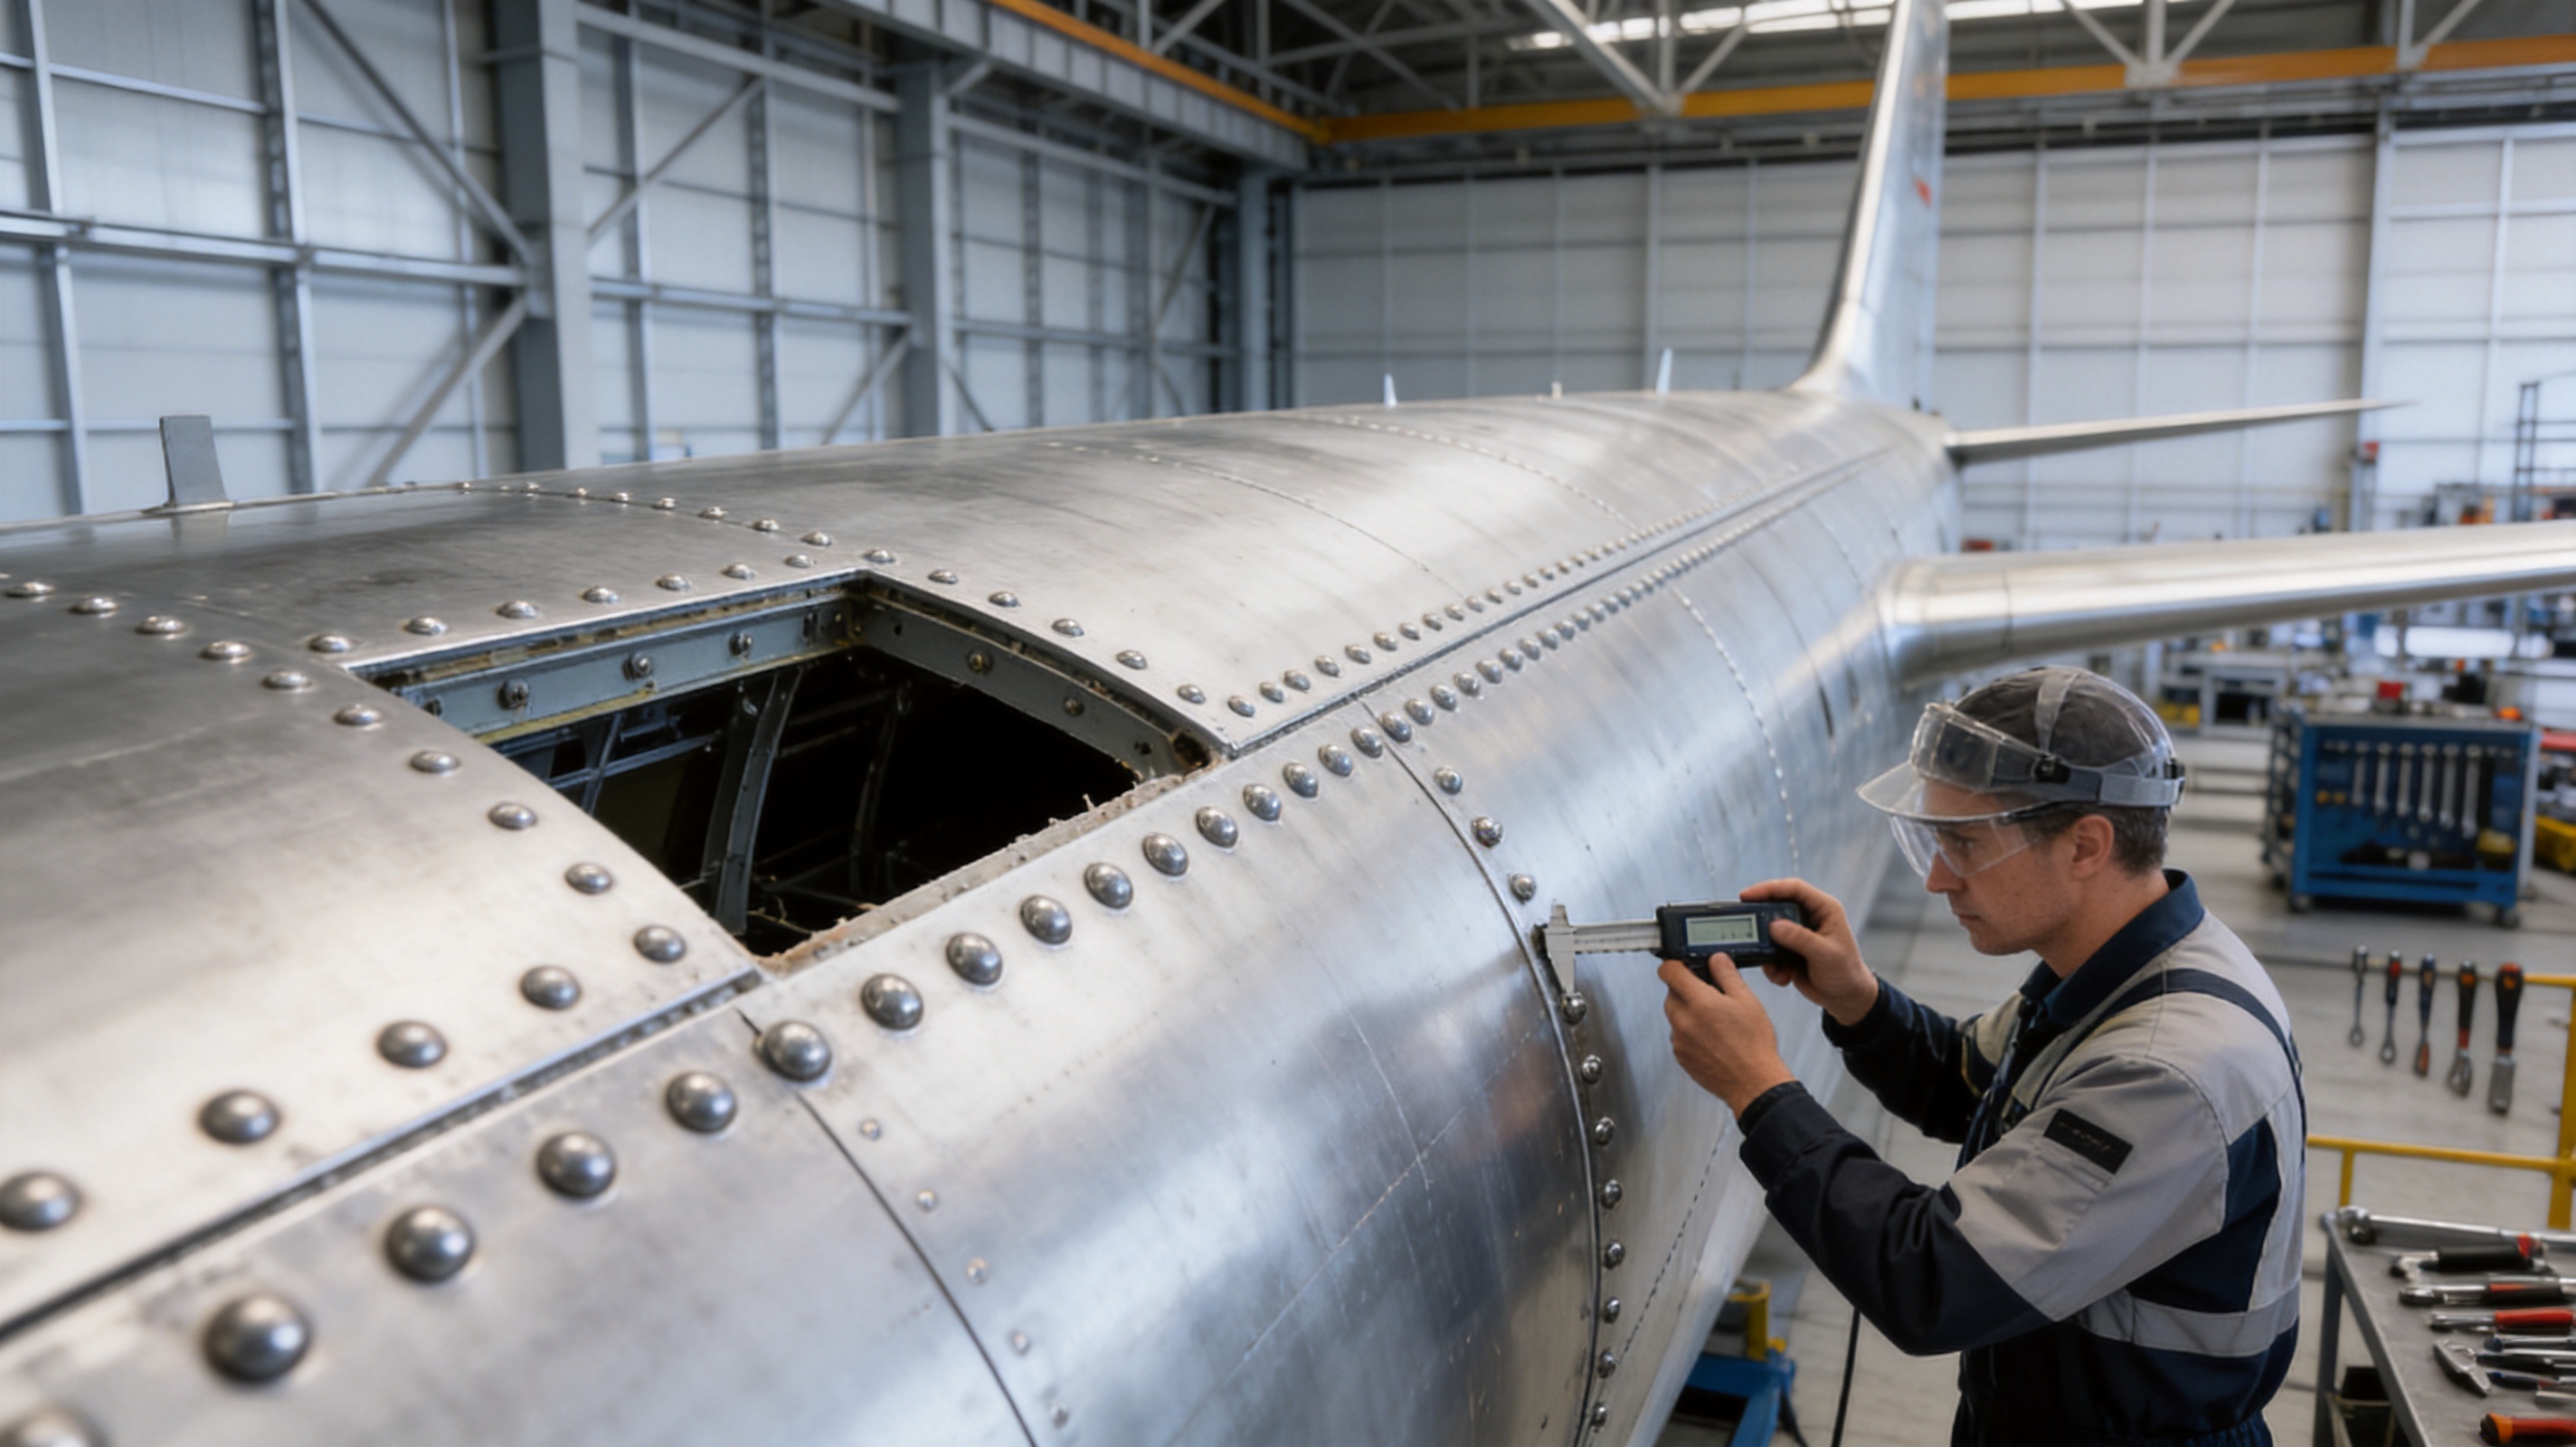
Riveted joints remain important in aircraft and aerospace manufacturing because they provide a practical and inspectable method of joining thin sheets, formed sections, skins, frames, and other structural parts. Aluminum alloy rivets are especially valuable because their density is significantly lower than that of steel rivets. Weight reduction is a primary design objective in aviation, where every saved kilogram can contribute to improved fuel efficiency, payload capacity, range, or operating economy.
Aluminum rivets also offer good compatibility with many aluminum structures. When the rivet and the components being joined have suitable electrochemical and mechanical characteristics, the risk of galvanic interaction can be reduced. The relatively low forming load of aluminum alloy rivets can also support efficient installation and help limit damage to thin or sensitive components.
Rivet wire is not simply ordinary aluminum wire cut into short lengths. It must meet more demanding requirements related to consistency, ductility, dimensional accuracy, surface quality, and response to forming. During rivet production, the wire may be cut, headed, upset, or otherwise formed into a fastener. Any defect in the wire can become a crack, surface split, inclusion, dimensional variation, or head-forming problem in the finished rivet.
For this reason, high-strength aluminum alloy rivet wire must combine a controlled chemical composition with an appropriate metallurgical condition. Strength alone is not sufficient. A wire that is extremely strong but difficult to form may create production problems. Conversely, a very soft wire may be easy to upset but unable to meet the mechanical requirements of the finished rivet. The most effective material is one that provides an appropriate relationship between strength, plastic deformation, toughness, corrosion resistance, and process stability.
Material Performance and Strengthening Characteristics
The supplied high-strength aluminum alloy wire is designed for demanding applications in aviation, aerospace, and military fields. Its performance is associated with precipitation strengthening and transition-phase strengthening mechanisms. Through suitable alloy design and heat treatment, alloying elements form strengthening phases within the aluminum matrix. These phases resist dislocation movement and increase the strength of the material.
Heat treatment and temper selection are especially important for high-strength aluminum alloys. The same basic alloy can exhibit different combinations of tensile strength, ductility, fracture toughness, and corrosion resistance depending on its processing condition. The product information identifies T6, T73, and T76 conditions as important examples of performance-oriented tempers.
T6 Condition
The T6 condition is generally associated with a high-strength state achieved through solution heat treatment, quenching, and artificial aging. For rivet applications requiring high load-bearing capability, this condition can offer an attractive strength level. It may be considered when the design prioritizes mechanical strength and the service environment is appropriately controlled.
Although high strength is a major advantage, T6 material must be selected with attention to the complete application. Rivets are formed and installed under mechanical deformation, and the condition of the wire must be compatible with the manufacturing process. The customer should confirm the required forming sequence, final fastener condition, and applicable technical standard before selecting T6 material for production.
T73 Condition
The T73 condition is associated with comparatively high fracture toughness and improved resistance to stress corrosion cracking and exfoliation corrosion. It also provides useful low-temperature performance. These characteristics can be important in aerospace assemblies exposed to cyclic loading, moisture, temperature changes, and long service periods.
Compared with a condition chosen only for maximum strength, T73 may offer a more balanced solution where damage tolerance and environmental durability are central design requirements. In aircraft structures, a small crack or corrosion feature can become more serious when it is located near a highly stressed joint. A material with improved fracture toughness and corrosion resistance can help support a more robust structural design, subject to proper joint engineering and inspection.
T76 Condition
The T76 condition is described as providing higher strength than T73 while retaining higher stress corrosion resistance than T6. This makes it an option for applications that require a compromise between strength and environmental resistance. The exact suitability depends on the rivet design, the alloy grade, the installation method, and the service environment.
By offering material in performance-oriented conditions, the supplier can support more precise material selection than a one-condition product approach. The customer can discuss whether the priority is maximum strength, improved toughness, environmental durability, low-temperature service, or a controlled combination of these properties.
The table below summarizes the general performance direction of the principal conditions described for this product. It is intended as a selection guide rather than a replacement for a certified material specification or customer-approved technical data sheet.
| Condition | Primary Performance Characteristics | Typical Selection Consideration |
|---|---|---|
| T6 | High strength | Applications where strength is a major design priority and the environment is properly controlled |
| T73 | Relatively high fracture toughness, stress corrosion resistance, exfoliation corrosion resistance, and low-temperature performance | Structures requiring improved damage tolerance and environmental durability |
| T76 | Higher strength than T73 and higher stress corrosion resistance than T6 | Applications requiring a balance of elevated strength and improved corrosion resistance |
Available Alloy Grades and Chemical Composition
The product information lists a wide range of aluminum and aluminum alloy grades. These include high-strength aerospace alloys such as 2A10, 2219, 7050, and 7075, together with aluminum-silicon welding grades, aluminum-magnesium welding grades, and other alloy families. This broad range allows the company to serve both rivet-wire and related aluminum material requirements.
Not every listed grade is intended for the same function. Some grades are primarily associated with high-strength structural applications, while others are more suitable for welding wire or filler-metal use. Correct classification is therefore essential. Customers should identify the required application before placing an order so that the alloy, temper, diameter, and processing condition can be matched to the intended use.
| Grade | Principal Alloying Features Shown in the Product Data | Potential Material Role |
|---|---|---|
| 2A10 | Copper approximately 3.9–4.5%; manganese approximately 0.30–0.50%; magnesium approximately 0.15–0.30% | High-strength aluminum alloy wire for demanding structural applications |
| 2219 | Copper approximately 5.8–6.8%; manganese approximately 0.2–0.4%; zirconium approximately 0.02–0.10% | High-strength alloy option for aerospace-related applications |
| 4043 | Silicon approximately 4.5–6.0% | Aluminum-silicon welding material |
| 4047 | Silicon approximately 11.0–13.0% | Higher-silicon aluminum welding material |
| 5183 | Magnesium approximately 4.3–5.2%; manganese approximately 0.5–1.0% | Aluminum-magnesium welding material |
| 5356 | Magnesium approximately 4.5–5.5%; manganese approximately 0.05–0.20% | Aluminum-magnesium welding material |
| 7050 | Zinc approximately 5.7–6.7%; copper approximately 2.0–2.6%; magnesium approximately 1.9–2.6% | High-strength aerospace alloy wire |
| 7075 | Zinc approximately 5.0–7.0%; magnesium approximately 1.8–2.8%; copper approximately 1.4–2.0% | High-strength aluminum alloy option for specialized applications |
The chemical composition data also identifies limits for silicon, iron, copper, manganese, magnesium, chromium, nickel, zinc, titanium, zirconium, beryllium, and other elements. Aluminum is listed as the balance element. These controls are important because relatively small changes in alloying or impurity levels can influence strength, ductility, corrosion behavior, melting characteristics, weldability, and the response to heat treatment.
For high-strength rivet wire, the alloy must be selected according to the requirements of the finished fastener and the structure in which it will be used. A copper-containing alloy may provide a high-strength response after heat treatment, while an aluminum-magnesium alloy may provide a different combination of corrosion resistance, ductility, and welding performance. The correct grade should therefore be confirmed with engineering documentation rather than selected only by nominal strength.
The supplier can support customers who need material for standard production as well as those developing a customized rivet or fastener solution. Customized discussions may include alloy grade, wire diameter, temper, coil or straight-length delivery, surface condition, packaging, inspection documentation, and production quantity.
Advantages Over General-Purpose Aluminum Wire
One of the main advantages of high-strength aluminum alloy rivet wire is its application-specific design. General-purpose aluminum wire may be suitable for basic forming, tying, electrical, or decorative uses, but it may not provide the mechanical consistency or heat-treatment response required for aerospace fasteners. Rivet wire must be produced with closer attention to internal quality, surface condition, dimensional consistency, and forming behavior.
Another advantage is the availability of multiple alloy and temper options. A single general-purpose wire may force the customer to compromise between strength and corrosion resistance. A broader product range allows the material to be selected according to the actual design environment. For example, a high-strength condition may be appropriate for one rivet design, while a toughness- and corrosion-oriented condition may be better for another.
Aluminum alloy rivet wire also provides a favorable strength-to-weight relationship. Compared with heavier metallic fastener materials, it can help reduce the mass of assembled structures. This is particularly valuable in aircraft, spacecraft, defense equipment, rail transportation, and other systems where structural weight affects operating performance.
When manufactured with controlled processing, the wire can offer more uniform deformation during heading and installation. Consistent deformation helps reduce variations in rivet head shape, improves production repeatability, and supports more reliable dimensional control. Stable wire quality can also reduce the likelihood of rejects caused by surface cracking, uneven forming, or inconsistent hardness.
The material can be supplied for different downstream operations. Depending on customer requirements, it may be delivered as wire suitable for cutting and forming into rivets or in another controlled configuration for further processing. The exact supply condition should be confirmed before production because wire diameter, straightness, coil tension, and temper all influence the performance of automated manufacturing equipment.
Advanced Manufacturing and Process Control
The manufacturing of high-strength aluminum alloy wire involves more than drawing aluminum through a die. It is a controlled sequence that may include raw-material preparation, melting or alloy preparation, casting, homogenization, hot working, rolling, drawing, heat treatment, surface cleaning, dimensional inspection, and packaging. Each stage can affect the final quality of the rivet wire.
Raw Material and Alloy Preparation
The process begins with the selection and proportioning of raw materials. Alloying elements must be introduced within the required composition range, while impurities must be controlled. The objective is to produce a stable melt and a consistent starting material that can respond predictably during subsequent thermal and mechanical processing.
For high-strength grades, composition control is especially important because copper, magnesium, zinc, manganese, chromium, zirconium, titanium, and other elements influence precipitation behavior, grain structure, corrosion resistance, and final mechanical properties. Chemical analysis provides the basis for confirming that the alloy meets the required grade before further processing.
Melting, Casting, and Homogenization
During melting and casting, process stability helps limit segregation, inclusions, gas porosity, and other metallurgical defects. The cast product must have a suitable internal structure before it is converted into rod or wire. Homogenization heat treatment can help reduce compositional variations and prepare the alloy for more consistent hot working and downstream deformation.
Internal quality is particularly relevant for rivet wire because defects that are not visible on the surface may become apparent during heading or upsetting. A sound starting structure supports improved reliability when the wire is subjected to repeated drawing and forming operations.
Rod Processing and Drawing
Aluminum alloy rod is reduced to the required wire dimensions through controlled mechanical processing. Drawing changes the cross-sectional area and can improve dimensional accuracy, but excessive deformation or unsuitable lubrication may damage the surface or create residual stress. Die condition, reduction schedule, drawing speed, lubrication, and intermediate treatment must therefore be managed carefully.
For rivet manufacturing, diameter consistency is important because the wire is commonly cut into blanks of a controlled length before the head is formed. Variations in diameter can affect blank volume, head dimensions, forming force, and the final fit of the rivet. Precision drawing and systematic measurement help maintain the stability required by automated or semi-automated production lines.
Heat Treatment and Temper Control
Heat treatment is one of the most important steps for precipitation-strengthened aluminum alloys. Solution treatment, quenching, artificial aging, and intermediate handling must be controlled to obtain the targeted condition. Differences in heating rate, holding time, cooling rate, or aging schedule can influence strength, hardness, toughness, and corrosion behavior.
The T6, T73, and T76 conditions described for the product represent different performance priorities. Producing these conditions requires disciplined thermal processing and clear identification of the material throughout the production cycle. Heat-treatment records and traceability are useful for verifying that each batch has undergone the intended process.
Surface Quality and Cleaning
Surface quality is critical for wire that will be cut and formed into rivets. The wire should be free from harmful scratches, cracks, laps, excessive oxide, embedded foreign material, and other conditions that could become failure-initiation points. Cleaning and handling practices should prevent contamination and preserve the condition of the wire before packaging.
A controlled surface also supports consistent feeding through rivet-making equipment. Excessive surface irregularity can increase friction, interfere with straightening, damage tooling, or produce inconsistent blank dimensions. Careful storage and packaging are therefore part of the quality system rather than merely logistical details.
Inspection and Testing
Inspection may cover chemical composition, diameter, ovality, surface condition, tensile properties, hardness, elongation, heat-treatment condition, and other customer-specified requirements. The appropriate testing program depends on the grade, product form, applicable standard, and intended use.
Process inspection throughout production is an important strength of a specialized wire manufacturer. Instead of relying only on final inspection, a controlled manufacturing system monitors quality at multiple stages. Early detection of deviations can reduce waste, improve consistency, and help maintain stable delivery performance.
Manufacturing Strengths of the Supplier
Jiangsu Hetuo Aluminum Wire Co., Ltd. was established in 2019 and has developed an intelligent manufacturing system for aluminum alloy materials. The company operates in the Guannan Economic Development Zone in Lianyungang, Jiangsu Province, China. Its factory covers approximately 40,000 square meters and employs 60 people, including professional managers and technical personnel.
The company’s manufacturing scope includes high-purity aluminum wire, high-strength aluminum alloy wire, aluminum alloy welding wire, and precision aluminum alloy profiles. This product structure allows the company to build experience across several related areas of aluminum processing. Knowledge gained from alloy preparation, drawing, welding material production, and profile processing can support a more comprehensive understanding of aluminum material behavior.
Advanced equipment and facilities are used to support production. The purpose of equipment modernization is not simply to increase output. It is also to improve control over alloy preparation, dimensional accuracy, thermal processing, surface condition, production records, and repeatability between batches.
Quality inspection is implemented throughout production. This approach is important for high-strength wire because quality can be affected by every stage from raw material selection to final packing. By applying inspection during production rather than only after completion, the company can identify process variation earlier and maintain greater control over the finished material.
The company has obtained ISO 9001 and IATF 16949 quality management system certifications. ISO 9001 provides a structured framework for quality management, customer requirements, process control, corrective action, and continual improvement. IATF 16949 is associated with automotive quality management and emphasizes process discipline, risk management, traceability, defect prevention, and supply-chain control. These systems can provide useful confidence for customers requiring documented and repeatable manufacturing practices.
Although rivet wire for aerospace applications and automotive material may have different technical specifications, the process-control principles are valuable in both fields. Stable procedures, documented inspections, personnel training, equipment maintenance, and corrective-action systems help reduce variation and support dependable delivery.
Rivet-Wire Manufacturing Considerations
The design of a rivet begins with the joint requirements. Engineers normally consider the thickness and type of materials being joined, expected loads, temperature range, vibration, moisture, corrosion exposure, accessibility, installation method, inspection requirements, and service life. The rivet alloy should be selected as part of this complete design rather than as an isolated material decision.
Wire diameter is another important factor. The diameter determines the starting volume of the rivet blank and influences the size of the finished head and shank. A supplier must be able to maintain the specified diameter within the agreed tolerance and provide consistent material along the length of the coil or batch.
Surface condition affects feeding, cutting, forming, and final appearance. A clean and uniform surface is desirable for automated equipment and for applications where the rivet must maintain a predictable interface with the joined material. The presence of deep scratches or localized defects may become more serious when the wire is upset during head formation.
Temper selection must account for both production and service. Some rivets may be installed in a condition that supports forming and then receive an aging treatment. Other designs may require a pre-existing strength condition or a particular balance of ductility and environmental resistance. The customer should specify whether the wire is intended for direct forming, post-forming heat treatment, or another manufacturing route.
Storage is also important. Aluminum wire should be protected from moisture, contamination, impact, and unnecessary temperature cycling. Packaging should prevent deformation of coils or straight lengths and should preserve identification labels. Batch traceability allows the material to be connected with its chemical analysis, process records, inspection results, and shipment documentation.
Applications in Aviation, Aerospace, and Military Equipment
Aviation and aerospace applications place demanding requirements on structural materials. Components may experience repeated vibration, pressure changes, thermal cycling, moisture, deicing chemicals, salt-laden air, and low temperatures at altitude. Rivet materials must therefore be selected for more than initial strength.
In aircraft structures, aluminum alloy rivets may be used in skins, frames, stringers, brackets, panels, and other assemblies. The required alloy and temper vary with the location of the joint and the design philosophy. Some joints prioritize ease of installation and controlled deformation, while others require improved strength or resistance to crack growth and corrosion.
Aerospace vehicles may encounter wider temperature ranges and more severe weight restrictions. High-strength aluminum alloy rivet wire can help contribute to lightweight structural design when used with compatible alloys and a properly engineered joint. The material’s strength-to-weight characteristics are especially relevant where many fasteners are used across a large airframe or aerospace structure.
Military equipment may also benefit from lightweight aluminum fasteners. Vehicles, shelters, aircraft, communication systems, and specialized equipment can require corrosion-resistant and mechanically dependable joints while maintaining transportability. The selected material must be compatible with the operating environment and the maintenance requirements of the equipment.
Other possible applications include transportation equipment, precision machinery, industrial structures, and custom fastening systems. The suitability of a particular alloy depends on the technical requirements of the end product. The supplier’s broad aluminum material portfolio allows customers to discuss rivet wire together with related welding or fabrication materials when a project requires multiple aluminum products.
How the Product Supports Customer Competitiveness
For rivet manufacturers, material consistency has a direct effect on production efficiency. Stable wire can reduce adjustments to cutting and heading equipment, minimize unexpected tooling wear, and support more predictable output. When defects and dimensional deviations are reduced, the manufacturer may also lower scrap rates and inspection costs.
For aircraft and aerospace component manufacturers, reliable material supply supports production planning. A supplier that can provide multiple alloy grades, controlled conditions, technical communication, and traceable documentation can simplify procurement. This is particularly useful for customers managing several aluminum material requirements across different programs.
Customization is another important advantage. Different customers may require different wire diameters, packaging formats, minimum order quantities, certification documents, or inspection items. A manufacturer that communicates closely with the customer can align the production and inspection plan with the actual application instead of providing a generic material that may require additional processing.
International supply capability is also relevant. The company exports its products to overseas high-end markets and has developed experience supporting customers beyond its domestic region. Export-oriented production requires attention to packaging, labeling, documentation, delivery coordination, and consistent product identification.
Competitive performance should not be judged only by the initial material price. Total value can also include reduced production interruptions, lower scrap, dependable delivery, fewer quality claims, technical responsiveness, and product life-cycle performance. High-strength aluminum alloy wire that performs consistently in the customer’s process may provide greater value than a lower-cost material with higher variability.
Quality, Traceability, and Technical Communication
Traceability is especially important for aerospace and other safety-sensitive applications. Each batch should be identifiable through appropriate labels, production records, test data, and shipment documentation. Traceability helps customers confirm the material received, investigate any nonconformity, and maintain records for internal or regulatory requirements.
Technical communication should begin before production. Customers should provide the intended alloy, temper, wire diameter, dimensional tolerance, surface requirements, delivery form, applicable standard, and required test documentation. If the material will be used to make rivets, information about cutting, heading, heat treatment, and installation can help the supplier recommend a more suitable condition.
Where a custom grade or special requirement is involved, sample evaluation may be appropriate. Trial material can be tested in the customer’s forming equipment to evaluate feeding, cutting, heading, hardness, surface appearance, and final rivet performance. Results from the trial can then be used to confirm or refine the production specification.
Customers should also clarify whether they require a specific national or international standard. The composition ranges shown in product information provide useful guidance, but final acceptance should be based on the agreed technical specification. Documentation may include a certificate of conformity, chemical analysis report, mechanical test report, heat-treatment record, dimensional inspection record, or other agreed documents.
Environmental and Sustainability Considerations
Aluminum is valued for its low density and recyclability. In transportation applications, reducing structural weight can contribute to lower energy consumption during operation. At the end of a product’s service life, aluminum components can be recovered and recycled through established metal-recycling systems.
Using the correct alloy and condition can also support longer service life. Improved corrosion resistance, fracture toughness, and resistance to environmental cracking may reduce the risk of premature replacement when the material is properly designed, installed, inspected, and maintained. Longer-lasting assemblies can reduce material consumption over the life of the equipment.
Manufacturing efficiency is another sustainability factor. Better control of casting, drawing, heat treatment, and inspection can reduce scrap and avoid unnecessary reprocessing. Consistent wire dimensions can improve the yield of rivet production and reduce the number of rejected blanks and finished fasteners.
Sustainability should be considered together with safety and performance. The lowest material consumption is not always the best engineering outcome if it leads to premature failure or excessive maintenance. A properly selected high-strength aluminum alloy can offer a balanced combination of low weight, reliable performance, and efficient use of resources.
Recommended Selection Process
The first step is to define the application. Customers should identify whether the wire will be used for aircraft rivets, aerospace fasteners, military equipment, general structural rivets, or another product. The operating temperature, moisture exposure, vibration, stress level, expected service life, and inspection requirements should also be considered.
The second step is to select the alloy family. High-strength copper-, magnesium-, or zinc-containing alloys may provide different properties and processing responses. The listed grades should be evaluated according to the required strength, ductility, corrosion resistance, toughness, heat-treatment response, and compatibility with the joined materials.
The third step is to select the temper or supply condition. T6, T73, and T76 represent different balances of strength and environmental performance. The condition should be matched to the rivet-forming process and the final service requirements.
The fourth step is to define dimensional and delivery requirements. These may include wire diameter, tolerance, coil weight, straightness, surface finish, length, packaging, labeling, and quantity. Clear requirements help prevent misunderstandings and allow the manufacturer to prepare an appropriate production plan.
The final step is to confirm testing and documentation. Chemical composition, mechanical properties, dimensional checks, surface inspection, heat-treatment records, and certificates may be required depending on the application. A formal technical review is recommended for aerospace and military projects.
| Selection Item | Questions to Confirm |
|---|---|
| Application | What type of rivet or fastener will be produced, and where will it be used? |
| Alloy | Which grade provides the required strength, ductility, corrosion resistance, and compatibility? |
| Temper | Is the priority maximum strength, fracture toughness, stress corrosion resistance, or a balanced performance? |
| Dimensions | What wire diameter, tolerance, straightness, and delivery form are required? |
| Processing | Will the wire be cut, headed, upset, heat treated, or otherwise formed after delivery? |
| Quality documents | Which certificates, test reports, traceability records, and standards are required? |
Frequently Asked Questions
What is high-strength aluminum alloy rivet wire?
It is aluminum alloy wire manufactured for conversion into rivets and related fasteners. Compared with general-purpose aluminum wire, it requires closer control of alloy composition, dimensions, surface condition, mechanical properties, and forming behavior.
Which industries use this product?
The principal target industries are aviation, aerospace, and military manufacturing. It may also be considered for transportation, industrial equipment, structural assemblies, and customized fastening applications when the selected alloy and condition meet the design requirements.
What are the main advantages of aluminum rivet wire?
The main advantages include low density, a favorable strength-to-weight ratio, compatibility with many aluminum structures, useful forming characteristics, and the availability of alloy and temper options. Properly selected material can also provide resistance to fracture, stress corrosion, exfoliation corrosion, and low-temperature service conditions.
What is the difference between T6, T73, and T76?
T6 is identified with high strength. T73 is associated with relatively high fracture toughness, stress corrosion resistance, exfoliation corrosion resistance, and low-temperature performance. T76 provides higher strength than T73 and higher stress corrosion resistance than T6. The appropriate condition depends on the complete application and manufacturing process.
Can the wire be customized?
Customization can be discussed for alloy grade, temper, diameter, tolerance, packaging, delivery format, inspection requirements, and quantity. Customers should provide detailed application information so that the proposed material can be matched to the rivet design and processing route.
Are all listed aluminum grades intended for rivets?
No. The product information includes both high-strength alloy grades and aluminum or aluminum-magnesium welding material grades. Some grades are more appropriate for rivets, while others are intended for welding or related applications. The final use should be confirmed before ordering.
How is quality controlled during production?
Quality control can include alloy composition analysis, process inspection, dimensional measurement, surface inspection, heat-treatment control, mechanical testing, and final documentation. The company states that it applies quality inspection throughout production and operates under ISO 9001 and IATF 16949 quality management systems.
What information should be included in an inquiry?
An inquiry should include the intended application, alloy grade, temper, wire diameter, dimensional tolerance, delivery form, estimated quantity, packaging requirements, applicable standard, required inspection documents, and any special forming or heat-treatment information.
How should aluminum alloy wire be stored?
The wire should be kept clean, dry, protected from moisture and contamination, and handled carefully to avoid impact or deformation. Original identification and batch information should be preserved to maintain traceability.
Can the material be used directly in aerospace production?
Use in aerospace production depends on the customer’s approved specifications, qualification procedures, quality requirements, and applicable regulations. The material should be reviewed and accepted by the responsible engineering and quality departments before use in safety-sensitive components.
Conclusion
High-strength aluminum alloy wire for rivets is a specialized material for lightweight, reliable, and demanding structural connections. Its value comes from the combination of controlled alloy chemistry, suitable heat-treatment conditions, precision wire processing, consistent surface quality, and application-oriented technical support.
The listed T6, T73, and T76 conditions provide different performance directions, allowing customers to consider strength, fracture toughness, stress corrosion resistance, exfoliation corrosion resistance, and low-temperature behavior. The broad range of aluminum alloy grades also supports diverse requirements across aerospace, military, transportation, welding, and industrial applications.
Jiangsu Hetuo Aluminum Wire Co., Ltd. strengthens this product offering through an intelligent manufacturing system, a 40,000-square-meter factory, experienced management and technical personnel, advanced equipment, process-wide inspection, and ISO 9001 and IATF 16949 quality management certifications. Its production capabilities and customization approach can help customers select aluminum wire that is better aligned with their rivet manufacturing process and service environment.
For the best result, customers should define the application, alloy, temper, dimensions, forming process, quality standard, and documentation requirements before placing an order. With the correct material selection and controlled manufacturing process, aluminum alloy rivet wire can support strong, lightweight, durable, and efficient assemblies for demanding global industries.
References
1. Product information for high-strength aluminum alloy wire for rivet applications, including alloy grades, chemical composition, and temper characteristics.
2. Aluminum Association, Aluminum Standards and Data, technical guidance on aluminum alloys and temper designations.
3. ASTM International, Standard Specifications for Aluminum and Aluminum-Alloy Wire and Related Products.
4. International Organization for Standardization, ISO 9001, Quality Management Systems—Requirements.
5. International Automotive Task Force, IATF 16949, Quality Management System Requirements for Automotive Production and Relevant Service Parts Organizations.
6. Standard aerospace materials references covering precipitation-strengthened aluminum alloys, corrosion resistance, fracture toughness, and heat-treatment conditions.
7. General engineering references on aluminum alloy forming, precipitation hardening, riveted-joint design, and aerospace fastener manufacturing.