

 English
 中文简体
 русский
 Deutsch
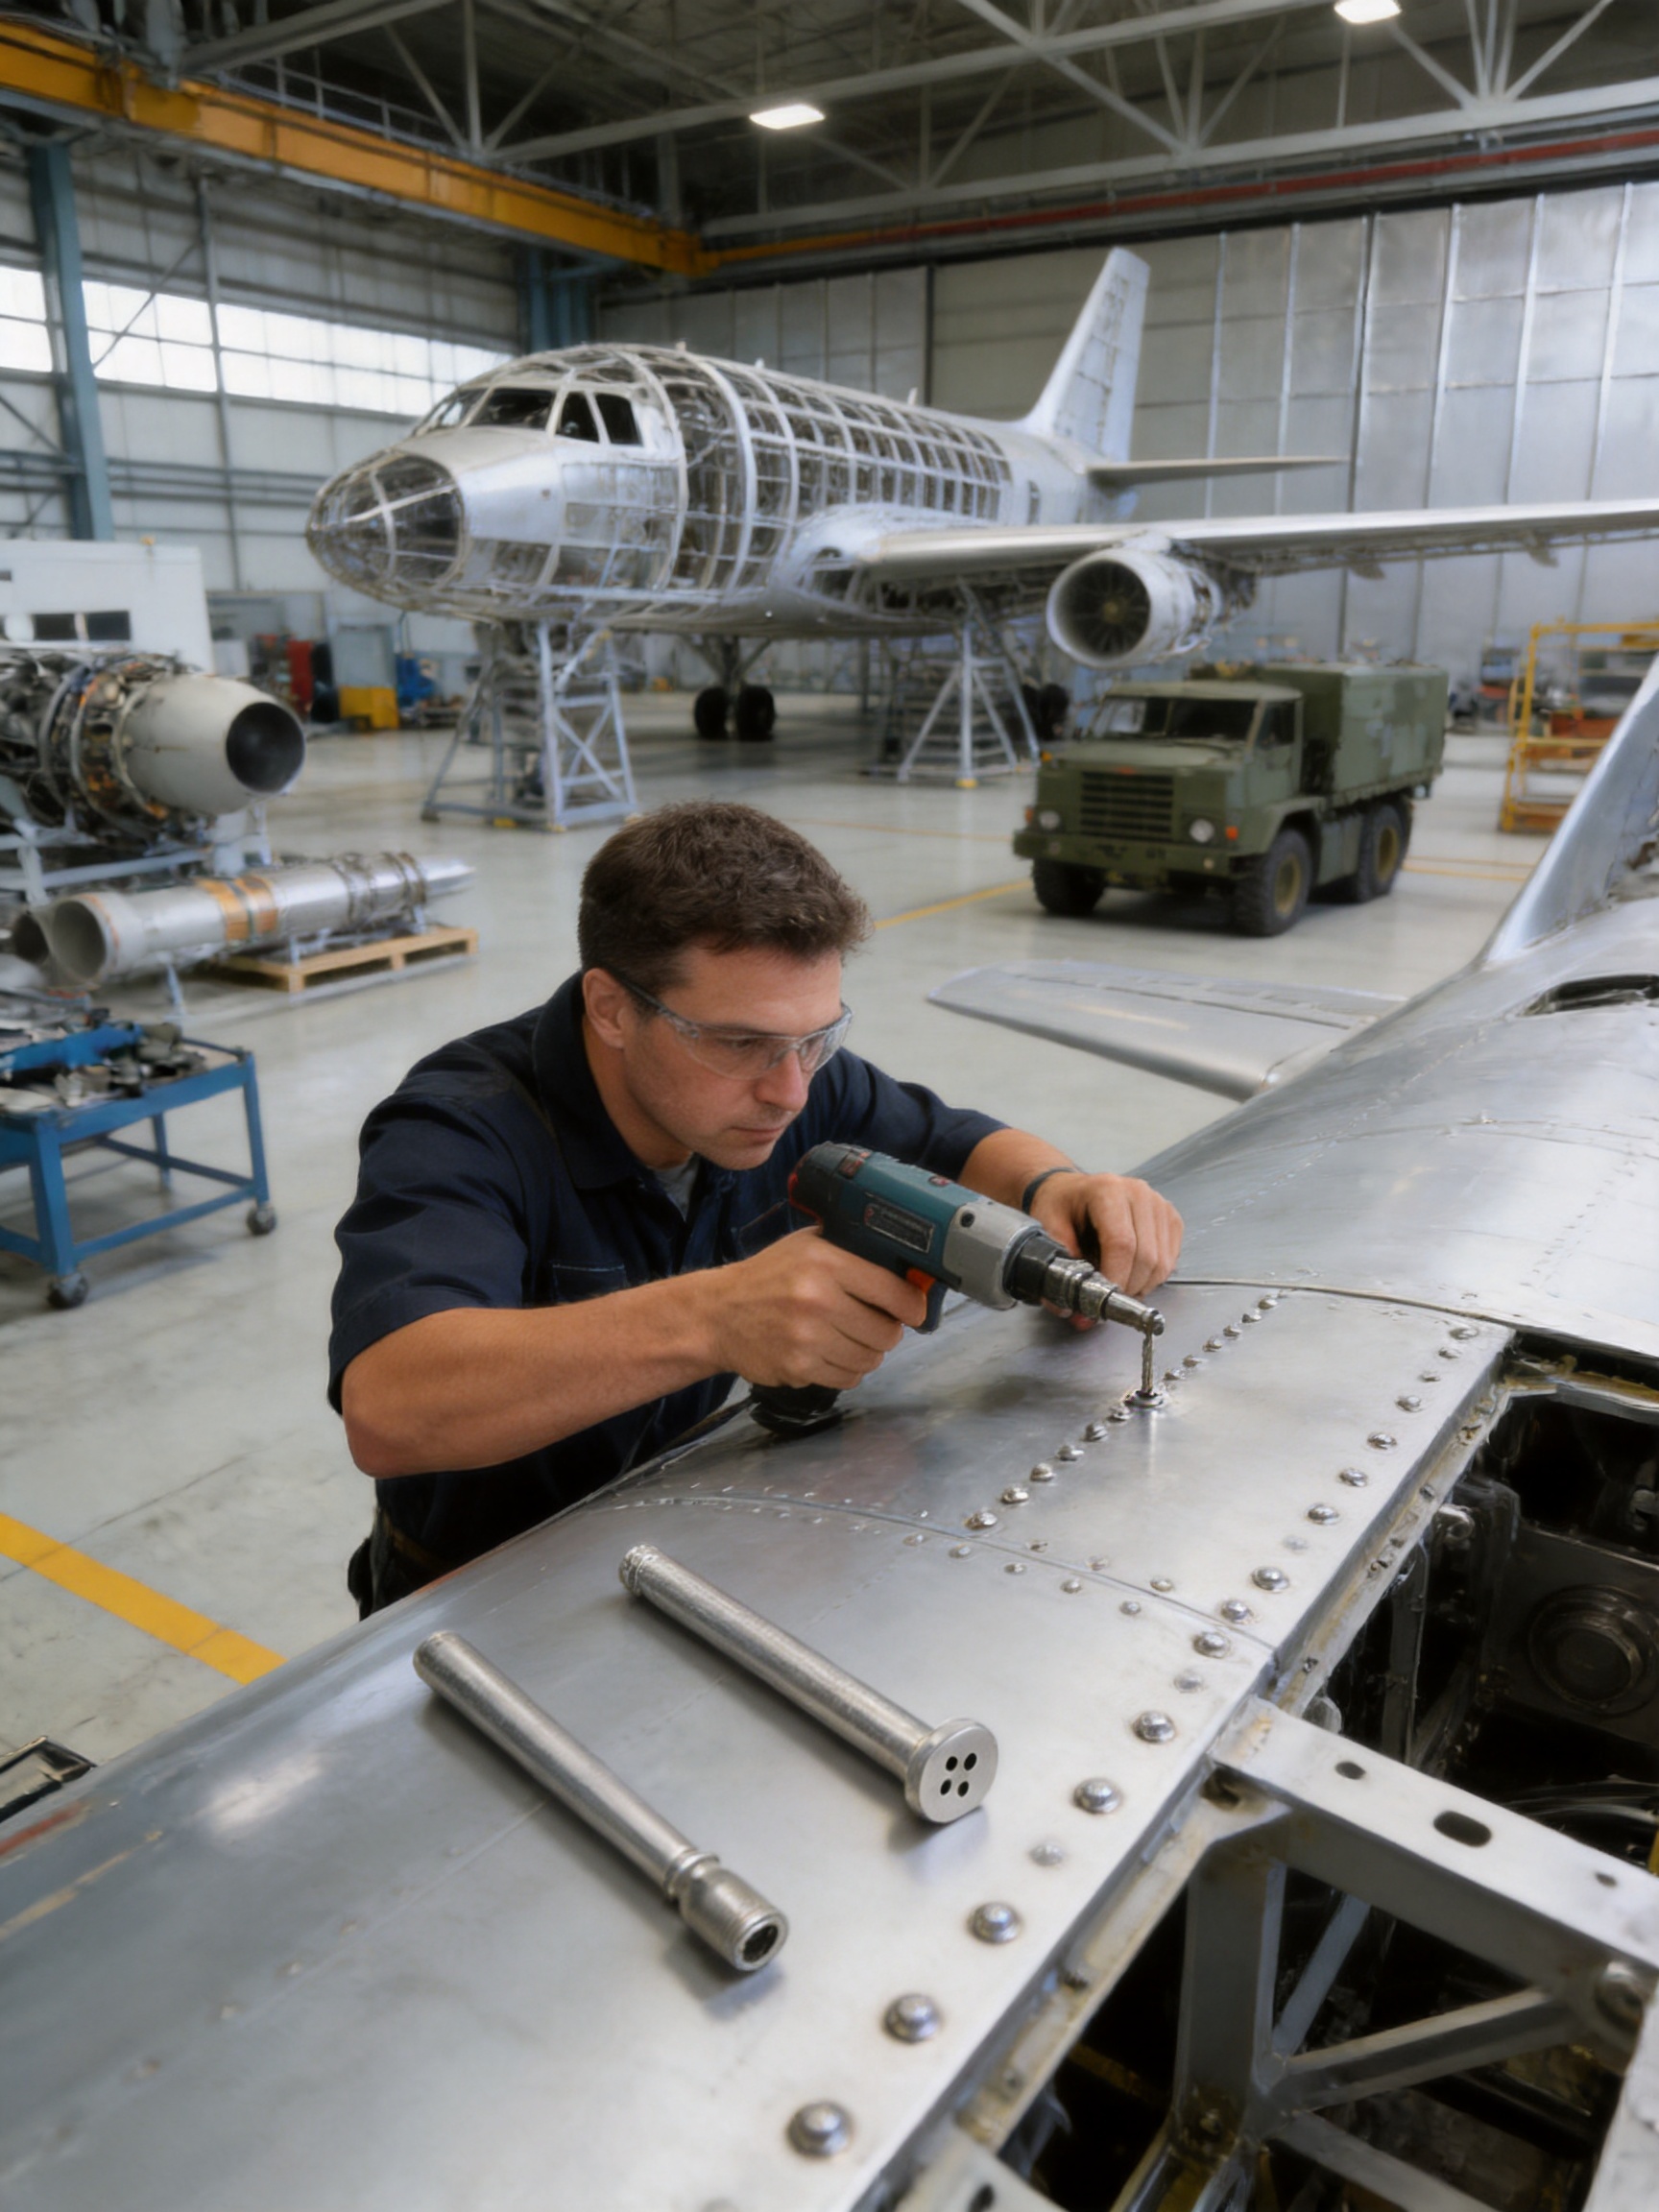
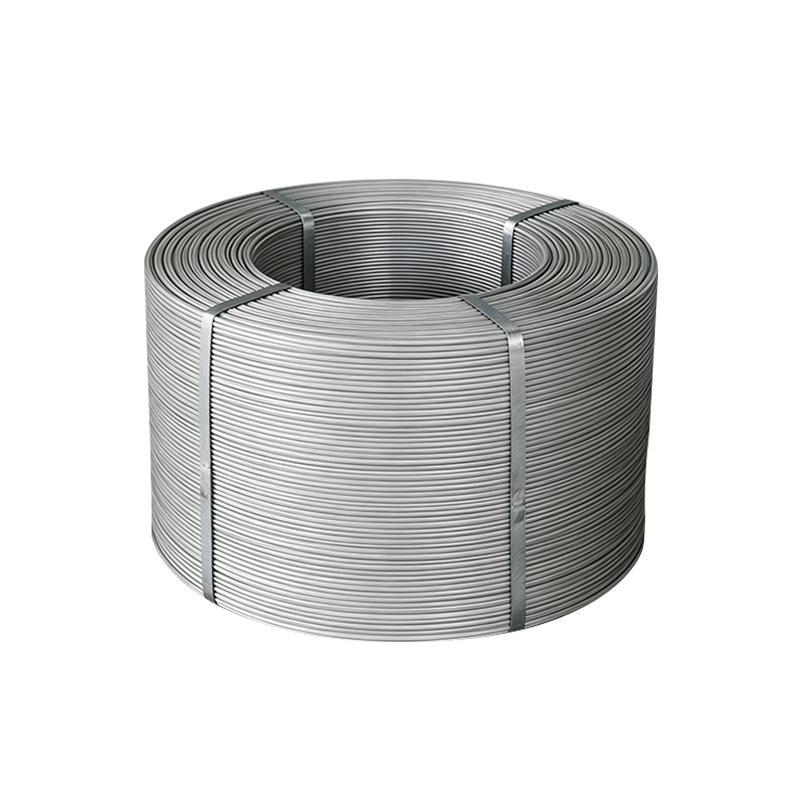
High-strength aluminum alloy wire for rivets is an essential material for industries that require reliable fastening, low structural weight, and consistent mechanical performance. Rivets produced from aluminum alloy wire are widely used in aircraft structures, aerospace assemblies, military equipment, transportation systems, and other applications where a permanent mechanical joint must withstand vibration, fatigue, corrosion, and demanding service conditions.
Compared with ordinary steel rivet materials, aluminum alloy rivet wire offers a valuable combination of low density, good formability, corrosion resistance, and high specific strength. These characteristics allow manufacturers to reduce structural weight without sacrificing the strength required for dependable fastening. When the correct alloy, temper, diameter, and heat treatment are selected, aluminum rivets can provide long-term service in complex environments.
Jiangsu Hetuo Aluminum Wire Co., Ltd. supplies high-strength aluminum alloy wire for rivet manufacturing, with product options including 2A10, 2219, 7050, and 7075. The company also manufactures high-purity aluminum wire and aluminum and aluminum alloy welding materials. Its manufacturing system is designed to support demanding industrial applications through controlled alloy preparation, precision wire processing, strict inspection, and quality management based on ISO 9001 and IATF 16949 systems.
Content
- 1 Understanding High-Strength Aluminum Alloy Rivet Wire
- 2 Why Aluminum Alloy Wire Is Used for Rivets
- 3 Principal Alloy Options for Rivet Applications
- 4 Typical Chemical Composition Range
- 5 Temper Selection and Performance Balance
- 6 Manufacturing Process for High-Strength Rivet Wire
- 7 Quality Control and Inspection
- 8 Advantages Compared with Conventional Rivet Wire Suppliers
- 9 Applications of Aluminum Alloy Rivet Wire
- 10 How to Select the Correct Rivet Wire
- 11 Installation and Joint Design Considerations
- 12 Storage and Handling Recommendations
- 13 Environmental and Sustainability Benefits
- 14 Frequently Asked Questions
- 14.1 What is high-strength aluminum alloy rivet wire?
- 14.2 Which aluminum alloy is best for rivets?
- 14.3 What is the difference between T6, T73, and T76?
- 14.4 Can 7075 aluminum wire be used for aviation rivets?
- 14.5 Are all aluminum welding wire grades suitable for rivets?
- 14.6 Why is chemical composition important?
- 14.7 What inspections should be requested for aerospace rivet wire?
- 14.8 Can the product be customized?
- 14.9 How should the wire be stored?
- 15 Conclusion
- 16 References
- 17 Product: For Rivets
Understanding High-Strength Aluminum Alloy Rivet Wire
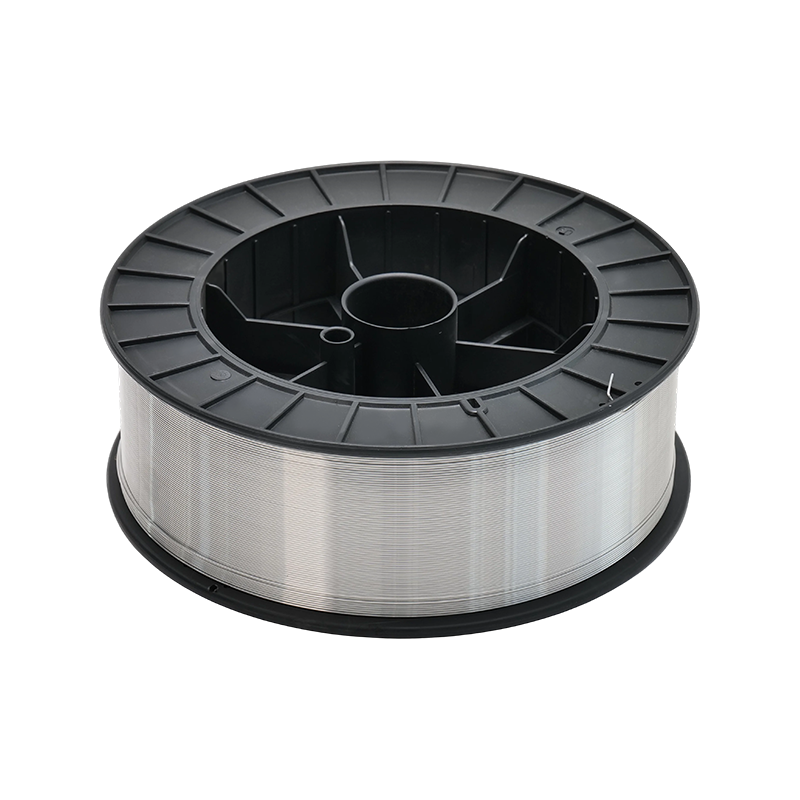
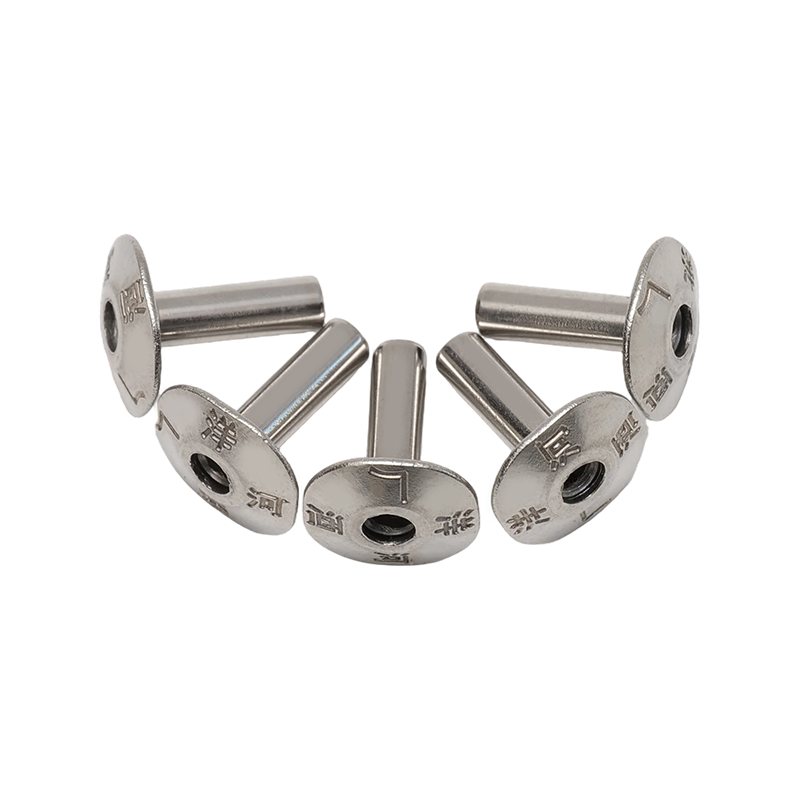
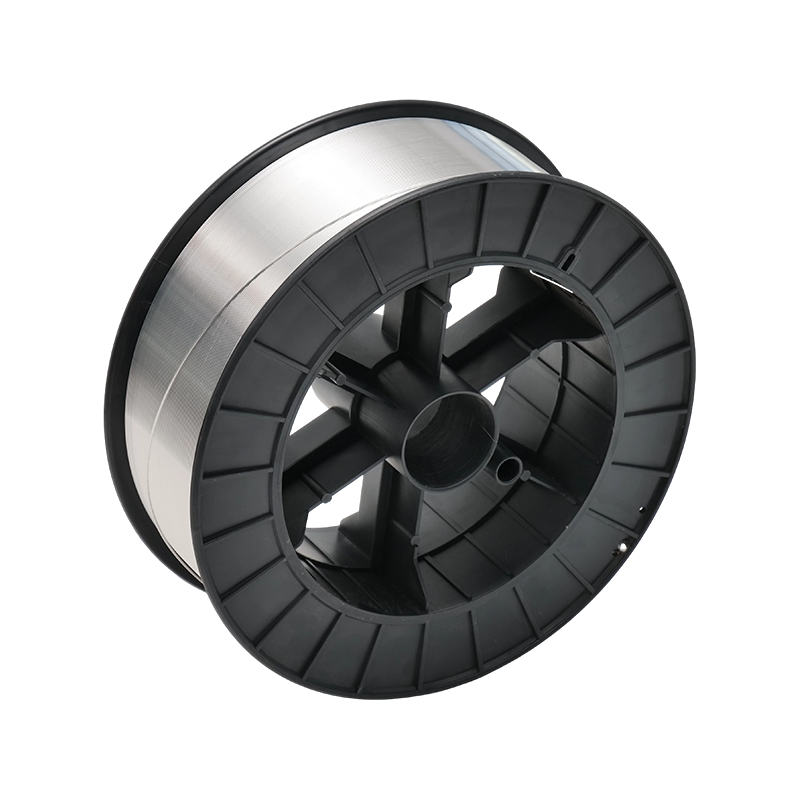
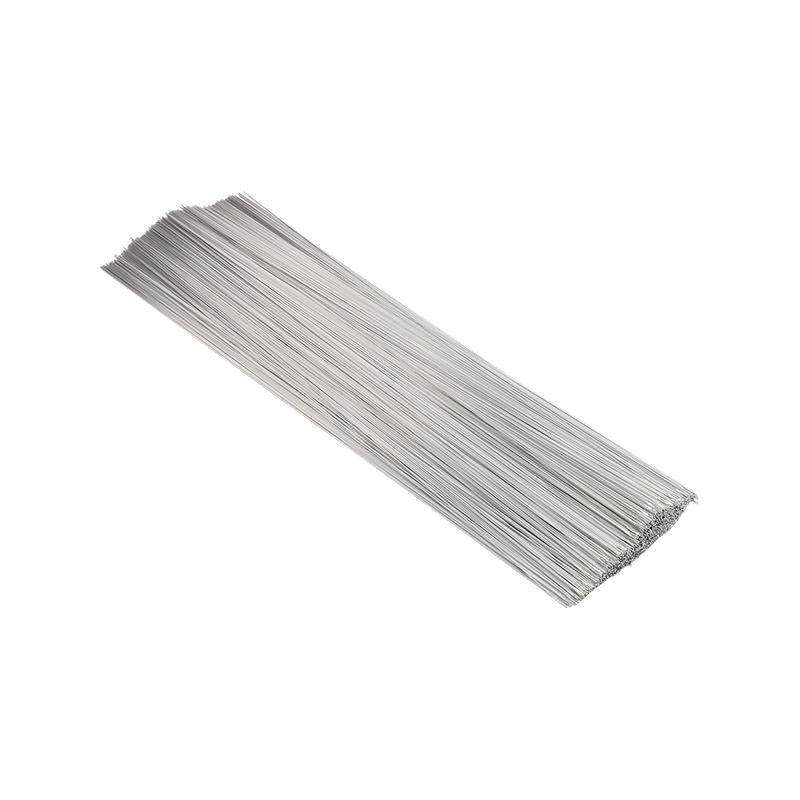
Rivet wire is semi-finished aluminum alloy material supplied in a continuous wire form. It is cut into suitable lengths and then formed into rivets through processes such as cold heading, hot heading, upsetting, trimming, and heat treatment. The wire must therefore possess a carefully controlled balance of strength, ductility, surface quality, dimensional consistency, and response to forming.
High-strength aluminum alloy wire is different from general-purpose aluminum wire. Pure aluminum wire is valued for its electrical conductivity, softness, and corrosion resistance, but it does not normally provide the mechanical strength required for highly loaded riveted joints. Alloying elements such as copper, magnesium, zinc, manganese, chromium, zirconium, and titanium are added to improve strength, heat-treatment response, fracture resistance, corrosion performance, or processing characteristics.
The alloy selection depends on the intended service environment and rivet manufacturing process. Copper-bearing alloys such as 2A10 and 2219 can provide strong precipitation-hardening potential. Zinc-containing alloys such as 7050 and 7075 offer very high strength after suitable heat treatment. Each alloy must be evaluated not only for its tensile strength, but also for its heading behavior, hardness, stress-corrosion resistance, fracture toughness, and compatibility with the parts being joined.
For aviation and aerospace applications, the wire must meet demanding requirements throughout its entire production route. Small variations in chemical composition, internal cleanliness, surface condition, or final temper can affect rivet forming and joint reliability. For this reason, a qualified supplier must control the material from melting and casting through rolling, drawing, heat treatment, inspection, packaging, and traceability.
Why Aluminum Alloy Wire Is Used for Rivets
Low Density and Weight Reduction
Aluminum has a density substantially lower than steel and many other structural metals. A riveted assembly containing thousands of fasteners can therefore achieve a meaningful reduction in total weight by using aluminum alloy rivets. Weight savings are particularly important in aircraft, spacecraft, high-speed vehicles, rail equipment, and mobile military systems.
Reducing fastener weight can also improve overall energy efficiency. A lighter aircraft requires less fuel, a lighter vehicle consumes less energy, and a lighter transport structure can carry a greater useful payload. Aluminum rivet wire supports these goals while retaining the mechanical characteristics needed for permanent fastening.
High Specific Strength
Although aluminum alloys are lighter than steel, high-strength grades can deliver an excellent strength-to-weight ratio. The specific strength of a material is especially important in aerospace design, where every component must contribute to structural integrity without adding unnecessary mass.
Alloys such as 7050 and 7075 are widely recognized for their high strength potential. Copper-bearing alloys such as 2A10 and 2219 are also suitable for specialized applications requiring high strength and a controlled response to heat treatment. The final performance depends on alloy chemistry, processing history, wire size, and temper condition.
Corrosion Resistance
Aluminum naturally forms a thin oxide film when exposed to air. This oxide layer helps protect the underlying metal from further oxidation. The corrosion performance of a rivet, however, depends on the alloy composition, heat treatment, surface condition, contact with other materials, and surrounding environment.
For applications exposed to moisture, salt spray, temperature variation, or industrial contaminants, the material should be selected with attention to stress-corrosion resistance and exfoliation-corrosion resistance. The T73 and T76 conditions are particularly important when the application requires improved resistance to stress corrosion and exfoliation corrosion compared with a peak-strength T6 condition.
Good Formability and Rivet Production Efficiency
Rivet wire must be capable of being cut and formed without cracking, excessive tool wear, or dimensional instability. Aluminum alloys can be formed efficiently when the material has the appropriate temper and surface condition. Consistent wire diameter and straightness also help automated rivet-making equipment maintain stable production rates.
The forming behavior of a rivet wire is influenced by the alloy, hardness, reduction schedule, annealing practice, grain structure, and final drawing process. A supplier with controlled production capabilities can help customers select the appropriate condition for cold heading, hot heading, or other forming operations.
Vibration and Fatigue Considerations
Aircraft and other mobile structures experience repeated vibration and cyclic loading. A riveted joint must remain secure even when subjected to repeated stress, thermal expansion, and mechanical movement. Aluminum alloy rivets can provide reliable performance when the alloy, rivet geometry, installation method, and joint design are properly matched.
Fatigue performance is not determined by the wire alone. It also depends on hole quality, installation force, clamping pressure, surface treatment, joint configuration, and load distribution. High-quality wire helps create rivets with uniform heads, predictable mechanical properties, and reduced risk of defects that could become fatigue initiation points.
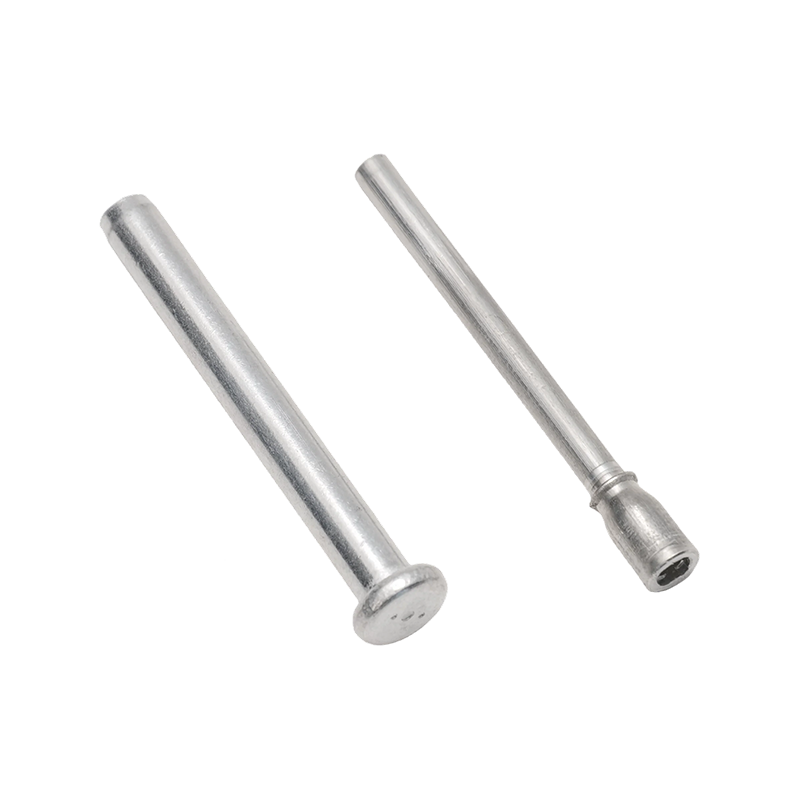
For Rivets
Principal Alloy Options for Rivet Applications
The product range includes several high-strength and application-oriented aluminum alloys. Some grades are intended primarily for high-strength rivets, while other grades in the broader product portfolio are used for welding or specialized joining applications. The correct grade should always be selected according to the customer’s technical specification and the final service conditions.
2A10 Aluminum Alloy Wire
2A10 is a copper-containing high-strength aluminum alloy. Its listed copper content is approximately 3.9% to 4.5%, with manganese and magnesium additions that support strength and heat-treatment response. The alloy is suitable for applications where high mechanical performance is required and where the manufacturing process can accommodate a heat-treatable aluminum alloy.
2A10 wire can be considered for high-strength rivets used in structural assemblies. Its performance is related to precipitation strengthening, in which controlled heat treatment produces fine strengthening phases within the aluminum matrix. The final temper and processing route are important because excessive hardness can reduce forming capability, while insufficient treatment can reduce finished rivet strength.
2219 Aluminum Alloy Wire
2219 contains approximately 5.8% to 6.8% copper, together with controlled manganese, vanadium-related or transition-element additions depending on the applicable specification, and other minor elements. It is a heat-treatable alloy known for high strength, good weldability relative to many other high-strength copper-bearing alloys, and useful performance at elevated temperatures.
2219 can be considered for aerospace components and high-performance structures where strength and temperature capability are important. When supplied as rivet wire, the manufacturing condition should be selected to provide sufficient formability during rivet production while allowing the finished fastener to achieve the required mechanical properties after treatment.
7050 Aluminum Alloy Wire
7050 is a high-zinc aluminum alloy containing approximately 5.7% to 6.7% zinc, 1.9% to 2.6% magnesium, and approximately 2.0% to 2.6% copper. It is designed for high-strength applications and can provide an advantageous balance between strength, fracture toughness, and stress-corrosion performance when processed in suitable tempers.
The T73 condition is associated with relatively high fracture toughness and improved resistance to stress corrosion, exfoliation corrosion, and low-temperature service conditions. The T76 condition offers higher strength than T73 while maintaining higher stress-corrosion resistance than a T6 condition. These temper choices allow designers to prioritize different performance requirements.
For demanding aerospace rivet applications, the ability to select among T6, T73, and T76-related performance objectives can be a significant advantage. The appropriate condition should be confirmed through engineering review and applicable standards because rivet forming, installation, and final heat treatment requirements can vary.
7075 Aluminum Alloy Wire
7075 is one of the best-known high-strength aluminum alloys. Its principal alloying elements include zinc at approximately 5.0% to 7.0%, magnesium at approximately 1.8% to 2.8%, and copper at approximately 1.4% to 2.0%. Chromium and other controlled additions contribute to the overall performance of the alloy.
7075 wire is suitable for applications requiring a high strength-to-weight ratio. It can be used for custom rivet wire and specialized aerospace fastening products when the customer’s design, forming process, and heat-treatment requirements are properly established. The alloy is especially attractive where minimizing fastener weight and maximizing mechanical strength are important.
Because 7075 is a high-strength alloy, forming conditions require careful control. The supplier must manage reductions, intermediate treatment, final drawing, and surface quality to reduce the possibility of cracks or other defects during heading. Customers should also consider the service environment and temper selection because high-strength zinc-bearing alloys require appropriate control for stress-corrosion resistance.
Other Aluminum Alloy Grades in the Product Portfolio
In addition to high-strength rivet grades, the product portfolio includes 4043, 4047, 5183, 5154, 5356, AlMg3, AlMg5, AlMg6, and AlMg61. These alloys are generally associated with aluminum and aluminum alloy welding materials or other joining applications rather than being universal substitutes for high-strength rivet wire.
4043 and 4047 contain higher levels of silicon and are commonly selected for welding applications where fluidity and crack resistance are important. 5183, 5356, and magnesium-containing grades are used where weld strength, corrosion performance, and compatibility with aluminum base materials are required. A broad alloy portfolio allows the supplier to support both mechanical fastening and welding-related projects from one manufacturing source.
Typical Chemical Composition Range
The following table summarizes the listed composition values for selected grades. Values are presented as percentages by mass based on the supplied product information. “Rest” indicates the balance of the composition is aluminum. A dash indicates that no specific value was listed in the provided material. Final acceptance should be based on the applicable national or international material specification and the supplier’s inspection certificate.
| Grade | Si | Fe | Cu | Mn | Mg | Cr | Zn | Ti | Zr | Other | Al |
|---|---|---|---|---|---|---|---|---|---|---|---|
| 2A10 | 0.25 | 0.20 | 3.9–4.5 | 0.30–0.50 | 0.15–0.30 | — | 0.10 | 0.15 | — | 0.05–0.10 | Rest |
| 2219 | 0.20 | 0.30 | 5.8–6.8 | 0.2–0.4 | 0.02 | — | 0.10 | 0.02–0.10 | — | 0.05–0.15 | Rest |
| 7050 | 0.12 | 0.15 | 2.0–2.6 | 0.10 | 1.9–2.6 | 0.04 | 5.7–6.7 | 0.06–0.20 | 0.08–0.15 | 0.05–0.15 | Rest |
| 7075 | 0.50 | 0.50 | 1.4–2.0 | 0.2–0.6 | 1.8–2.8 | 0.10–0.25 | 5.0–7.0 | 0.05 | — | 0.05–0.10 | Rest |
| 4043 | 4.5–6.0 | 0.80 | 0.30 | 0.05 | 0.05 | — | 0.10 | 0.20 | — | 0.05–0.15 | Rest |
| 4047 | 11.0–13.0 | 0.80 | 0.30 | 0.15 | 0.10 | — | 0.20 | — | — | 0.05–0.15 | Rest |
| 5183 | 0.40 | 0.40 | 0.10 | 0.5–1.0 | 4.3–5.2 | 0.05–0.25 | 0.25 | 0.15 | — | 0.05–0.15 | Rest |
| 5356 | 0.25 | 0.40 | 0.10 | 0.05–0.20 | 4.5–5.5 | 0.05–0.20 | 0.10 | 0.06–0.20 | — | 0.05–0.15 | Rest |
Temper Selection and Performance Balance
Temper describes the condition of an aluminum alloy resulting from mechanical and thermal treatment. It has a direct influence on strength, ductility, hardness, fracture toughness, corrosion resistance, and forming behavior. A rivet manufacturer should not select a wire solely by alloy designation. The temper must also be matched to the manufacturing method and final performance requirement.
T6 Condition
The T6 condition is commonly associated with high strength obtained through solution heat treatment, quenching, and artificial aging. For certain high-strength aluminum alloys, T6 can provide excellent tensile and yield strength. This makes it attractive for structural applications where maximum strength is the primary objective.
However, the highest available strength is not always the best choice for every riveted joint. Rivets may require a specific level of ductility during forming and installation. In addition, the service environment may create stress-corrosion concerns. Consequently, T6 should be selected only after considering forming behavior, joint design, environmental exposure, and the applicable technical specification.
T73 Condition
T73 is an overaged condition developed to improve fracture toughness and resistance to stress corrosion and exfoliation corrosion. Compared with T6, it generally provides a more favorable corrosion and toughness balance, although its strength can be lower.
This condition is valuable for critical structures exposed to humidity, salt, cyclic loading, or long service periods. The improved resistance to environmentally assisted cracking can help extend component life when the material is used in a properly designed and maintained joint.
T76 Condition
T76 is intended to provide a performance balance between the high strength associated with T6 and the improved stress-corrosion resistance associated with overaged conditions. Based on the supplied product information, T76 offers higher strength than T73 and higher stress-corrosion resistance than T6.
This balance can make T76 attractive for aerospace and military structures that require both load-carrying capability and enhanced environmental resistance. The actual properties must be confirmed by the applicable specification, product form, diameter, heat treatment, and inspection documentation.
Manufacturing Process for High-Strength Rivet Wire
Alloy Preparation and Melting
The manufacturing process begins with controlled alloy preparation. Aluminum and alloying additions must be weighed and introduced in the correct proportions. Chemical composition control is particularly important for high-strength grades because small changes in copper, magnesium, zinc, manganese, or transition elements can influence precipitation behavior and final mechanical properties.
Melting equipment must provide stable temperature control and adequate mixing. The melt may undergo processes intended to reduce hydrogen, nonmetallic inclusions, and other impurities. Clean metal is important for wire products because inclusions or internal defects can reduce ductility, affect fatigue performance, and create cracking during rivet forming.
Casting and Homogenization
After melting, the alloy is cast into a suitable billet, rod, or intermediate form. Casting conditions influence grain structure and segregation. Homogenization heat treatment can then be used to reduce chemical segregation and prepare the material for subsequent deformation.
Stable casting and homogenization practices help create a more uniform starting material. This uniformity supports consistent rolling, drawing, heat treatment, and final wire properties across the length of a production batch.
Rolling and Rod Production
The cast and homogenized material is processed into rod through controlled rolling or related deformation operations. Rolling reduces the cross-sectional area and refines the material structure. The reduction schedule must be suitable for the selected alloy and target wire size.
Uniform rod quality is essential because any significant variation in diameter, surface condition, or internal structure can become more pronounced during drawing. Controlled rolling also contributes to dimensional stability and consistent response during later heat treatment.
Drawing and Precision Sizing
Wire drawing reduces the rod to the specified diameter by pulling it through a series of dies. The drawing schedule, lubrication, die condition, reduction per pass, and intermediate treatment all influence the final product.
Precision drawing is particularly important for rivet wire because the wire is often processed automatically. Dimensional variation can cause inconsistent cut lengths, irregular rivet heads, uneven upsetting, or poor fit in automated forming equipment. A reliable manufacturer monitors diameter, ovality, surface quality, and straightness throughout production.
Intermediate and Final Heat Treatment
Heat treatment is used to control the balance between strength and formability. Depending on the alloy and requested temper, operations can include solution treatment, quenching, natural aging, artificial aging, annealing, or stabilization.
High-strength aluminum alloys are sensitive to heating and cooling conditions. Furnace temperature uniformity, holding time, transfer time, quench conditions, and aging parameters must be controlled. Inadequate treatment can result in inconsistent hardness or strength, while excessive treatment can reduce ductility or cause dimensional changes.
Surface Protection and Handling
The surface of aluminum wire must be protected from damage, contamination, and excessive oxidation during storage and transport. Scratches, dents, embedded particles, and oil residues may affect forming or the quality of the finished rivet.
Careful coiling, packaging, labeling, and handling help preserve the wire’s condition. Product identification should remain clear from production through delivery so that alloy, temper, diameter, batch number, and inspection records can be matched throughout the customer’s manufacturing process.
Quality Control and Inspection
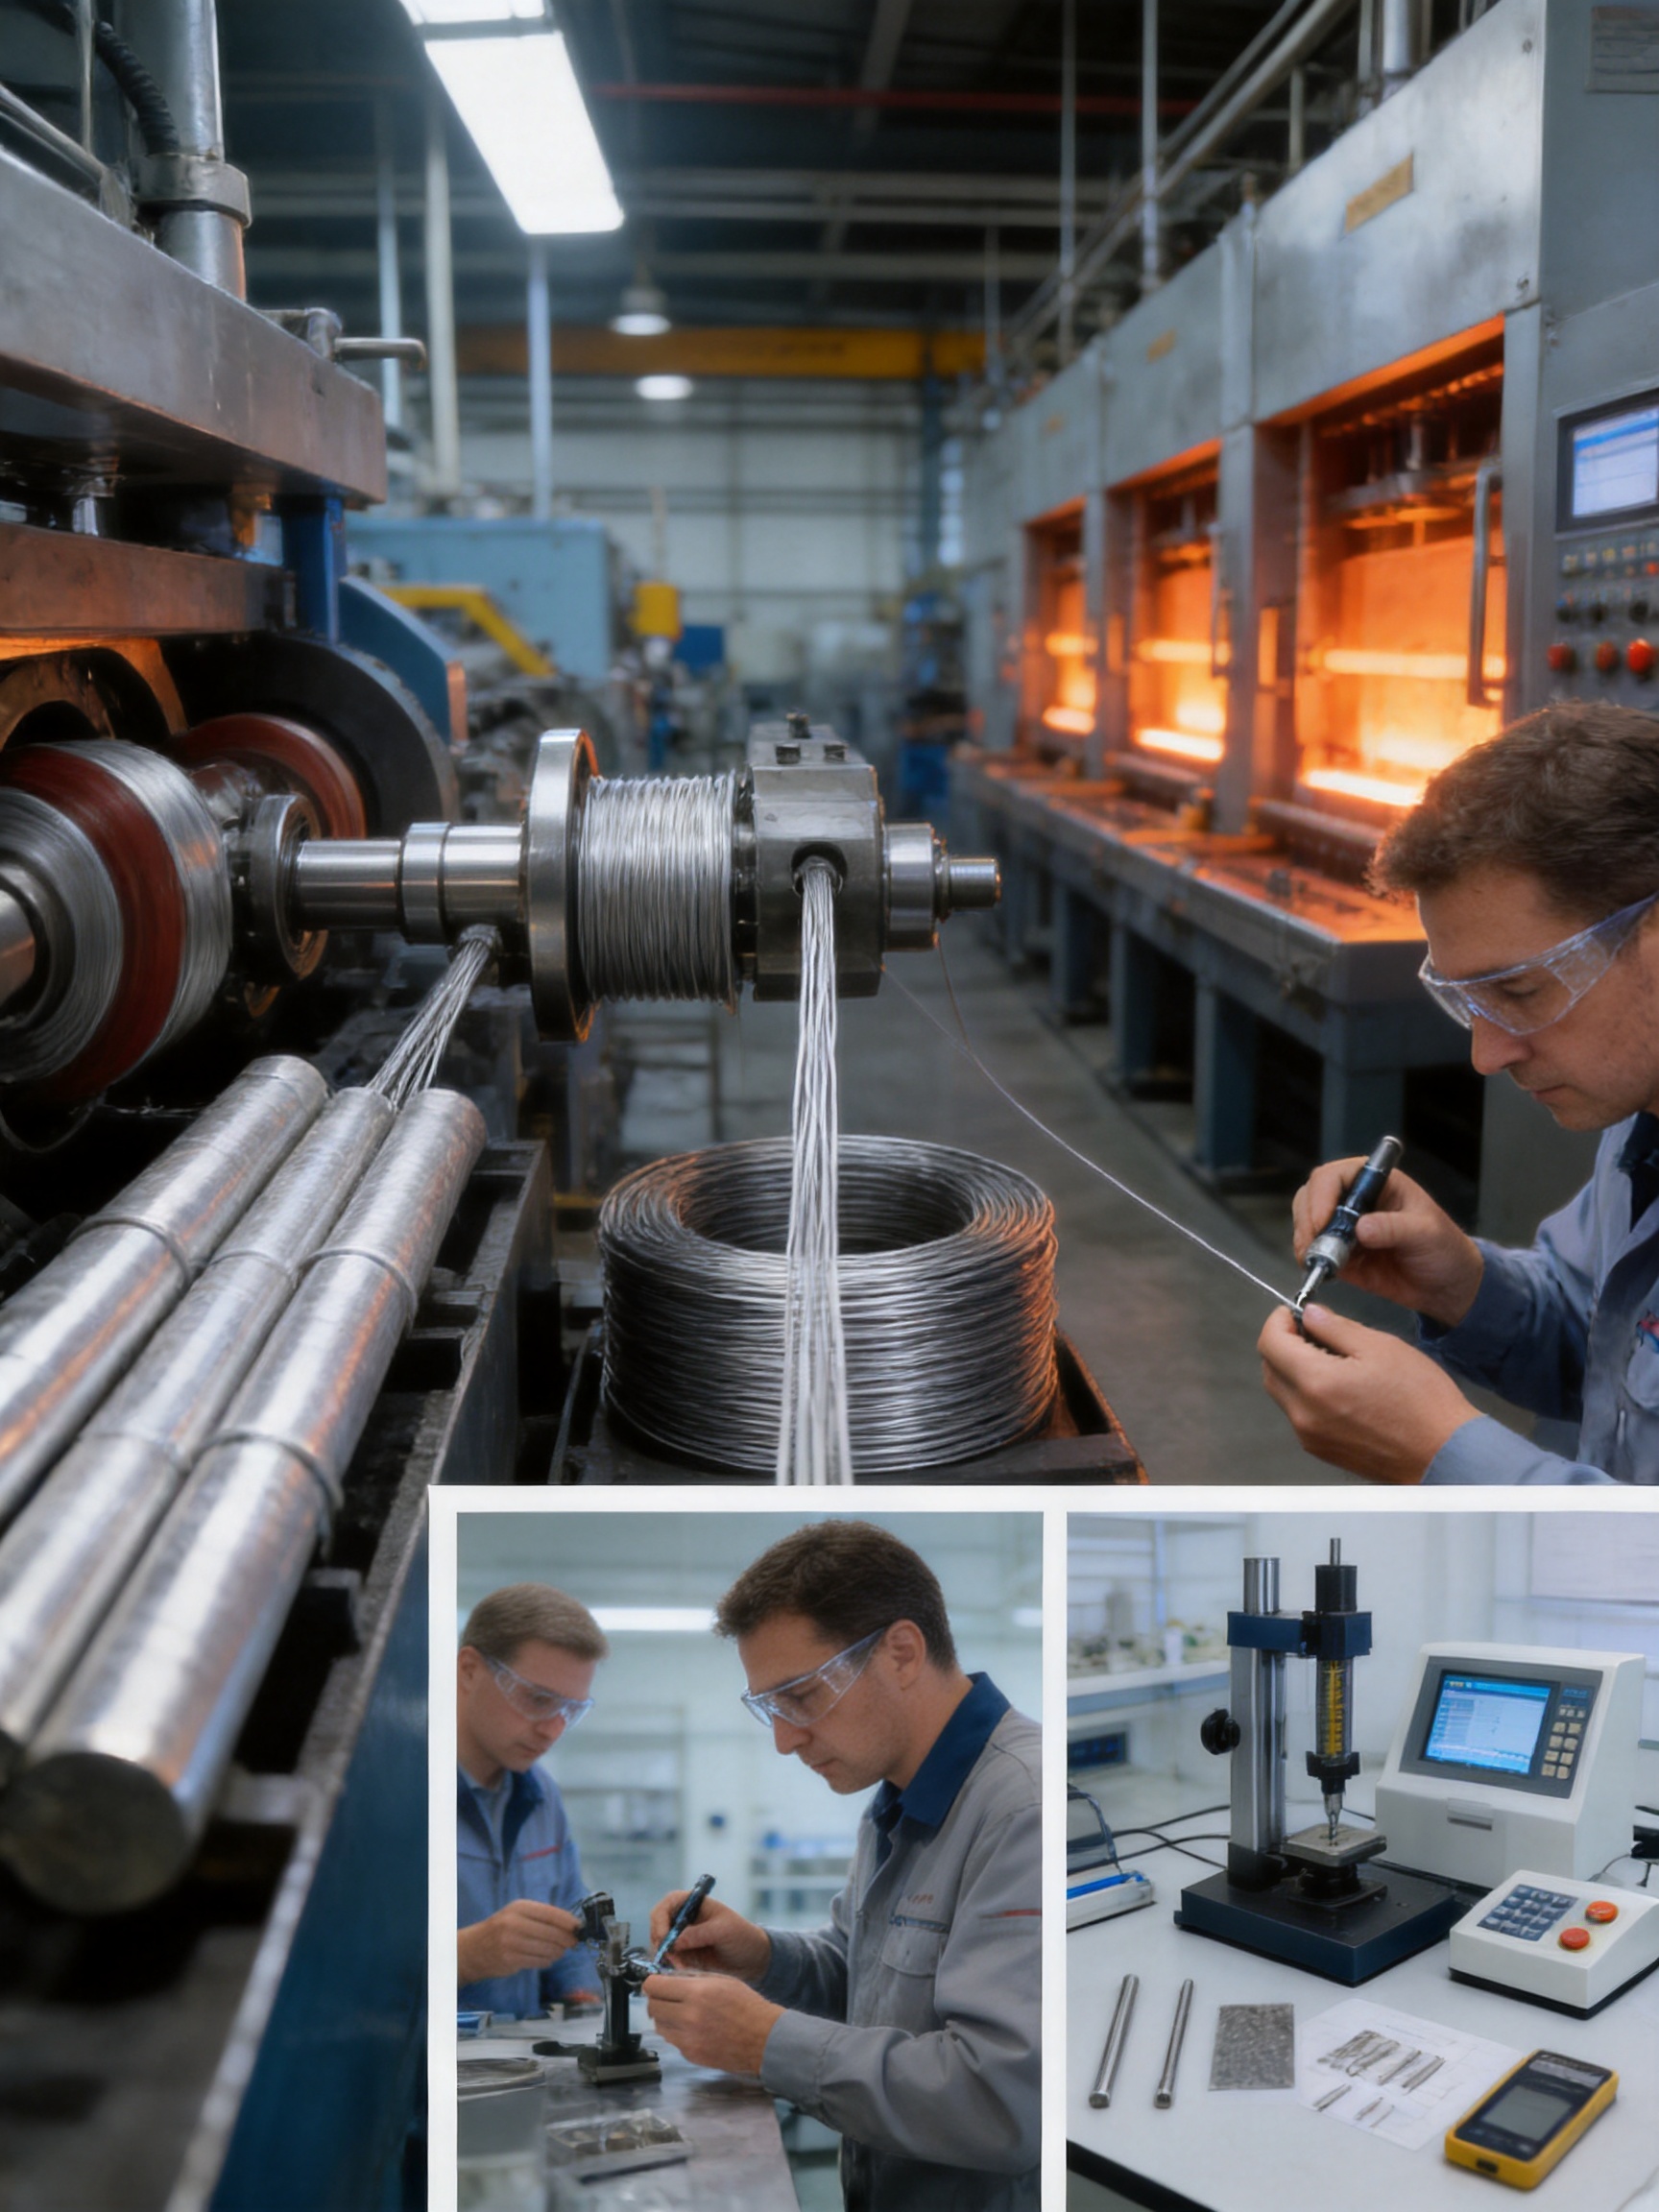
Quality control for rivet wire must extend beyond a single final inspection. Jiangsu Hetuo Aluminum Wire Co., Ltd. states that it implements quality inspection throughout production. This approach is important because a wire product can meet its final diameter requirement while still containing defects introduced during melting, casting, rolling, drawing, or heat treatment.
Chemical Composition Inspection
Chemical analysis confirms that the alloy is within the specified composition range. This is the foundation for consistent heat-treatment response and mechanical performance. A composition certificate should identify the alloy grade, batch, measured elements, and applicable acceptance requirements.
Dimensional Inspection
Diameter, ovality, length, and dimensional consistency are important for automated rivet production. Measuring equipment should be calibrated and inspection results should be recorded. Tight dimensional control helps customers reduce material waste and maintain stable heading operations.
Surface Inspection
Surface inspection can identify scratches, laps, seams, cracks, corrosion, dents, and other conditions that could compromise rivet forming or joint reliability. The required surface condition depends on the customer’s specification and manufacturing process, but clean and defect-free wire is essential for high-quality finished rivets.
Mechanical Testing
Mechanical tests may include tensile strength, yield strength, elongation, hardness, and other tests required by the relevant standard. For high-strength alloys, mechanical testing helps confirm that the selected temper has been achieved consistently.
Additional tests may be appropriate for aerospace or military applications, including fracture toughness evaluation, stress-corrosion testing, exfoliation-corrosion testing, fatigue testing, or metallographic examination. The exact testing program should be agreed upon before production.
Traceability and Documentation
Traceability connects the finished wire to its raw materials, alloy batch, processing route, heat-treatment records, inspection results, and packaging information. This documentation is particularly valuable for safety-critical applications because it supports process verification, customer audits, failure analysis, and long-term quality management.
The company’s ISO 9001 and IATF 16949 certifications demonstrate its commitment to structured quality management. ISO 9001 focuses on consistent quality systems and customer satisfaction, while IATF 16949 provides a more demanding framework associated with automotive supply chains and process control. Together, these systems support disciplined manufacturing and continuous improvement.
Advantages Compared with Conventional Rivet Wire Suppliers
Broad Material Capability
A major advantage is the ability to supply different families of aluminum wire, including high-purity aluminum wire, high-strength alloy wire, and welding materials. Customers can obtain materials for multiple joining and conductivity-related applications from one specialized source rather than coordinating with several unrelated suppliers.
Support for High-Performance Grades
The availability of 2A10, 2219, 7050, and 7075 supports applications that require more than general-purpose aluminum performance. These grades provide options for strength, toughness, temperature capability, and corrosion resistance. A broader grade range allows engineers to optimize the material instead of choosing a single alloy for every application.
Controlled Manufacturing Environment
The company operates a manufacturing facility covering approximately 40,000 square meters and employs approximately 60 people, including professional managers and technicians. This combination of production space, technical personnel, and specialized equipment supports organized manufacturing and process supervision.
An intelligent manufacturing system can improve production consistency by integrating equipment, process parameters, inspection data, and product tracking. For precision wire, process stability is often more valuable than simply increasing output because customers depend on repeatable properties from one batch to the next.
Experience in Demanding End Markets
High-strength aluminum alloy wire is intended for aviation, aerospace, military, transportation, and other high-performance applications. These markets require greater attention to material reliability than many ordinary industrial uses. A supplier familiar with demanding specifications is better positioned to support documentation, inspection, and customized production requirements.
Customization Capability
Rivet wire requirements can vary by alloy, diameter, temper, coil weight, surface condition, packaging, and documentation. Custom 7075 aluminum rivet wire and other made-to-order products can be developed according to customer requirements, subject to technical review and production feasibility.
Customization is useful when a customer has specialized heading equipment, a proprietary rivet design, strict dimensional limits, or a unique heat-treatment route. Early communication between the wire supplier and rivet manufacturer helps prevent problems during trial production.
Applications of Aluminum Alloy Rivet Wire
Aviation Structures
Aircraft structures use permanent fasteners in skins, frames, brackets, panels, and internal assemblies. Aluminum alloy rivets are attractive because they reduce weight and can be compatible with aluminum airframe materials. High-strength grades can support load-bearing applications, while corrosion-resistant tempers can improve durability in challenging service environments.
Aerospace Equipment
Space and aerospace systems require materials with predictable performance under vibration, temperature variation, low pressure, and severe weight restrictions. Rivet wire for these applications must be manufactured and inspected with a high level of discipline. Alloy and temper selection should consider not only static strength but also fracture resistance, thermal exposure, and long-term reliability.
Military Equipment
Military vehicles, aircraft, shelters, equipment housings, and field systems may be exposed to impact, vibration, humidity, dust, salt, and rapid temperature changes. Aluminum alloy rivets can provide durable fastening with reduced weight. The choice between a maximum-strength temper and a more corrosion-resistant temper depends on the equipment’s design and operating environment.
Transportation Equipment
Rail vehicles, marine structures, commercial vehicles, and specialized transport equipment increasingly use lightweight aluminum structures. Riveted joints can be advantageous where welding would cause distortion, require extensive heat input, or complicate maintenance. Aluminum alloy wire gives manufacturers a material option for producing consistent fasteners suited to lightweight structures.
Industrial and Specialized Assemblies
Other possible applications include pressure-resistant housings, industrial enclosures, equipment frames, electrical assemblies, and custom mechanical products. The suitability of a high-strength alloy rivet depends on the joint load, operating temperature, corrosion exposure, galvanic compatibility, and installation method.
How to Select the Correct Rivet Wire
Define the Load Requirements
Begin by identifying tensile, shear, bearing, fatigue, and impact loads. The fastener must be strong enough for the joint without becoming excessively brittle or difficult to form. High-strength alloys may provide excellent static strength, but a lower-strength alloy with better ductility can sometimes be more appropriate for a particular rivet design.
Consider the Service Environment
Humidity, salt spray, chemicals, low temperature, elevated temperature, and contact with dissimilar metals can influence alloy selection. If the joint is exposed to a corrosive environment, stress-corrosion and exfoliation-corrosion resistance should be evaluated along with strength.
Match the Forming Process
Cold heading, hot heading, machining, and other forming methods place different demands on the wire. The requested temper must be compatible with the forming operation. Customers should provide details about forming speed, tooling, reduction, rivet dimensions, and any intermediate or final heat treatment.
Confirm Diameter and Packaging Requirements
Wire diameter affects the rivet blank size, forming force, dimensional accuracy, and material yield. Packaging must protect the wire from mechanical damage and contamination. Coil dimensions and weight should also be compatible with the customer’s pay-off and production equipment.
Request Complete Documentation
For critical applications, customers should request chemical composition results, mechanical test data, heat-treatment records, dimensional inspection results, surface inspection information, and a certificate of conformity. Traceability requirements should be established before the purchase order is released.
Installation and Joint Design Considerations
Even the highest-quality rivet wire cannot compensate for poor joint design or incorrect installation. Hole diameter, hole quality, edge distance, pitch, grip length, rivet hardness, installation force, and head dimensions all affect joint performance.
The hole should be clean, correctly sized, and free from burrs or damage. Excessive clearance can reduce load transfer and allow movement, while an undersized hole can create installation damage or excessive residual stress. The rivet length must provide enough material to form the closing head without creating an oversized or poorly shaped head.
When aluminum rivets are installed into dissimilar metals, galvanic corrosion should be considered. Suitable coatings, sealants, isolating layers, or compatible fastener materials may be required. The finished joint should also be protected from moisture accumulation and contaminants.
Heat treatment after forming may be required for some high-strength alloys. The customer should establish whether the rivet is supplied in a forming condition and then treated after installation, or whether the wire is converted into rivets that are already in the required final condition. This distinction affects production planning, dimensional control, and final inspection.
Storage and Handling Recommendations
Aluminum alloy wire should be stored in a clean, dry, and temperature-controlled environment whenever possible. Direct contact with water, condensation, corrosive chemicals, and contaminated surfaces should be avoided. Packaging should remain intact until the material is ready for use.
Coils should be handled with suitable lifting equipment to prevent deformation and impact damage. The product label should remain attached so that alloy grade, temper, diameter, batch number, and production information are not separated from the material.
Before processing, the wire should be inspected for visible corrosion, scratches, dents, contamination, and packaging damage. Any material that appears inconsistent with the purchase specification should be isolated and reviewed before entering production.
Environmental and Sustainability Benefits
Aluminum is highly recyclable, and production scrap from cutting and forming can generally be collected and returned to an appropriate recycling stream. The low density of aluminum also reduces the operating weight of vehicles and aircraft, which can contribute to lower energy consumption throughout the product life cycle.
Lightweight fastening is one part of a broader strategy for sustainable engineering. When aluminum rivet wire replaces heavier fastener materials without compromising safety or service life, manufacturers may reduce material consumption, transport energy, and operational energy. Long-lasting corrosion-resistant joints can also reduce maintenance requirements and replacement frequency.
Responsible sustainability decisions should include the entire material life cycle, including alloy production, processing energy, product durability, recycling infrastructure, packaging, and transportation. Customers can support better outcomes by selecting the correct material grade, reducing production waste, and maintaining traceability for recycling at the end of service.
Frequently Asked Questions
What is high-strength aluminum alloy rivet wire?
High-strength aluminum alloy rivet wire is a continuous wire product made from heat-treatable or otherwise strengthened aluminum alloys. It is cut and formed into rivets for structural fastening. Typical grades include 2A10, 2219, 7050, and 7075, depending on the required strength, corrosion resistance, toughness, and forming behavior.
Which aluminum alloy is best for rivets?
There is no single best alloy for every rivet application. 7075 and 7050 are suitable when very high strength is important. 2A10 and 2219 may be selected for copper-bearing high-strength applications and aerospace requirements. The correct choice depends on load, environment, forming method, temper, joint design, and applicable standards.
What is the difference between T6, T73, and T76?
T6 is generally associated with high strength after solution treatment and artificial aging. T73 is overaged to improve fracture toughness and resistance to stress corrosion and exfoliation corrosion. T76 is intended to provide higher strength than T73 while offering higher stress-corrosion resistance than T6. The exact properties depend on alloy, product form, and specification.
Can 7075 aluminum wire be used for aviation rivets?
7075 aluminum wire can be considered for custom aviation rivet applications when its alloy, temper, forming behavior, corrosion performance, and inspection documentation meet the aircraft manufacturer’s or engineering specification. Qualification testing and approval may be required before production use.
Are all aluminum welding wire grades suitable for rivets?
No. Welding grades such as 4043, 4047, 5183, 5154, and 5356 are designed primarily for welding performance. They should not automatically be substituted for high-strength rivet alloys. The material must be selected according to the mechanical and forming requirements of the finished fastener.
Why is chemical composition important?
Chemical composition controls the alloy’s strengthening response, corrosion behavior, weldability, ductility, and heat-treatment performance. Consistent composition helps ensure that wire from different production batches behaves predictably during forming and in final service.
What inspections should be requested for aerospace rivet wire?
Customers may request chemical analysis, tensile testing, elongation, hardness, dimensional inspection, surface inspection, heat-treatment records, metallographic evaluation, and corrosion or fracture-related testing when required. The appropriate inspection plan should be based on the customer’s drawing, quality standard, and application risk.
Can the product be customized?
Customization may be available for alloy grade, temper, diameter, coil format, packaging, inspection documentation, and other technical requirements. Customers should provide complete specifications, including the forming process and final application, so the supplier can evaluate feasibility and recommend a suitable product condition.
How should the wire be stored?
The wire should be kept sealed and protected in a clean, dry environment. It should be protected from condensation, water, chemicals, impact, and surface contamination. Product identification and traceability labels should remain with the material throughout storage and production.
Conclusion
High-strength aluminum alloy wire for rivets provides a practical solution for lightweight, durable, and technically demanding fastening applications. Its combination of low density, high specific strength, corrosion resistance, formability, and heat-treatment flexibility makes it suitable for aviation, aerospace, military, transportation, and specialized industrial structures.
The availability of 2A10, 2219, 7050, and 7075 gives engineers several options for balancing strength, toughness, corrosion resistance, and manufacturing performance. The T6, T73, and T76 conditions further allow the material to be matched to different service priorities. Correct selection, however, requires consideration of the complete joint system rather than strength alone.
Jiangsu Hetuo Aluminum Wire Co., Ltd. strengthens this product offering through a broad aluminum material portfolio, an approximately 40,000-square-meter manufacturing facility, professional technical personnel, intelligent production equipment, process-wide inspection, and ISO 9001 and IATF 16949 quality management certifications. These capabilities support consistent production and customized supply for customers requiring dependable aluminum alloy wire solutions.
For the best results, customers should communicate alloy, temper, diameter, forming process, service environment, packaging, inspection, and traceability requirements before ordering. With appropriate material selection and controlled manufacturing, aluminum alloy rivet wire can help create lighter and stronger structures while supporting long-term reliability and sustainable product design.
References
Aluminum Association. Aluminum Standards and Data. Industry reference for aluminum alloy designations, properties, and applications.
ASTM International. Standard Specifications for Aluminum and Aluminum Alloy Products. Reference framework for chemical composition, mechanical properties, testing, and conformity.
International Organization for Standardization. ISO 9001, Quality Management Systems—Requirements.
International Automotive Task Force. IATF 16949, Quality Management System Requirements for Automotive Production and Relevant Service Parts Organizations.
ASM International. ASM Handbook: Properties and Selection of Nonferrous Alloys and Special-Purpose Materials.
ASM International. Aluminum and Aluminum Alloys: Metallurgy, Heat Treatment, and Applications.
Military and aerospace material specifications applicable to high-strength aluminum alloys, heat-treated products, rivet wire, corrosion resistance, and fastener qualification.